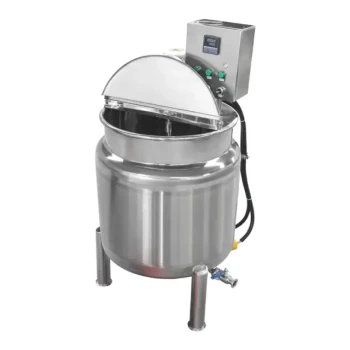
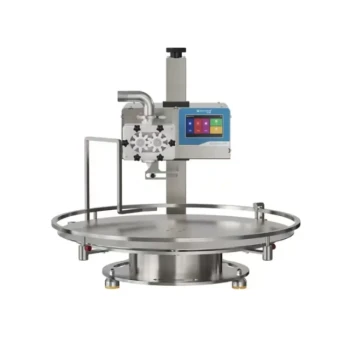
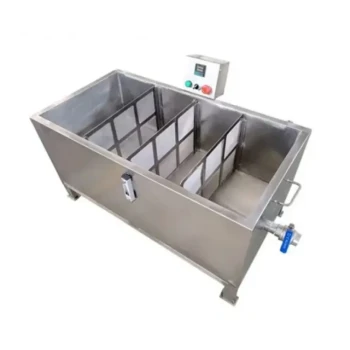
Industrial-grade honey creaming and mixing equipment is the essential foundation for functional honey products because it ensures structural stability and ingredient uniformity. By utilizing precise temperature regulation and controlled stirring speeds, these machines transform raw honey into a smooth, micro-crystalline matrix. This specialized environment is the only way to prevent functional additives—like superfood extracts or herbs—from separating, ensuring every jar delivers consistent potency and texture.
To succeed in the high-growth functional honey market, distributors must prioritize products processed with industrial-grade equipment. This technology guarantees a stable, homogenized product that preserves bioactive compounds while meeting the rigorous consistency standards required for international retail and wholesale.
Achieving Structural Perfection and Stability
The Science of Micro-Crystalline Creaming
Industrial equipment uses precise temperature regulation to force honey into an extremely fine crystalline structure. This process results in a smooth, spreadable texture that remains stable under various storage conditions. Without this level of control, honey often develops coarse, uneven crystals that diminish the premium consumer experience.
Prevention of Phase Separation
When incorporating functional ingredients like berry powders or plant extracts, maintaining a uniform mix is a significant challenge. Industrial mixers create a stable honey matrix that keeps additives perfectly suspended. This prevents the "layering" effect where ingredients float to the top or sink to the bottom, ensuring the product remains marketable throughout its shelf life.
Enhancing Product Efficacy and Market Value
Maximizing Bioavailability of Additives
The specialized stirring speeds of industrial machinery ensure that functional superfoods are integrated at a molecular level. This uniform distribution significantly enhances the bioavailability of bioactive components, such as antioxidants and vitamins. For distributors, this means providing a product that actually delivers on its health-related marketing claims.
Standardizing Sensory Characteristics
Wholesalers require product consistency across thousands of units to maintain brand reputation. Industrial-grade equipment allows for the homogenization of different honey batches, balancing flavors and chemical indicators. This ensures that every shipment meets strict market requirements for color, taste, and moisture content.
Ensuring Compliance and Export Readiness
Maintaining High Hygiene Standards
Industrial systems are designed to operate in strictly sterile environments, minimizing manual contact and external contamination. This automation is critical for meeting international food safety regulations and hygiene standards required for global export. High-precision filling machines further guarantee that each container meets exact weight specifications for retail.
Preservation of Natural Enzymes
While processing honey, it is vital to retain its natural antibacterial properties and heat-sensitive enzymes. Professional equipment uses controlled filtration and dehydration to remove impurities without overheating the product. This protects the medicinal value and phenolic compounds that define high-quality functional honey.
Understanding the Trade-offs
Technical Complexity vs. Output Quality
While industrial-grade equipment is necessary for quality, it requires deep professional expertise to calibrate and maintain. Improperly calibrated machinery can lead to over-processing, which may degrade the honey’s delicate enzyme profile. Partnering with a supplier that offers comprehensive technical oversight is essential to mitigate these risks.
Capital Investment and Scale
The primary challenge of industrial-grade production is the significant initial investment in hardware. For resellers, this highlights the importance of one-stop sourcing from established traders who have already scaled their operations. Accessing high-volume, automated production lines allows distributors to benefit from lower per-unit costs without sacrificing quality.
How to Apply This to Your Portfolio
To capitalize on the growing demand for functional honey, your sourcing strategy must focus on technical precision and supply chain reliability.
- If your primary focus is Premium Brand Positioning: Prioritize suppliers who utilize micro-crystalline creaming technology to ensure a luxurious texture and high bioactive retention.
- If your primary focus is Large-Scale Retail Distribution: Seek partners with high-precision automated filling and homogenization capabilities to guarantee product consistency across large volumes.
- If your primary focus is Rapid Market Entry: Leverage a trader with one-stop sourcing and ultra-fast delivery to bypass the complexities of manufacturing while ensuring export-grade quality.
Choosing products backed by industrial-grade technology is the only way to ensure the long-term stability and marketability of functional honey in a competitive global landscape.
Summary Table:
| Key Benefit | Industrial Equipment Feature | Value for Distributors & Wholesalers |
|---|---|---|
| Structural Stability | Precise Temperature Control | Prevents phase separation; ensures long shelf life. |
| Ingredient Uniformity | High-Speed Homogenization | Guarantees consistent additive potency in every jar. |
| Export Readiness | Sterile Automated Systems | Meets global hygiene and food safety regulations. |
| Market Appeal | Micro-Crystalline Processing | Creates a premium, smooth texture for high-end branding. |
Scale Your Functional Honey Business with HONESTBEE
Are you looking to dominate the high-growth functional honey market with superior product quality? HONESTBEE is your strategic partner for professional-grade beekeeping machinery and one-stop sourcing solutions.
We provide commercial apiaries, distributors, and B2B resellers with a comprehensive portfolio of high-performance hardware—from honey-filling machines and industrial mixers to essential industry consumables and hive-making equipment.
Why partner with HONESTBEE?
- Deep Industry Expertise: Specialized equipment designed to preserve bioactive honey compounds.
- Efficiency First: Ultra-fast delivery and rapid response times to keep your supply chain moving.
- Premium Trading Services: Exceptional customer support and OEM/ODM capabilities for global scale.
Take your wholesale operations to the next level with equipment that guarantees consistency and profit. Contact HONESTBEE Today to discuss your equipment needs and sourcing requirements!
References
- Małgorzata Dżugan, Monika Tomczyk. Gospodarcze i środowiskowe znaczenie pszczoły miodnej. DOI: 10.15584/pjsd.2024.28.1.7
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Economy Honey Homogenizer Mixer and Melting Machine for Beekeeping
- Double Wall Honey Heating Stirring Homogenizer Mixing Machine with Various Capacity
- Double Nozzle Small Honey Filling Machine Honey Sachet Packing Packaging Equipment
- Heavy Duty Stainless Steel Honey Processing Machine Decrystallizing Tank
- Small Honey Filling Machine Sachet Packing Equipment Single Nozzle
People Also Ask
- What impact do homogenizers or oscillating equipment have on honey microbial detection? Ensure Testing Accuracy
- Why is thorough mechanical stirring and homogenization emphasized in honey processing? Ensure Sample Accuracy
- How do heating equipment and homogenizers liquefy crystallized honey? Expert Guide to Professional Honey Processing
- What is the significance of honey homogenization? Elevate Commercial Honey Quality and Brand Consistency
- What is the role of homogenization equipment in the sensory evaluation of honey? Ensure Precision and Consistency