High-quality packaging is the critical barrier that preserves the high antioxidant levels and unique acidity of Trigona honey. It achieves this by blocking ultraviolet light and air exposure, which triggers oxidative degradation of the honey's active ingredients. Simultaneously, airtight, food-grade seals prevent the honey from absorbing atmospheric moisture, effectively stopping fermentation and maintaining its specific chemical profile.
Premium packaging materials transform a volatile natural product into a stable, high-value commodity by safeguarding its bioactive compounds and preventing spoilage. For B2B partners, this protection ensures product efficacy, regulatory compliance, and maximum shelf life throughout the global supply chain.
Preserving Bioactive Compounds and Chemical Stability
Neutralizing Oxidative Degradation
Trigona honey is prized for its high antioxidant content, which is highly sensitive to environmental factors. High-quality materials, such as darkened food-grade glass or specialized UV-resistant plastics, block the light and oxygen that cause these compounds to break down. This ensures that the honey retains its medicinal properties from the point of origin to the end consumer.
Maintaining Unique Acidity Levels
Unlike many other varieties, Trigona honey has a distinctively high acidity and low pH level. Inferior packaging materials can react with this acidity, leading to chemical leaching or a change in the honey’s flavor profile. Utilizing chemically inert materials ensures the honey's unique physicochemical indicators remain unchanged during long-term storage.
Preventing Fermentation Through Moisture Control
Honey is a hygroscopic substance, meaning it readily absorbs moisture from the surrounding air. If the moisture content rises, natural yeasts can trigger fermentation and spoilage, ruining the batch. High-quality airtight seals act as an absolute barrier against humidity, maintaining the physical stability of the product.
Strategic Advantages for Global Distribution
Ensuring Integrity During International Transport
For wholesalers and distributors, industrial-grade packaging is vital for surviving the rigors of long-distance international shipping. These materials provide the physical strength needed to prevent leakage while maintaining a stable internal environment despite fluctuating external temperatures. This reliability reduces the risk of order fulfillment issues and product loss.
Compliance and Food Safety Standards
Utilizing standardized, clean packaging materials is a fundamental requirement for meeting international food safety regulations. High-quality containers prevent secondary pollution and the intrusion of foreign odors during transit. This professional standard is essential for distributors looking to penetrate high-premium markets that demand strict hygiene certifications.
Enhancing Market Value and Brand Recognition
Beyond protection, premium packaging serves as a marketing tool that transforms bulk honey into a standardized retail product. Features like anti-counterfeit seals and unique bottle designs build consumer confidence and reinforce brand authority. This differentiation allows B2B resellers to command higher margins in competitive landscapes.
Understanding the Trade-offs
Balancing Protection and Shipping Costs
While heavy, high-density glass offers superior chemical protection and a premium feel, it significantly increases logistical costs and the risk of breakage. Distributors must often choose between the ultimate protection of glass and the efficiency and durability of specialized, high-grade plastics for bulk fulfillment.
Quality Control vs. Rapid Response
Implementing rigorous packaging standards can sometimes slow down the initial production phase. However, partnering with a supplier that offers one-stop sourcing and deep industry expertise ensures that high-quality standards are met without sacrificing rapid response times or order fulfillment speed.
Making the Right Choice for Your Goal
As a professional distributor or reseller, your choice of packaging should align with your specific market positioning and logistical requirements.
- If your primary focus is premium retail and medicinal branding: Prioritize high-density, UV-blocking glass bottles with anti-counterfeit seals to maximize chemical preservation and consumer trust.
- If your primary focus is high-volume international distribution: Opt for specialized, food-grade plastic containers that offer a high moisture barrier and durability while reducing shipping weight and breakage risks.
- If your primary focus is long-term inventory stability: Ensure all packaging features advanced induction-sealed liners to provide the highest level of protection against atmospheric moisture and oxidation.
Selecting the right packaging is not merely a logistical detail, but a strategic investment in the chemical integrity and marketability of Trigona honey.
Summary Table:
| Protection Factor | Technical Mechanism | Strategic B2B Benefit |
|---|---|---|
| UV & Light Control | Blocks light-induced oxidation | Preserves high antioxidant/medicinal levels |
| Airtight Sealing | Prevents moisture absorption | Stops fermentation; ensures long shelf life |
| Chemical Inertness | Neutralizes reaction with acidity | Maintains unique pH and flavor profiles |
| Structural Durability | High-density industrial grade | Reduces leakage and loss during global shipping |
| Regulatory Compliance | Food-grade standardized materials | Meets strict international safety certifications |
Streamline Your Supply Chain with HONESTBEE
Maximize your profit margins and ensure product integrity with HONESTBEE, the leading one-stop sourcing partner for commercial apiaries and B2B distributors. We provide a comprehensive full-spectrum portfolio, including honey-filling machines, hive-making hardware, and premium food-grade packaging consumables designed for the global market.
Why partner with HONESTBEE?
- Deep Industry Expertise: Professional-grade tools tailored for Trigona and premium honey varieties.
- Rapid Response & Fulfillment: Ultra-fast delivery to keep your distribution lines moving.
- Premium Trading Services: Dedicated support for wholesalers and resellers seeking reliable OEM/ODM solutions.
Contact us today to enhance your operational efficiency and secure your supply!
References
- S. Syamsurizal, Elsa Badriyya. Empowerment of UMKM Umah Labah An Nahl Farm and Education in improving Trigona honey bee cultivation. DOI: 10.24036/pelitaeksakta/vol8-iss2/269
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
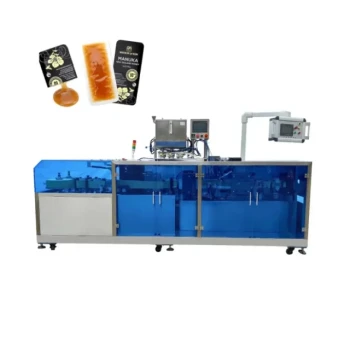
- Automatic Single-Dose Snap & Squeeze Honey Sachets Packing Machine
- Hexagonal Glass Honey Jars with Metal Lug Caps Elegant Versatile Packaging
- Inverted Squeezable Honey Jar with No Drip Flip Top Cap for Easy Pouring
- Classic Drum Shaped Glass Honey Jar with Airtight Lid
- Food Grade Plastic Honey Bucket Pail for Beekeeping
People Also Ask
- What are the advantages of honey sachet packing machines? Boost Efficiency & Unlock New Markets
- What are the main functions of a honey sachet packing machine? Boost Efficiency with Automated Precision
- How does an industrial-grade honey sachet packaging machine assist beekeepers in accessing public institution markets?
- Why is automated packaging machinery essential for scaling industrial honey production? Drive Commercial Scalability
- Why is it advantageous for apiaries to be located near honey processing centers? Boost Quality and Market Reach