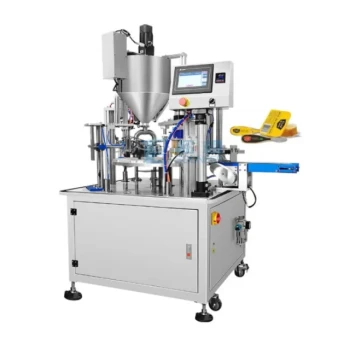
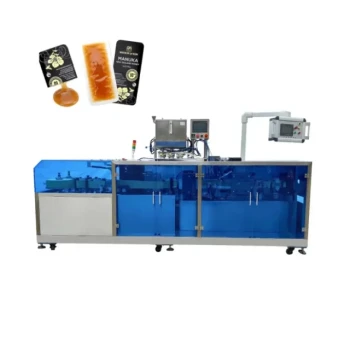
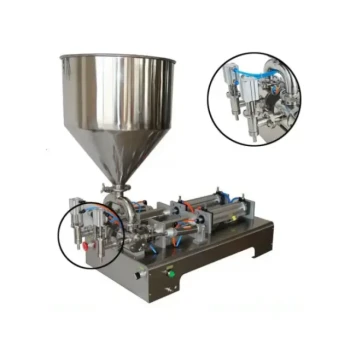
Automated honey-filling production lines serve as the ultimate safeguard for product purity and brand integrity.
These systems utilize standardized, closed-loop processes and precision sealing technologies to eliminate human contact and environmental exposure during the packaging phase. By integrating advanced anti-counterfeiting seal technologies, these lines create a robust technical barrier that prevents ingredient tampering and illegal product substitution. For B2B resellers, this translates to a guaranteed level of product integrity that manual operations simply cannot match.
For high-volume honey distributors, automation is a critical risk management strategy that replaces manual vulnerabilities with standardized precision. This technology secures the product against biological and physical contamination while providing the physical proof of authenticity required to maintain market trust and brand credit.
Eliminating Contamination through Environmental Control
The Security of Closed-Loop Systems
Automated lines function as fully enclosed operating systems, isolating the honey from the external environment. This setup prevents secondary contamination from airborne molds, yeasts, and dust that often occur during manual pouring or open-air handling. By maintaining a sterile path from the storage tank to the bottle, the system ensures the honey remains as pure as the day it was harvested.
Precision Filtration and Impurity Removal
Industrial-grade machinery often incorporates precision filtration systems directly into the production line. This eliminates physical impurities such as glass shards, metal fasteners, or industrial debris before the honey enters the container. For wholesalers, this level of automated monitoring reduces the liability risks associated with foreign objects in food products.
Preventing Fermentation and Moisture Absorption
Honey is hygroscopic and can quickly absorb moisture from the air, which leads to fermentation and spoilage. Automated systems utilize vacuum sealing and high-precision controls to maintain moisture content below the critical 20% threshold. This ensures long-term shelf stability and compliance with international packaging regulations, which is vital for long-distance shipping and storage.
Securing Product Authenticity and Preventing Fraud
Integrated Anti-Counterfeiting Seals
The primary defense against product tampering is the application of advanced anti-counterfeiting seals during the automated process. These machines apply tamper-evident packaging that is nearly impossible to replicate or reseal without detection. This creates a "physical foundation" for building brand credit and protecting the profit potential of premium honey products.
Precision Volumetric Control
Automated lines use precision metering to ensure that every unit contains the exact volume of product specified on the label. Consistent filling levels serve as a hallmark of professional quality and help distributors identify potential fraud in the supply chain. If filling levels are inconsistent, it often signals manual tampering or inferior processing methods.
Enhanced Labeling and Traceability
Modern filling lines often integrate automated labeling functions that can print batch codes and QR codes directly onto the packaging. This allows for rapid response times in the event of a recall and provides wholesalers with the data needed for efficient inventory management. High-standard encapsulation and professional aesthetics directly enhance the purchase appeal of the final product.
Understanding the Trade-offs of Automation
Capital Investment and Complexity
While automated lines significantly reduce risk, they require a substantial initial capital investment and ongoing maintenance by skilled technicians. Distributors must balance the high cost of machinery against the long-term gains in packaging efficiency and reduced waste.
Flexibility and Changeover Time
High-speed automated systems are often optimized for specific bottle shapes and sizes, which can limit production flexibility. Switching between different product types or container styles may involve downtime for recalibration. However, for B2B operations focused on ultra-fast delivery, the speed of standardized production usually outweighs the need for high variability.
Optimizing Your Supply Chain for Quality Assurance
As a distributor or wholesaler, your choice of sourcing partner should be guided by their commitment to technical excellence and professional industry expertise. Automated production is the benchmark for reliability in the modern honey market.
- If your primary focus is Market Trust and Brand Protection: Prioritize suppliers who utilize fully enclosed, automated lines with integrated tamper-evident sealing technology to ensure 100% product authenticity.
- If your primary focus is Supply Chain Efficiency and Scale: Seek partners with high-speed industrial filling capabilities that support rapid response times and consistent order fulfillment during peak demand.
- If your primary focus is Regulatory Compliance and Safety: Ensure your sourcing partner utilizes precision filtration and moisture-control systems to meet rigorous food safety standards and extend product shelf life.
Investing in products backed by automated precision is the most effective way to guarantee the safety, purity, and marketability of your honey inventory.
Summary Table:
| Feature | Protection Mechanism | Business Value for B2B |
|---|---|---|
| Contamination Control | Closed-loop systems & precision filtration | Ensures product purity and reduces liability risks. |
| Authenticity Security | Tamper-evident seals & integrated labeling | Protects brand credit and prevents illegal substitution. |
| Quality Consistency | Precision volumetric metering & vacuum sealing | Guarantees shelf stability and standardized professional quality. |
| Traceability | Automated batch and QR code printing | Enables rapid response and efficient inventory management. |
Secure Your Supply Chain with HONESTBEE Precision
Protect your brand integrity and maximize profit margins with HONESTBEE. We provide commercial apiaries and distributors with a one-stop sourcing solution for high-performance honey-filling machines and the full spectrum of beekeeping equipment.
From industrial-grade machinery to essential consumables, our portfolio is designed for rapid response and ultra-fast delivery. Partner with us to leverage deep industry expertise and premium trading services that ensure your products meet the highest safety standards.
Ready to upgrade your production? Contact our experts at HONESTBEE today!
References
- E. R. Mendybayeva, A.R. Khairushev. CONSUMER PREFERENCES IN PURCHASING NATURAL HONEY: EVIDENCE FROM A SURVEY IN WEST KAZAKHSTAN REGION. DOI: 10.52578/2305-9397-2025-4-1-167-176
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Automatic Honey Filling and Filtering Machine for Beekeeping Bottle Filling
- Precision Automated Packaging Turntable Honey Spoon Filling Sealing Packing Machine
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
- Commercial Rotary Honey Filling Machine for Production
People Also Ask
- Why are fully automatic honey filling and packaging lines essential? Boost Your Honey's Market Value and Quality
- What is a fully-automatic honey filler? Streamline Your Production with High-Precision Automation
- How do automated honey filling and packaging machines affect profitability? Boost Margins with HONESTBEE Technology
- How do automated honey filling and packaging machines contribute to the market value of honey products? Maximize Your ROI
- How do industrial-grade automated honey filling and packaging machines mitigate the risk of physical contamination?