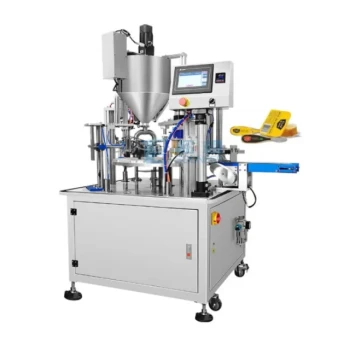
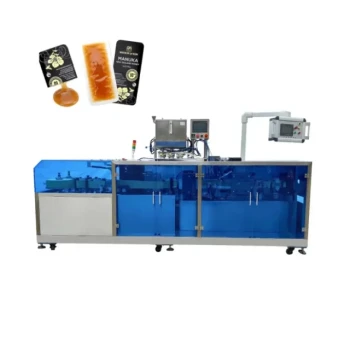
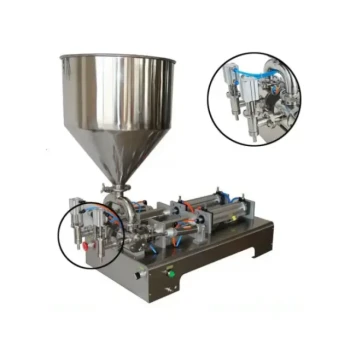
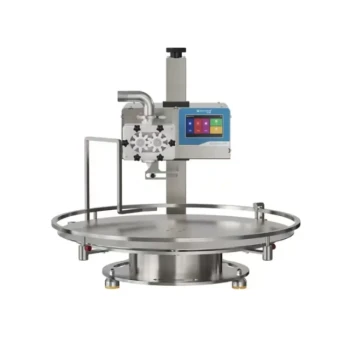
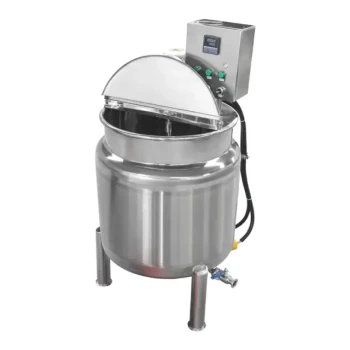
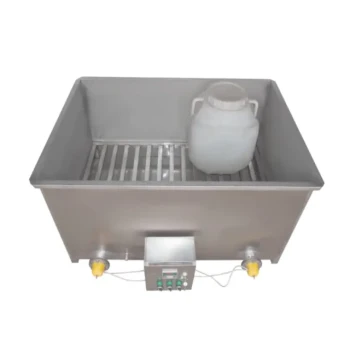
Industrial-grade honey filling and packaging machines transform raw organic honey into a high-value, export-ready commodity by ensuring biological integrity and operational precision. These machines utilize temperature-controlled environments and airtight, closed-loop systems to protect sensitive bioactive compounds like enzymes and antioxidants. By providing high-precision volumetric filling and standardized sealing, they ensure every unit meets the rigorous hygiene and weight requirements of global high-end markets.
The core value of industrial honey equipment lies in its ability to bridge the gap between raw harvest and premium retail through contamination-free automation. This infrastructure is essential for distributors seeking consistent, scalable, and internationally certified products that maintain their "organic" premium.
Preserving the Biological Essence of Organic Honey
Temperature Control and Bioactive Integrity
Industrial equipment ensures the dispensing process occurs under strictly controlled temperatures. This is vital for maximizing the preservation of bioactive components such as antioxidants, enzymes, and polyphenols that define high-quality organic honey.
Oxygen Isolation and Flavor Retention
Closed-system designs isolate the honey from excess oxygen and external contaminants. This prevents oxidation, helping to maintain the natural flavor profiles and vitamins that sophisticated B2B buyers and consumers demand.
Preventing Physicochemical Spoilage
Honey is naturally hygroscopic, meaning it easily absorbs moisture from the air, which can lead to fermentation. Standardized, airtight sealing technologies effectively prevent spoilage, ensuring physicochemical stability throughout the supply chain.
Achieving Operational Excellence and Scalability
High-Precision Volumetric Metering
Modern machines utilize automated metering to achieve exact quantitative packaging. This level of precision minimizes product waste and ensures the net weight accuracy of every retail unit, protecting the distributor's margins.
Rapid Order Fulfillment and Throughput
For wholesalers, speed is a competitive advantage. Industrial automation significantly increases filling efficiency, allowing for the rapid processing of large-scale orders and ensuring ultra-fast delivery to global markets.
Eliminating Secondary Contamination
By implementing a closed-loop operation, these machines minimize contact between the honey and the external environment or human operators. This reduces the risk of cross-contamination, maintaining the hygienic quality required for high-end supplement and cosmeceutical applications.
Securing Market Access and Brand Credibility
Meeting International Export Standards
Standardized packaging is a prerequisite for entering modern retail channels and achieving international export certification. These machines provide the consistency needed to satisfy the most rigorous global hygiene requirements.
Traceability and Professional Branding
Automated labeling systems integrated into the packaging line assist in establishing brand identity and traceability. This allows consumers to distinguish authentic organic honey from unbranded alternatives, increasing market credibility.
Professional Finishing for Premium Markets
High-quality seals and consistent container presentation signal professionalism and reliability. For B2B resellers, this translates into a product that is "shelf-ready" for premium boutiques and health-conscious retailers.
Understanding the Trade-offs
The Cost of Precision
While industrial-grade machines offer unmatched quality, they require a higher initial capital investment compared to manual or semi-automated processes. This cost is typically offset by the reduction in labor and the elimination of product waste over time.
Maintenance and Technical Expertise
These sophisticated systems require regular maintenance and a degree of technical expertise to operate. Distributors should partner with suppliers who offer deep professional industry expertise and dedicated customer support to minimize downtime.
Flexibility vs. Speed
High-speed machines are often optimized for specific container shapes. Transitioning between different packaging formats (e.g., glass jars to plastic sachets) may require changeover time, which must be factored into production schedules.
How to Apply This to Your Sourcing Strategy
Making the Right Choice for Your Goal
To maximize the value of your organic honey portfolio, your equipment and sourcing choices should align with your specific business objectives.
- If your primary focus is global export and certification: Prioritize machines with airtight, closed-loop systems that meet international hygiene and traceability standards.
- If your primary focus is maximizing profit margins: Invest in high-precision volumetric filling to eliminate product "overfill" and minimize raw material waste.
- If your primary focus is premium health and beauty markets: Ensure your processing equipment emphasizes strict temperature control to guarantee the potency of bioactive enzymes and polyphenols.
By integrating advanced filling and packaging technology, you ensure that the intrinsic value of organic honey is not just preserved, but amplified for the global marketplace.
Summary Table:
| Key Feature | Benefit to Organic Honey | Strategic Value for B2B |
|---|---|---|
| Temperature Control | Preserves bioactive enzymes & antioxidants | Ensures premium quality & certification |
| Closed-Loop System | Prevents oxidation & secondary contamination | Guarantees hygiene for health markets |
| Volumetric Metering | High-precision quantitative packaging | Minimizes waste & protects profit margins |
| Automated Labeling | Professional finish & full traceability | Enhances brand credibility & export-readiness |
Ready to Scale Your Organic Honey Exports?
Partner with HONESTBEE, your one-stop sourcing partner for commercial beekeeping excellence. We empower distributors and wholesalers with a comprehensive full-spectrum product portfolio, ranging from high-precision honey-filling and hive-making machinery to essential industry consumables and honey-themed cultural merchandise.
Why Choose HONESTBEE?
- One-Stop Sourcing: Access everything from specialized hardware to retail-ready supplies in one place, streamlining your procurement.
- Operational Excellence: Benefit from ultra-fast delivery and efficient order fulfillment to keep your supply chain moving at market speed.
- Deep Industry Expertise: Leverage our professional knowledge to select equipment that maximizes your profit margins and ensures international certification compliance.
- Dedicated Support: Experience exceptional customer service with rapid response times tailored specifically to the needs of B2B resellers.
Contact HONESTBEE Today to optimize your production line and secure your position in the premium global honey market!
References
- Ye. V. Klimov, O. B. Krupskiy. Global market for organic honey: trends, barriers and potential for the Republic of Kazakhstan. DOI: 10.46666/10.46666/2025-4.2708-9991.10
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Economy Small Honey Filling Machine Honey Bottle Filler Packaging Machine
- Precision Automated Packaging Turntable Honey Spoon Filling Sealing Packing Machine
- Double Nozzle Small Honey Filling Machine Honey Sachet Packing Packaging Equipment
- Small Honey Filling Machine Sachet Packing Equipment Single Nozzle
People Also Ask
- Why are fully automatic honey filling and packaging lines essential? Boost Your Honey's Market Value and Quality
- What is a fully-automatic honey filler? Streamline Your Production with High-Precision Automation
- How do automated honey filling and packaging machines affect profitability? Boost Margins with HONESTBEE Technology
- How do automated honey filling and packaging machines contribute to the market value of honey products? Maximize Your ROI
- How do industrial-grade automated honey filling and packaging machines mitigate the risk of physical contamination?