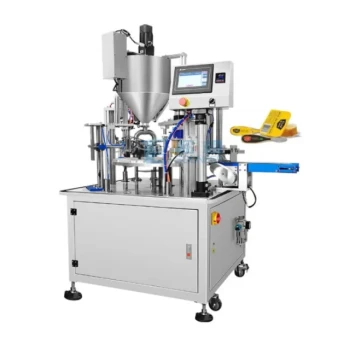
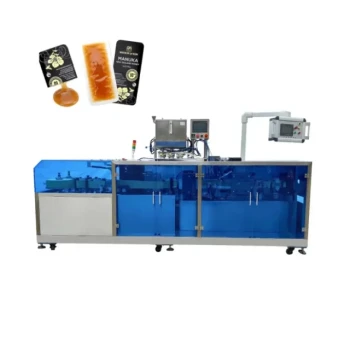
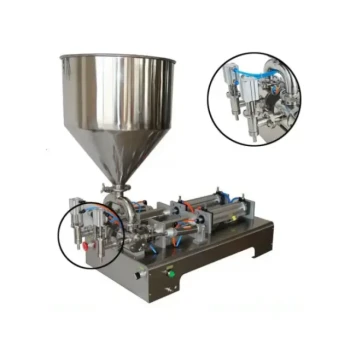
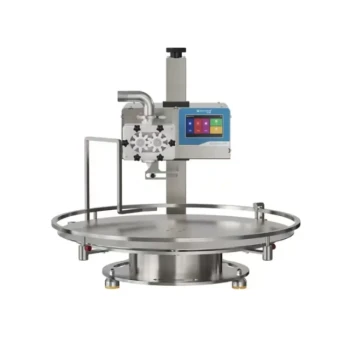
Automated honey filling and packaging equipment secures product quality by integrating precision metering with advanced hermetic sealing and temperature regulation. These systems prevent moisture absorption and fermentation while preserving natural enzymes and aromatic compounds through controlled, low-temperature processing. By eliminating manual handling, these machines ensure every unit meets international food safety standards and maintains shelf-life stability for several years.
Automated equipment creates a sterile, controlled environment that safeguards honey from its primary threats—moisture and contamination—ensuring that the final product retains its natural integrity and commercial value throughout the global supply chain.
Preserving Natural Integrity Through Temperature Control
Protecting Heat-Sensitive Enzymes
Honey is a bio-active product containing delicate enzymes like amylase and catalase that are easily destroyed by excessive heat. Automated systems utilize integrated temperature control units to facilitate filling at the lowest possible temperature required for flow. This precision ensures that the honey’s nutritional profile and medicinal properties remain intact from the apiary to the consumer.
Maintaining Aromatic Compounds and Flavor
High-precision equipment minimizes the time honey is exposed to the environment during processing. Rapid, low-temperature filling prevents the volatilization of delicate aromatic compounds. This keeps the flavor profile consistent, a critical factor for distributors managing premium brands that rely on specific floral notes.
Eliminating Contamination and Fermentation Risks
The Role of Hermetic Sealing
Moisture is the primary catalyst for honey fermentation and spoilage. Automated packaging lines provide a hermetically sealed environment, creating an airtight barrier that prevents the honey from absorbing moisture from the atmosphere. This seal is the foundation of long-term shelf-life stability, often extending the product's viability for years.
Prevention of Secondary Contamination
Manual handling is a significant source of microbial introduction in food packaging. Automated, closed-system filling isolates the product from human contact and airborne pollutants. By meeting strict food safety and compliance standards, these systems reduce the risk of costly product recalls for wholesalers and resellers.
Engineering Consistency for the Global Market
High-Precision Volume Metering
Consistency is a prerequisite for modern commercial distribution. Automated machines use precision metering pumps to ensure that every bottle contains the exact net weight required by international trade regulations. This eliminates material waste and ensures that distributors receive standardized units ready for immediate retail placement.
Managing High Viscosity and Crystallization
Honey’s physical properties vary significantly, from fluid blossom honey to thick, viscous chestnut varieties. Professional equipment is engineered to handle these specific viscosity profiles without dripping or clogging. This mechanical reliability ensures high production efficiency and uniform product appearance across entire batches.
Understanding the Trade-offs and Technical Challenges
Balancing Speed with Product Stability
While high-speed filling increases throughput, excessive mechanical agitation can introduce air bubbles that lead to unsightly foaming or premature crystallization. Finding the "sweet spot" in machine calibration is essential to maintain visual appeal and purchase appeal.
Maintenance and Sanitation Requirements
The complexity of automated metering systems requires a disciplined maintenance schedule. Residue buildup in a closed system can compromise hygiene if not managed with professional cleaning-in-place (CIP) protocols. For B2B partners, sourcing equipment from providers with deep technical expertise is vital to avoid these operational pitfalls.
Making the Right Choice for Your Goal
As a distributor or wholesaler, selecting the right equipment or sourcing partner depends on your specific market requirements and volume goals.
- If your primary focus is Premium Quality preservation: Prioritize systems with advanced low-temperature control and vacuum-sealed filling to protect natural enzyme activity.
- If your primary focus is High-Volume Distribution: Invest in high-precision quantitative technology that emphasizes rapid response times and ultra-fast delivery through efficient order fulfillment.
- If your primary focus is International Compliance: Ensure the machinery utilizes closed-system packaging to meet the strictest global food safety and hygiene standards.
By leveraging automated precision and professional industry expertise, businesses can ensure their honey products remain stable, safe, and highly marketable across the entire distribution network.
Summary Table:
| Key Feature | Functional Benefit | Impact on Product Quality & Stability |
|---|---|---|
| Temperature Control | Protects heat-sensitive enzymes | Preserves nutritional profile and natural floral aromas. |
| Hermetic Sealing | Airtight moisture barrier | Prevents fermentation and ensures multi-year shelf-life. |
| Precision Metering | Uniform weight/volume filling | Guarantees international trade compliance and zero waste. |
| Closed-System Design | Eliminates manual contact | Prevents secondary contamination and microbial growth. |
Scale Your Honey Distribution with HONESTBEE
Are you looking to optimize your production line or expand your wholesale inventory? HONESTBEE is your premier partner for one-stop beekeeping and processing solutions. We cater specifically to commercial apiaries, distributors, and B2B resellers, offering a comprehensive full-spectrum product portfolio—from high-precision honey-filling and hive-making machines to essential industry consumables.
Why partner with us?
- Deep Industry Expertise: Advanced machinery designed to meet global food safety standards.
- Premium Trading Services: Dedicated support for OEM/ODM requirements and maximizing your profit margins.
- Rapid Fulfillment: Ultra-fast delivery and efficient order processing to keep your supply chain resilient.
Ready to elevate your product quality? Contact HONESTBEE Today to discuss our wholesale offerings and technical solutions.
References
- Małgorzata Dżugan, Monika Tomczyk. Gospodarcze i środowiskowe znaczenie pszczoły miodnej. DOI: 10.15584/pjsd.2024.28.1.7
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Precision Automated Packaging Turntable Honey Spoon Filling Sealing Packing Machine
- Automatic Single-Dose Snap & Squeeze Honey Sachets Packing Machine
- Double Nozzle Small Honey Filling Machine Honey Sachet Packing Packaging Equipment
- Automatic Honey Filling and Filtering Machine for Beekeeping Bottle Filling
People Also Ask
- Why are fully automatic honey filling and packaging lines essential? Boost Your Honey's Market Value and Quality
- What is a fully-automatic honey filler? Streamline Your Production with High-Precision Automation
- How do automated honey filling and packaging machines affect profitability? Boost Margins with HONESTBEE Technology
- How do automated honey filling and packaging machines contribute to the market value of honey products? Maximize Your ROI
- How do industrial-grade automated honey filling and packaging machines mitigate the risk of physical contamination?