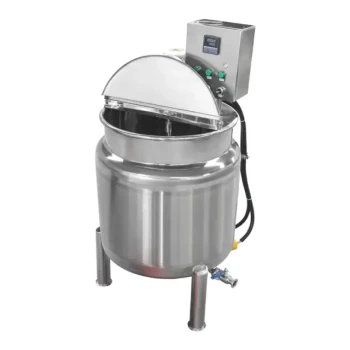
Automated filling and labeling systems are the essential technical drivers for premium organic honey positioning. These systems ensure pharmaceutical-grade hygiene, absolute product consistency, and the precise application of organic certifications required to command high-end retail prices. For distributors and wholesalers, this technology transforms raw bulk honey into a standardized, high-value commodity ready for immediate international export and elite shelf placement.
Automated systems bridge the gap between artisanal production and global scalability by integrating hygiene, precision, and traceability. This infrastructure is necessary to justify "organic" price premiums and satisfy the rigorous quality demands of modern B2B supply chains.
Scaling Professionalism Through Technical Precision
Maintaining Aseptic Integrity and Flavor
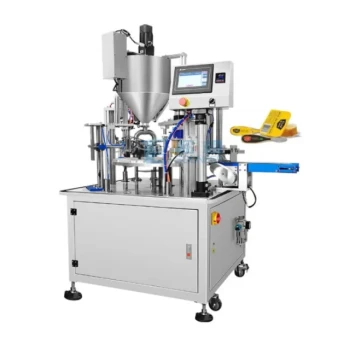
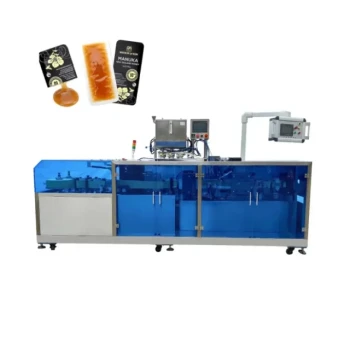
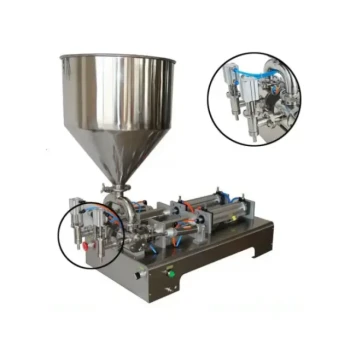
Industrial-grade automated filling machines facilitate the commercialization of organic honey by providing high-precision quantitative filling in a sealed, aseptic environment. This mechanical process prevents secondary contamination and protects the honey from flavor loss caused by oxidation, ensuring the sensory profile remains intact from production to the end-consumer.
Standardization for Rapid Order Fulfillment
High-precision filling equipment maintains consistent product specifications across every unit, which is critical for wholesalers managing large-scale inventories. This consistency allows for ultra-fast delivery and efficient order fulfillment, as every jar meets the exact physical and chemical standards required for high-end international retail markets.
Transitioning Bulk Production to Retail-Ready Goods
Automated systems transform bulk honey into retail-ready products by ensuring consistent weight and volume through precise measurement. By facilitating this transition from bulk sales to branded bottling, distributors can meet food safety registration requirements and significantly increase the product's price premium potential.
Elevating Brand Perception in the Organic Sector
The Power of High-Precision Labeling
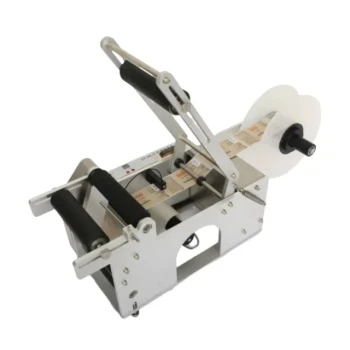
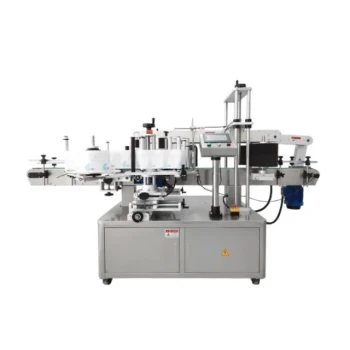
High-precision labeling functions allow for the clear presentation of organic certification marks and traceability QR codes. These elements are essential for communicating product differentiation and enhancing brand transparency, which are the primary drivers of consumer trust in a competitive organic market.
Visual Cues for Authenticity and Quality
In the organic honey market, consumers rely heavily on visual packaging to perceive product authenticity and quality. Automated systems ensure that labels are perfectly aligned and tamper-evident seals are secure, directly addressing consumer concerns regarding safety, health benefits, and premium positioning.
Supporting Full-Spectrum Product Portfolios
Advanced automated lines allow for diverse packaging materials and ergonomic designs, enabling distributors to offer a comprehensive product portfolio. This flexibility allows businesses to pivot quickly to market trends, providing a one-stop sourcing capability for diverse retail needs.
Understanding the Trade-offs and Challenges
Significant Initial Capital Investment
The primary barrier to implementing automated filling and labeling is the high initial expenditure required for industrial-grade machinery. While these systems lower long-term labor costs and increase efficiency, the upfront cost can be a significant hurdle for smaller producers or emerging distributors.
Requirements for Specialized Technical Expertise
Operating and maintaining high-precision automated systems requires a level of professional industry expertise that manual bottling does not. Without a dedicated technical team or a reliable service partner, mechanical downtime can disrupt the supply chain and impact rapid response times.
Loss of the "Handmade" Aesthetic
In some niche markets, perfectly uniform, machine-labeled jars may lack the artisanal "handmade" feel that some organic consumers crave. Distributors must balance the benefits of industrial efficiency with a packaging design that still communicates the natural, rustic origins of organic honey.
Strategic Recommendations for B2B Growth
Selecting the right packaging infrastructure is a critical business decision that impacts your entire supply chain. As a distributor or reseller, your choice should align with your specific market entry and scaling goals.
- If your primary focus is rapid market expansion and export: Invest in high-speed, aseptic automated lines to ensure your product meets the strict food safety and standardization requirements of international retail giants.
- If your primary focus is premium brand building and trust: Prioritize systems with high-precision labeling and traceability integration to clearly showcase organic certifications and origin stories, which are the main drivers of consumer purchase intent.
- If your primary focus is operational efficiency and fulfillment: Utilize automated systems that offer quick-changeover capabilities to maintain a diverse product portfolio and guarantee ultra-fast delivery for your B2B clients.
By integrating automated precision into your organic honey supply chain, you secure a competitive advantage rooted in quality, transparency, and professional reliability.
Summary Table:
| Feature | Benefit for Organic Positioning | Impact on B2B Operations |
|---|---|---|
| Aseptic Filling | Protects flavor and prevents contamination | Ensures pharmaceutical-grade quality for export |
| Precision Labeling | Displays organic certifications and QR codes | Builds brand transparency and consumer trust |
| Standardization | Guarantees consistent weight and appearance | Enables ultra-fast fulfillment and retail readiness |
| Packaging Flexibility | Supports diverse materials and ergonomic designs | Facilitates a full-spectrum product portfolio |
Elevate Your Honey Production with HONESTBEE
At HONESTBEE, we empower commercial apiaries and B2B distributors with the professional machinery needed to dominate the organic market. Our one-stop sourcing capability covers the full spectrum of beekeeping tools, from hive-making hardware to high-precision honey-filling and labeling machines.
Why Partner with HONESTBEE?
- Comprehensive Portfolio: Access a full array of machinery and industry consumables tailored for scale.
- Deep Industry Expertise: Benefit from our professional knowledge to optimize your production efficiency.
- Rapid Fulfillment: We prioritize ultra-fast delivery to ensure your supply chain remains uninterrupted.
- Premium B2B Service: Dedicated support designed to help wholesalers maximize profit margins and brand reliability.
Ready to transform your bulk honey into a high-value retail asset? Contact our expert team today to explore our wholesale solutions!
References
- Fatih Bilici, Nebi Seren. A Study on Consumers' Knowledge of Distinguishing Natural and Organic Honey. DOI: 10.24925/turjaf.v13i3.545-552.7182
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Automatic Honey Filling and Filtering Machine for Beekeeping Bottle Filling
- Precision Automated Packaging Turntable Honey Spoon Filling Sealing Packing Machine
- Semi Automatic Small Honey Bottle Filling Machine Honey Filler
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
People Also Ask
- Why are fully automatic honey filling and packaging lines essential? Boost Your Honey's Market Value and Quality
- What is a fully-automatic honey filler? Streamline Your Production with High-Precision Automation
- How do automated honey filling and packaging machines affect profitability? Boost Margins with HONESTBEE Technology
- How do automated honey filling and packaging machines contribute to the market value of honey products? Maximize Your ROI
- How do industrial-grade automated honey filling and packaging machines mitigate the risk of physical contamination?