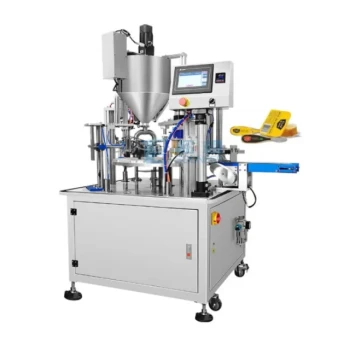
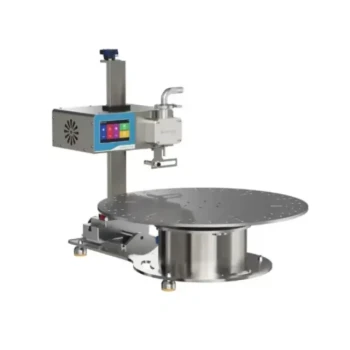
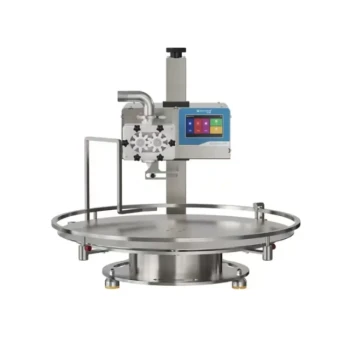
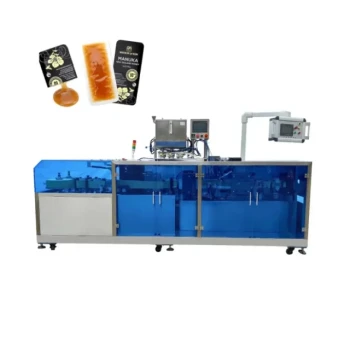
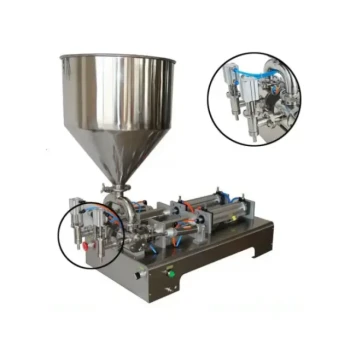
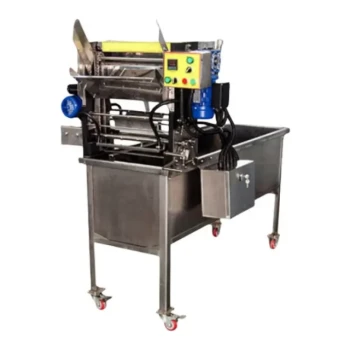
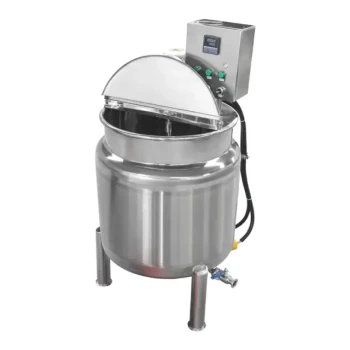
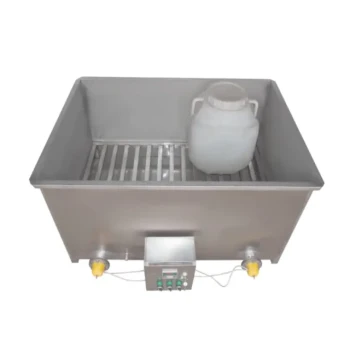
High-automation honey filling and sealing machines are the critical link between raw forest extraction and global commercial distribution. These systems provide the industrial scale, hygienic precision, and standardized packaging necessary to transform premium forest honey into a market-ready commodity. By automating the final processing stage, producers can guarantee food safety and volume consistency, ensuring the product meets the rigorous demands of international retail markets.
For distributors and wholesalers, these machines represent more than just speed; they are the foundation of supply chain reliability and product integrity. High-automation systems ensure that high-value forest honeys maintain their unique properties while meeting the volume requirements of large-scale B2B contracts.
Preserving the Quality of Premium Forest Honey
Protecting Delicate Natural Properties
Forest honeys, such as acacia and linden, are prized for their low crystallization tendencies and unique aroma profiles. High-automation machines utilize closed-loop systems that minimize exposure to air, preventing moisture absorption and the loss of volatile aromatic compounds.
Mitigating Secondary Contamination
In a commercial environment, manual handling is a primary source of contamination. Automated lines operate in sterile, controlled environments, using specialized sealing processes that protect the honey from impurities and ensure a longer, more stable shelf life for global export.
Maintaining Nutritional Integrity
Premium forest honey contains high-value nutritional components that are sensitive to environmental fluctuations. Industrial-grade filling equipment ensures that the honey is processed at optimal temperatures and speeds, preserving its natural enzyme content and health benefits.
Driving Efficiency in Large-Scale Supply Chains
Precision Quantitative Packaging
Wholesalers require exact consistency across thousands of units to maintain profit margins and regulatory compliance. High-precision metering pumps ensure that every jar contains the exact volume specified, minimizing material waste and ensuring standardized packaging for retail shelves.
Scaling for Industrial Capacity
When forest sources yield thousands of tons of honey, manual processes become a bottleneck. Automated lines provide the industrial capacity necessary for rapid order fulfillment, allowing distributors to respond to large-scale market demands without compromising on delivery timelines.
Enhancing Market Competitiveness
A professional, uniform appearance is non-negotiable for modern branding. Automation ensures that every seal is perfect and every label is aligned, meeting the aesthetic standards of high-end international markets and building consumer trust in the brand.
Understanding the Trade-offs
High Initial Investment vs. Unit Cost
The primary drawback of high-automation systems is the significant capital expenditure required for procurement and setup. However, for large-scale operations, this is balanced by a drastically lower cost-per-unit and the elimination of losses caused by manual handling errors.
Technical Complexity and Maintenance
These machines require specialized technical expertise to operate and maintain. While they reduce manual labor, they increase the need for skilled technicians to manage the precise metering controls and ensure the machinery remains compliant with food safety certifications.
Flexibility vs. Speed
Highly automated lines are often optimized for specific container shapes and sizes to maximize speed. This can lead to a lack of flexibility if a distributor needs to switch frequently between diverse packaging formats, requiring additional downtime for equipment recalibration.
Strategic Advantages for Your Business Goal
Making the Right Choice for Your Goal
To succeed in the competitive honey market, your equipment strategy must align with your specific commercial objectives and supply chain requirements.
- If your primary focus is Rapid Market Entry and Fulfillment: Prioritize high-speed automated lines that offer ultra-fast delivery and efficient order fulfillment to capture immediate market share.
- If your primary focus is Brand Premiumization: Invest in machines with advanced vacuum sealing and precise metering to ensure the highest possible aesthetic and hygienic standards for luxury forest honey.
- If your primary focus is Operational Scalability: Look for modular automated systems that can handle thousands of tons, providing the industrial capacity needed for high-volume wholesale contracts.
- If your primary focus is Risk Mitigation: Select closed-loop, high-automation systems that guarantee food safety and consistency, reducing the likelihood of product recalls or regulatory hurdles.
By integrating high-automation technology into the production process, you ensure that every jar of forest honey delivered to your clients is a testament to professional excellence and uncompromising quality.
Summary Table:
| Key Feature | Advantage for B2B Operations | Strategic Business Impact |
|---|---|---|
| Closed-Loop System | Eliminates secondary contamination | Ensures export-grade food safety standards |
| Precision Metering | Minimizes product giveaway/waste | Protects profit margins and compliance |
| Industrial Speed | Enables rapid order fulfillment | High capacity for large-scale contracts |
| Vacuum Sealing | Preserves volatile aromatic compounds | Maintains premium quality and shelf life |
Partner with HONESTBEE to Revolutionize Your Honey Supply Chain!
As a leading one-stop sourcing partner, HONESTBEE empowers distributors and commercial apiaries with a comprehensive portfolio of beekeeping machinery and consumables. We specialize in providing the full spectrum of equipment—from high-precision honey-filling lines to specialized hive-making machines—tailored to the needs of B2B resellers.
Why choose HONESTBEE?
- Deep Industry Expertise: Professional guidance to optimize your production efficiency.
- Full-Spectrum Portfolio: One-stop access to hardware, machinery, and cultural merchandise.
- Rapid Fulfillment: Ultra-fast delivery and dedicated service to ensure your supply chain remains reliable.
- B2B Focus: Supporting your growth with competitive wholesale offerings and OEM/ODM capabilities.
Connect with our wholesale experts today to scale your business!
References
- Serhii Razanov, Halyna Hytsol. EVALUATION OF THE FOREST NECTAR-POLLINIFEROUS TREES AND EFFICIENCY OF THEIR USAGE IN THE NECTAR-BEARING LINE OF BEES IN THE CONDITIONS OF VINNYTSІA REGION. DOI: 10.37128/2707-5826-2019-1-17
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Precision Automated Packaging Turntable Honey Spoon Filling Sealing Packing Machine
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Automatic Honey Filling and Filtering Machine for Beekeeping Bottle Filling
- Commercial Rotary Honey Filling Machine for Production
People Also Ask
- Why is the use of professional filling and sealing packaging machinery necessary for the production of high-value honey?
- What role do automated filling and packaging machines play in the honey supply chain? Scale Your Retail Distribution
- What are the benefits of automated honey filling and packaging? Scale Your Apiary with Industrial Precision
- What role do professional automated filling and packaging machines play in honey processing? Boost Efficiency & Value
- How do automated honey filling and packaging machines contribute to the market value of honey products? Maximize Your ROI