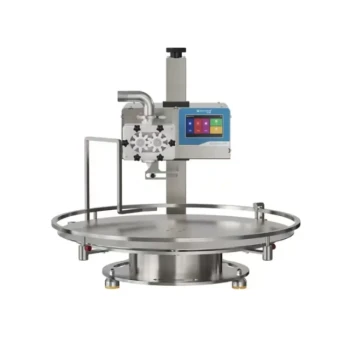
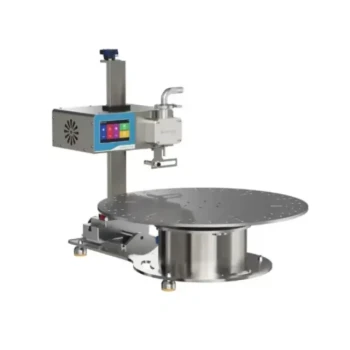
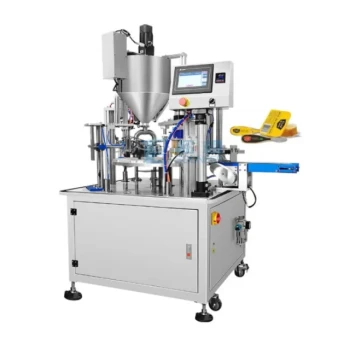
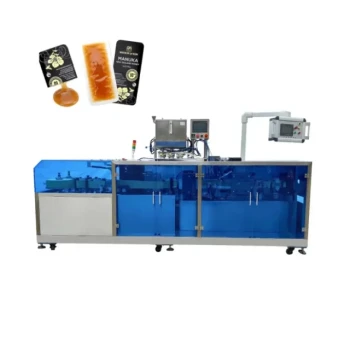
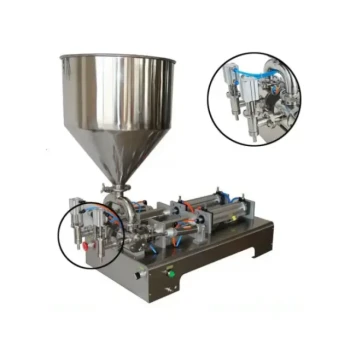
Industrial honey-filling machines serve as the critical infrastructure that transforms raw apiary output into standardized, market-ready commodities. By utilizing high-precision weight control and automated workflows, these machines bridge the gap between variable biological production and the strict uniformity required for global commercial distribution.
The primary role of these machines is to convert the raw productivity of forager bees into high-value economic assets through standardization and hygiene. This process ensures that bulk honey is rapidly packaged into consistent units, minimizing product loss and meeting the rigorous quality standards of international B2B markets.
Transforming Raw Output into Standardized Assets
Precision Quantitative Filling
Industrial machines use precision metering pumps and weight control technology to ensure every container meets exact net weight specifications. This level of accuracy is a prerequisite for branding and entry into high-end markets where consistency is non-negotiable.
Handling High-Viscosity Products
These systems are engineered to manage the unique physical properties of honey, royal jelly, and propolis. By handling dehydrated and filtered products with high viscosity, the machinery maintains the integrity of the substance while ensuring high-speed packaging.
Uniformity for Global Distribution
Automation enables the creation of standardized, shelf-ready products that comply with international export requirements. For distributors, this means receiving a product portfolio that is ready for immediate wholesale or retail placement without further processing.
Maximizing Operational Throughput and Efficiency
Rapid Response and Order Fulfillment
High-speed automation allows apiaries and processing facilities to handle peak volumes during harvest cycles. This capacity is essential for wholesalers who require ultra-fast delivery and efficient order fulfillment to maintain supply chain stability.
Minimizing Product Loss
By automating the dispensing process, these machines significantly reduce the waste associated with manual pouring and spillages. This efficiency ensures that the biological productivity of the bee colony is fully captured and converted into sellable inventory.
Scaling Commercial Operations
Industrial-grade equipment reduces the reliance on manual labor, allowing for large-scale operations that can meet the demands of massive distribution networks. This scalability is what allows a local apiary to function as a global commercial supplier.
Ensuring Hygiene and Market Compliance
Preventing Secondary Contamination
The use of sterile, automated systems minimizes human contact with the product, effectively preventing secondary contamination. This is critical for maintaining export-grade quality and ensuring the honey meets strict health and safety regulations.
Extending Product Shelf Life
Consistent, airtight sealing systems provided by these machines ensure that the honey remains stable during transit and storage. For resellers, this translates to a reliable product life and reduced risk of spoilage or fermentation.
Enhancing Professional Credibility
Utilizing sophisticated filling technology signals a high level of industry expertise and commitment to quality. This builds trust with distributors who seek partners capable of providing a comprehensive, full-spectrum product portfolio.
Understanding the Trade-offs
Equipment Specialization vs. Versatility
While high-precision machines offer unmatched efficiency for honey, they often require significant reconfiguration or specialized parts to handle different container shapes or viscosities. This lack of instant flexibility means that a "one-size-fits-all" approach can lead to bottlenecks if a distributor suddenly shifts packaging requirements.
Maintenance and Downtime Risks
The complexity of automated metering systems requires dedicated technical maintenance to prevent drift in accuracy. For a distributor, a breakdown in these machines during peak season can cause immediate delays in the supply chain, highlighting the need for suppliers with robust service protocols.
Applying This Knowledge to Your Sourcing Strategy
Making the Right Choice for Your Goal
- If your primary focus is rapid market entry: Prioritize suppliers who utilize high-speed automated filling to ensure ultra-fast delivery and immediate stock availability.
- If your primary focus is premium brand positioning: Source products from facilities using high-precision quantitative technology to guarantee absolute weight consistency and superior hygiene.
- If your primary focus is supply chain stability: Seek out partners with a full-spectrum product portfolio who use industrial-grade automation to minimize product loss and maintain steady output levels.
By understanding the technical bridge between the hive and the bottle, distributors can better evaluate the reliability and market-readiness of their honey supply chain.
Summary Table:
| Key Role | Main Benefit | Impact on Distribution |
|---|---|---|
| Precision Filling | Weight Consistency | Meets high-end market standards & compliance |
| High-Speed Automation | Rapid Fulfillment | Ensures ultra-fast delivery for large orders |
| Sterile Processing | Export-Grade Quality | Prevents contamination & extends shelf life |
| Scalable Infrastructure | Increased Throughput | Supports supply chain stability for wholesalers |
Scale Your Honey Distribution with HONESTBEE
Are you a distributor, wholesaler, or B2B reseller looking for a reliable partner to streamline your supply chain? HONESTBEE provides the industry's most comprehensive full-spectrum product portfolio, designed to maximize your profit margins and operational efficiency.
From high-precision honey-filling machines and hive-making equipment to essential consumables and honey-themed merchandise, we offer one-stop sourcing capabilities backed by deep professional expertise.
Why partner with us?
- Rapid Response & Ultra-Fast Delivery: Minimize downtime and meet market demand instantly.
- Premium Quality & OEM/ODM Support: Tailored solutions with full international certifications.
- Exceptional Customer Service: Dedicated support to ensure efficient order fulfillment.
Ready to elevate your commercial apiary operations? Contact HONESTBEE today and experience the power of professional beekeeping machinery!
References
- Md Mostafizur Rahaman, Xiangsheng Wang. Threshold Dynamics of Honey Bee Colonies with General Eclosion and Social Inhibition. DOI: 10.3390/axioms14100773
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Commercial Rotary Honey Filling Machine for Production
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Automatic Honey Filling and Filtering Machine for Beekeeping Bottle Filling
- Economy Small Honey Filling Machine Honey Bottle Filler Packaging Machine
People Also Ask
- What role do commercial honey filling machines play in honey distribution? Scaling Efficiency and Quality Control
- What technical support do commercial-grade filling machines provide? Convert Honey NTFPs into Marketable Commodities
- What is the significance of specialized honey filling equipment? Scaling from Beekeeping to Commercial Success
- Why is professional honey filling machinery critical for honey production? Scale Your Apiary's Profit & Efficiency
- Why is high-capacity honey filling machinery necessary for Giant Honey Bees? Solve the Apis dorsata Volume Crisis