Tropical Apis cerana honey requires specialized processing because it usually arrives with more water and greater heat sensitivity than European honey. In humid tropical environments, Apis cerana honey commonly contains around 20% moisture, while European Apis mellifera honey is typically below 17%. That difference substantially increases fermentation and spoilage risk, so commercial processors need controlled dehumidification, low-temperature concentration, settling, filtration, and hygienic filling equipment.
The central issue is not simply that tropical honey is “wetter.” Its higher moisture content reduces storage stability, while excessive heat used to remove that water can damage enzymes such as invertase and diastase. The correct solution is controlled, low-temperature moisture reduction followed by equipment designed for consistent, hygienic packaging.
Why Tropical Honey Has a Higher Processing Requirement
Humid Conditions Increase Initial Moisture
Apis cerana colonies in tropical regions operate in environments with high atmospheric humidity. Honey harvested under these conditions can retain more water, often reaching approximately 20% moisture before processing.
European honey is commonly harvested at a lower moisture level, typically below 17%, which gives it greater natural stability during storage and transport.
Moisture Creates Fermentation Risk
Honey with excessive water provides a more favorable environment for naturally occurring yeasts. If moisture remains too high, fermentation can begin during storage, producing unwanted acidity, gas, off-flavors, and product loss.
This risk becomes more serious for distributors and wholesalers because honey may spend significant time in bulk storage, international transit, warehouses, or retail inventory.
Floral Origin Adds Further Variation
Moisture is not identical across all honey batches. Floral source, local climate, harvest timing, specific gravity, viscosity, and crystallization behavior can all vary significantly.
Commercial facilities therefore need processing systems that can adapt to incoming honey rather than relying on a single fixed treatment profile.
Why Ordinary Heating Is Not Enough
Heat Removes Water but Can Damage Quality
The simplest way to reduce moisture is to heat honey and encourage evaporation. However, uncontrolled or excessive heat can degrade heat-sensitive enzymes, including invertase and diastase.
These enzymes contribute to honey’s quality profile and are important considerations for premium, nutritional, and export-oriented products.
Vacuum Dehydration Lowers the Heat Requirement
Vacuum concentration reduces the pressure around the honey, allowing water to evaporate at a lower temperature. This helps remove excess moisture while limiting thermal exposure.
For tropical Apis cerana honey, low-temperature vacuum dehydration provides a better balance between shelf-life improvement and preservation of sensitive components.
Temperature Control Must Continue After Dehydration
Moisture reduction is only one stage of the process. Temperature-controlled settling or bulk tanks help maintain consistent viscosity, support impurity separation, and prevent unnecessary heat exposure before filtration and filling.
A properly controlled process protects the batch from both fermentation and quality loss.
What Equipment Commercial Processors Need
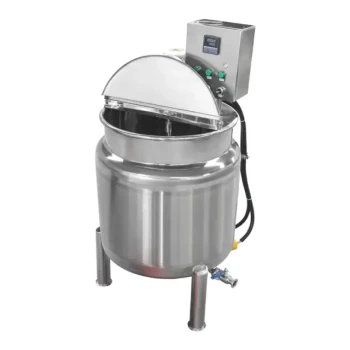
Vacuum Dehumidifiers or Concentrators
Vacuum dehumidification equipment is the core solution for reducing excess water in tropical honey. It should provide controlled pressure, stable temperature, and repeatable processing conditions across different batch sizes.
The objective is to reach a commercially stable moisture level without treating the honey as a high-temperature syrup.
Temperature-Controlled Bulk Tanks
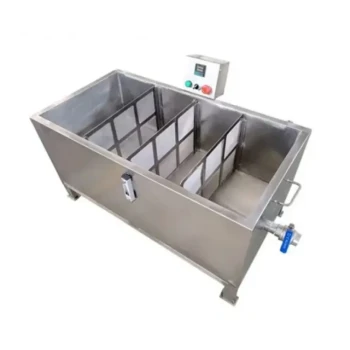
Bulk processing and settling tanks provide controlled holding conditions after extraction and during preparation for filtration. They help processors manage viscosity and maintain batch consistency.
For distributors and private-label packers, this control is particularly important because inconsistent viscosity can disrupt downstream filling and packaging operations.
Filtration Systems
Honey may contain wax particles, comb fragments, and other natural impurities after extraction. Filtration systems remove these materials before bottling and help produce a more uniform commercial product.
High-viscosity honey may require appropriately powered filtration equipment to maintain throughput without excessive aeration or unnecessary heating.
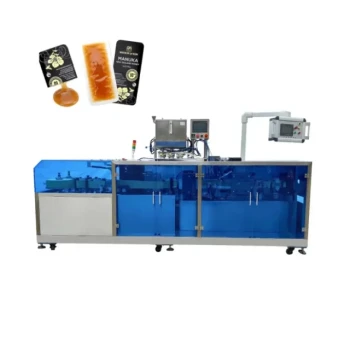
Hygienic Filling and Capping Machines
Once the honey reaches the desired condition, filling equipment must handle its viscosity accurately and hygienically. Industrial machines use food-grade, corrosion-resistant stainless steel pumps and precise volumetric nozzles to deliver consistent fills.
Automated filling and capping improve hygiene, reduce product variation, and make the transition from raw bulk honey to standardized commercial units more efficient.
Specialized Harvesting Equipment
Moisture control begins at harvest. Poor extraction or handling practices can introduce impurities or contribute to abnormal moisture increases.
Equipment suited to the bee species, hive structure, and honey consistency helps protect the raw material before it reaches the processing line.
Why Processing Must Be Matched to the Honey
Viscosity Affects Pumping and Filling
Honey viscosity varies according to moisture level, temperature, and botanical origin. Higher-viscosity honey places greater demands on pumps, filters, valves, and filling nozzles.
Using equipment designed for honey rather than general-purpose liquids reduces filling errors, contamination risk, and production interruptions.
Crystallization Affects Consistency
Some honey varieties crystallize more quickly than others. Temperature-controlled stirring or holding facilities may be needed to maintain a consistent texture and prevent blockages or uneven filling.
The correct machinery helps processors preserve a stable product without relying on excessive heat.
Standardization Supports Commercial Value
Processing equipment transforms variable raw honey into a product with more consistent moisture, appearance, weight, hygiene, and shelf stability.
That standardization makes the honey easier to distribute, package under private labels, position in premium channels, and manage across international supply chains.
Understanding the Trade-offs
Moisture Reduction Must Not Become Overprocessing
Removing too little water leaves the honey vulnerable to fermentation. Removing water with excessive heat can reduce enzyme activity and compromise the qualities that support premium positioning.
The practical requirement is controlled dehydration, not maximum dehydration.
Faster Processing Can Increase Thermal Exposure
High-throughput systems may appear attractive when handling large volumes, but speed must be balanced against temperature, residence time, and batch uniformity.
A reliable supplier should specify operating conditions and throughput together rather than treating capacity as the only performance measure.
Automation Requires Product-Specific Configuration
A filling machine that works well for one honey may perform poorly with another because of differences in viscosity, crystallization, and moisture. Pump type, nozzle design, filtration capacity, and temperature control may all need adjustment.
Equipment selection should therefore follow the honey’s physical characteristics and the intended package format.
Equipment Quality Affects the Whole Supply Chain
A weak moisture-reduction stage can cause fermentation claims, rejected batches, and shortened shelf life. An unsuitable filling line can create underfilled containers, inconsistent weights, contamination risks, or delays in order fulfillment.
For B2B buyers, the relevant evaluation is the performance of the complete processing system, not the specifications of one machine in isolation.
Making the Right Choice for Your Goal
The best equipment package depends on the condition of the incoming honey, the required output, and the market standards for the finished product.
- If your primary focus is shelf stability: Prioritize low-temperature vacuum dehydration and accurate moisture monitoring to reduce fermentation risk without unnecessary heat exposure.
- If your primary focus is enzyme and quality preservation: Choose vacuum concentration, controlled tank temperatures, and short, well-managed thermal residence times.
- If your primary focus is production efficiency: Integrate extraction, filtration, bulk holding, filling, and capping equipment so that each stage supports the next.
- If your primary focus is export or premium packaging: Select hygienic stainless-steel contact parts, precise filling systems, repeatable batch controls, and documentation suitable for commercial quality assurance.
- If your primary focus is multi-variety processing: Choose modular equipment that can accommodate changes in viscosity, crystallization behavior, floral origin, and moisture content.
With the right low-temperature moisture-control and packaging system, tropical Apis cerana honey can be converted from a storage-sensitive raw product into a stable, consistent, and commercially competitive honey.
Summary Table:
| Factor | Tropical Apis cerana Honey | European Apis mellifera Honey |
|---|---|---|
| Typical Moisture Content | ~20% | Below 17% |
| Fermentation Risk | High without processing | Lower natural stability |
| Heat Sensitivity | Sensitive enzymes (invertase, diastase) | More tolerant but still affected |
| Recommended Processing | Low-temperature vacuum dehydration, controlled settling, filtration, hygienic filling | Conventional processing may suffice |
| Outcome | Stable, premium-grade honey with preserved quality | Naturally stable, easier to store |
Ensure your tropical honey meets the highest standards of quality and shelf stability. At HONESTBEE, we specialize in providing comprehensive beekeeping equipment and processing machinery tailored to the unique challenges of Apis cerana honey. From low-temperature vacuum dehydrators to hygienic filling lines, our one-stop sourcing and expert support guarantee efficient, reliable production. For B2B distributors and wholesalers, we offer OEM/ODM customization, certified quality, and rapid fulfillment to keep your supply chain moving. Contact us today to optimize your honey processing and boost your profit margins—get in touch with our specialists!
Related Products
- High Quality Honey Dehumidifier Dryer Thickening Machine for Beekeeping
- Honey Concentrating and Filtering Dehumidifier Machine 2T Capacity for Honey
- 0.5T Capacity Honey Dehumidifier Dryer with Vacuum Heating and Thickening Filtering Machine
- Honey Concentrating Vacuum Heating Thickening Machine Dehumidifier for Honey
- Economy Small Scale Honey Dryer Dehumidifier Thickening Machine
People Also Ask
- Can you dehumidify honey? A Beekeeper's Guide to Preventing Fermentation
- How to dry up honey? The Safe Guide to Stabilizing Honey and Preventing Fermentation
- How can the moisture content of honey be reduced? A Guide to Safe, Effective Drying Methods
- How to remove humidity from honey? Protect Your Harvest from Fermentation
- What is the process for using a dehumidifier to lower honey's moisture content? Expert Drying Techniques