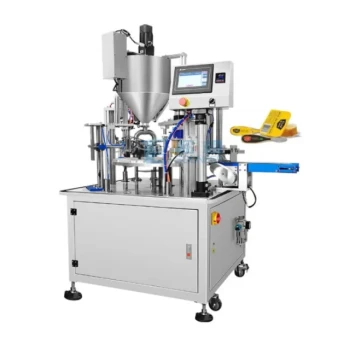
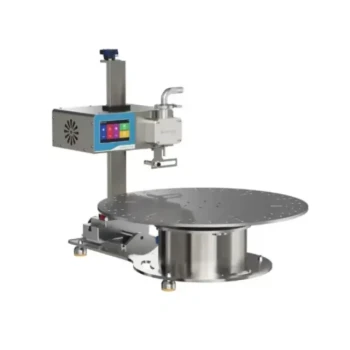
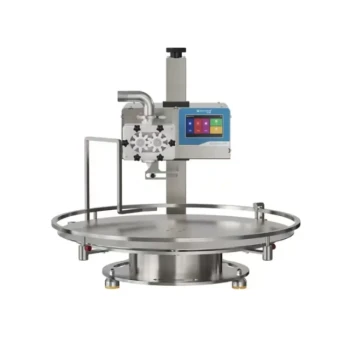
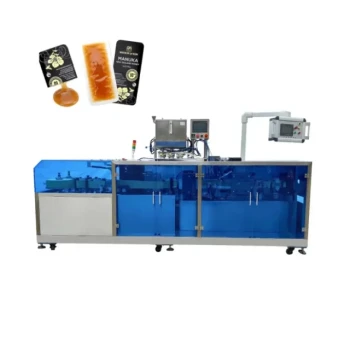
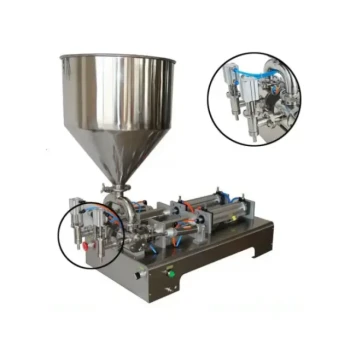
High-precision honey filling and packaging machines act as the critical bridge between raw apiary output and high-value commercial assets. These machines utilize automated dosage control and sterile sealing to ensure every unit meets strict food safety and weight consistency standards. By transforming bulk honey into standardized, retail-ready products, this technology enables honey producers to access high-end global markets and maximize the economic value of their harvest.
The integration of high-precision machinery shifts honey production from manual, high-risk processes to standardized industrial excellence. This transition not only protects product integrity and brand reputation but also provides the scalable infrastructure necessary for distributors to meet the demands of modern retail and electronic trading platforms.
Enhancing Product Integrity and Safety
Eliminating Contamination Risks
Automated filling systems operate in closed, sterile environments that effectively eliminate the cross-contamination risks associated with manual handling. By reducing human contact, these machines ensure that delicate products like honey, propolis, and bee pollen remain pure and compliant with international food hygiene regulations.
Preserving Biochemical Quality
Precision sealing processes prevent moisture absorption and secondary contamination, which are vital for maintaining the honey's natural composition. This rigorous control ensures that biochemical indicators, such as Hydroxymethylfurfural (HMF) levels, remain within optimal ranges for premium market acceptance.
Supporting Sustainable Agriculture
By increasing the economic output per hive, these machines provide beekeepers with the financial incentive to maintain sustainable, bee-friendly practices. This economic stability supports the conservation of bee resources and ensures a long-term, reliable supply chain for wholesalers and distributors.
Driving Commercial Standardization and Brand Value
Precision Dosage and Waste Reduction
High-precision technology ensures consistent volumetric dispensing, which significantly reduces raw material loss during the packaging phase. For B2B resellers, this weight consistency is essential for maintaining transparent pricing and fulfilling large-scale orders without discrepancies.
Packaging Uniformity for High-End Retail
Uniform packaging is a prerequisite for establishing a professional brand image in competitive retail environments. Automated machines produce standardized containers that meet the aesthetic and functional requirements of high-end commercial channels and global export standards.
Scaling for Rapid Fulfillment
Industrial machines are optimized for high-speed production, particularly for small packaging sizes under 500 grams that dominate the retail market. This efficiency allows distributors to respond rapidly to market fluctuations and manage high-volume orders with ultra-fast delivery times.
Understanding the Trade-offs
High Initial Capital Investment
Implementing high-precision machinery requires a significant upfront financial commitment compared to traditional manual methods. While the long-term ROI is high through reduced waste and labor costs, it necessitates a strategic approach to capital allocation and sourcing.
Technical Maintenance Requirements
Advanced automation requires specialized technical expertise for setup, calibration, and ongoing maintenance to ensure continued accuracy. Distributors must partner with suppliers who offer comprehensive technical support and deep industry expertise to avoid production downtime.
Complexity in Multi-Product Lines
While these machines are highly efficient for standardized runs, switching between different honey types or bottle shapes can require complex adjustments. Finding a "one-stop" solution that offers versatile equipment is critical for businesses dealing with diverse product portfolios.
How to Apply This to Your Sourcing Strategy
Choosing the right technical infrastructure is a strategic decision that impacts every tier of your supply chain. To maximize your competitive advantage, align your equipment sourcing with your specific business trajectory.
- If your primary focus is international market entry: Prioritize machines that guarantee compliance with global food safety standards and provide the sterile packaging required for long-term storage stability.
- If your primary focus is rapid order fulfillment: Invest in high-speed, automated systems optimized for small-unit retail packaging to ensure your supply chain can handle the demands of large-scale electronic trading platforms.
- If your primary focus is building a premium brand: Focus on equipment that offers the highest level of dosage precision and superior sealing integrity to ensure a consistent, high-quality experience for the end consumer.
Empowering your production line with high-precision technology is the definitive step toward securing a dominant and sustainable position in the global honey trade.
Summary Table:
| Impact Category | Key Technical Benefit | Commercial Outcome for Distributors |
|---|---|---|
| Product Integrity | Sterile, closed-loop filling | International food safety compliance & brand trust |
| Standardization | High-precision dosage control | Minimal raw material waste & uniform retail pricing |
| Operational Speed | High-speed automated output | Rapid fulfillment of large-scale e-commerce orders |
| Market Value | Premium sealing & aesthetics | Higher retail margins & long-term storage stability |
Scale Your Honey Business with HONESTBEE’s Industrial Solutions
Maximize your profit margins and supply chain reliability with HONESTBEE, your premium one-stop partner for commercial beekeeping technology. We provide a full spectrum of high-precision honey-filling and honey-making machines, alongside a comprehensive range of industry consumables and specialized hardware.
Designed specifically for distributors, wholesalers, and B2B resellers, our solutions offer:
- Deep Industry Expertise: Specialized equipment tailored to global export standards.
- Rapid Fulfillment: Ultra-fast delivery and dedicated support to keep your production lines moving.
- Comprehensive Sourcing: From hive-making machines to honey-themed cultural merchandise.
Ready to elevate your production value? Contact HONESTBEE today to discuss our wholesale offerings and OEM/ODM support!
References
- Damayanti Buchori, Dewi Sartiami. Strategi Konservasi dan Pelestarian Lebah di Indonesia. DOI: 10.29244/agro-maritim.0503.690-694
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Precision Automated Packaging Turntable Honey Spoon Filling Sealing Packing Machine
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
- Commercial Rotary Honey Filling Machine for Production
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Automatic Single-Dose Snap & Squeeze Honey Sachets Packing Machine
People Also Ask
- Why is the use of professional filling and sealing packaging machinery necessary for the production of high-value honey?
- What role do automated filling and packaging machines play in the honey supply chain? Scale Your Retail Distribution
- What are the benefits of automated honey filling and packaging? Scale Your Apiary with Industrial Precision
- What role do professional automated filling and packaging machines play in honey processing? Boost Efficiency & Value
- How do automated honey filling and packaging machines contribute to the market value of honey products? Maximize Your ROI