Stingless bee honey is typically more dilute and fermentation-prone than Apis honey. Compared with conventional Apis honey, including Apis mellifera, stingless bee “pot-honey” generally has higher moisture content and lower viscosity, while retaining distinctive bioactive compounds and strong antibacterial activity. Commercial packaging therefore requires tighter moisture management, gentle handling, sanitary filling, and reliable airtight sealing.
The central difference is moisture and handling behavior: stingless bee honey’s higher water content gives it a thinner consistency and greater spoilage risk. A commercial line must therefore combine specialized extraction with moisture control, gentle filtration, precision filling, and hygienic sealing.
How Stingless Bee Honey Differs from Apis Honey
Higher moisture content
Stingless bee honey typically contains more water than standard Apis honey. Some reported stingless bee honeys reach approximately 30% moisture, although the actual value varies by species, floral source, climate, harvest maturity, and storage conditions.
This higher moisture content increases the likelihood of fermentation and spoilage if the product is not processed and sealed appropriately.
Lower viscosity and different flow behavior
Because it contains more water, stingless bee honey is generally less viscous and more fluid than conventional Apis honey. This affects pumping, filtration, filling accuracy, container selection, and sealing.
Equipment designed only for thick Apis honey may not provide reliable metering or clean shutoff when handling a thinner product.
Distinctive bioactive profile
Stingless bee honey can contain bioactive substances associated with its propolis and botanical sources, including flavonoids, phenolic acids, and compounds such as mangostin in relevant regional products.
These compounds contribute to its reported broad-spectrum antibacterial activity and support its premium positioning. However, the composition is not uniform; it depends strongly on bee species, forage, geography, and post-harvest treatment.
A premium product with lower production volume
Stingless bee colonies generally produce far less honey than Apis mellifera colonies. Reported annual yields can be around 2 kg per hive for some stingless bee operations, compared with the much larger commercial output possible from Apis colonies.
The lower yield and distinctive sensory and bioactive characteristics often support a higher unit price, but they also make loss through leakage, fermentation, or contamination particularly costly.
Why Stingless Bee Honey Requires Different Processing
The honey is stored in individual pots
Apis bees store honey in vertical comb frames that can commonly be uncapped and extracted using centrifugal honey extractors. Stingless bees instead store honey in separate spherical or oval cerumen pots.
These pots cannot be processed efficiently with standard frame-based extraction systems. The cerumen containers must be punctured, suctioned, or pressed using equipment that removes the honey without unnecessarily damaging the brood area or hive structure.
Moisture control is a primary process step
Commercial processors should measure and manage moisture before filling. Depending on the product specification, this may involve a moisture-control or dehumidification unit designed to reduce fermentation risk while avoiding unnecessary damage to the honey’s desirable characteristics.
The correct process must be validated for the specific honey. Excessive heat or aggressive treatment may alter sensory qualities and reduce the value of heat-sensitive components.
Filtration must be effective but gentle
Stingless bee honey may contain wax, cerumen fragments, pollen, and other suspended material from the storage pots. A gentle sanitary filtration system is needed to remove unwanted particles without unnecessarily stripping the product’s natural character.
Filtration should be selected according to the desired appearance, final package, and product positioning. Premium minimally processed honey may require a different filtration specification from a highly clarified retail product.
Equipment Required for Commercial Packaging
Specialized extraction equipment
The initial equipment requirement is not the same as the equipment used for conventional Apis honey. Commercial operations generally need:
- Pot puncturing or opening equipment
- Low-shear suction or transfer pumps
- Pressing or draining equipment, where appropriate
- Food-grade collection tanks
- Coarse pre-filtration equipment
The equipment should accommodate the delicate cerumen pots and the relatively fluid honey without excessive aeration or contamination.
Moisture-control equipment
A commercial line should include a means of monitoring and, where necessary, controlling moisture. Typical requirements include:
- Honey moisture measurement
- Controlled moisture-reduction equipment
- Temperature and process monitoring
- Closed product-transfer systems
Moisture control is not simply a quality upgrade; it is a shelf-life and distribution requirement for a high-moisture product.
Gentle filtration equipment
A suitable filtration section may include:
- Sanitary coarse filters
- Fine filtration, if required by the product specification
- Food-grade piping and valves
- Cleanable filter housings
- Closed transfer lines
The filtration system should be sized for the lower viscosity of stingless bee honey and configured to minimize product retention and unnecessary exposure to air.
Sanitary filling equipment
Commercial packaging requires a precision honey-filling machine capable of handling fluid, variable-viscosity honey. Important capabilities include:
- Accurate volumetric or mass-based metering
- Adjustable filling parameters
- Anti-drip or clean-shutoff functions
- Compatibility with glass jars, squeeze containers, or other approved formats
- Food-contact stainless steel construction
- Cleanable product-contact components
Accurate filling protects margins, supports consistent labeling, and helps distributors meet retail and export requirements.
Airtight capping and sealing equipment
Because stingless bee honey is more susceptible to fermentation and leakage, filling must be followed by dependable closure. The packaging line may require:
- Automatic or semi-automatic capping equipment
- Torque control
- Induction or tamper-evident sealing
- Leak inspection
- Date, batch, and traceability coding
Airtight sealing limits exposure to external contamination and helps prevent moisture exchange during storage and transport.
Hygienic handling and quality-control systems
The packaging equipment should operate as part of a controlled hygienic system, including:
- Sanitary holding tanks
- Closed transfers
- Clean-in-place or validated cleaning procedures
- Batch traceability
- Moisture and fill-weight checks
- Container and closure inspection
Packaging protects more than appearance. It helps preserve the product’s physicochemical properties and reduces the risk of secondary contamination.
Understanding the Trade-offs
Moisture reduction versus natural product quality
Reducing moisture can improve stability, but aggressive processing can affect flavor, aroma, color, and sensitive bioactive compounds. Processors should establish a moisture target and treatment method based on the product’s intended market and labeling claims.
The objective is not to process stingless bee honey until it behaves exactly like Apis honey. The objective is to achieve a stable, safe, and commercially consistent product while preserving its distinctive value.
Fine filtration versus premium positioning
Highly filtered honey may look cleaner and be easier to standardize, but excessive filtration can change the product’s natural sensory and particulate profile. A premium raw or minimally processed product may require a gentler specification.
The correct filtration level should be agreed with the buyer, retailer, and regulatory market before equipment is selected.
Standardization versus batch variability
Stingless bee honey varies with floral source, season, geography, and bee species. This variability can be part of the product’s appeal, but it complicates automated filling and shelf-life control.
Distributors and wholesalers should request representative batch data rather than relying on a single specification sheet.
Conventional equipment may be unsuitable
A standard Apis honey extractor may not work with cerumen pots, and a filler configured for thick honey may deliver inconsistent volumes with more fluid stingless bee honey.
The safest approach is to specify the entire process—from pot opening through final sealing—rather than purchasing a filling machine in isolation.
Selecting a Commercial Line
Match equipment to the product format
The required machinery depends on whether the honey will be sold as:
- Raw or minimally processed honey
- Moisture-controlled honey
- Filtered retail honey
- Small premium jars
- Larger wholesale or food-service containers
Container size, viscosity, target throughput, and closure type should be defined before requesting quotations.
Prioritize sanitary design
For a high-moisture honey, hygienic design is essential. Select equipment with accessible product-contact parts, food-grade materials, reliable seals, and a documented cleaning procedure.
Suppliers should be able to provide technical specifications, commissioning support, spare parts, and responsive after-sales service.
Consider a complete sourcing package
For distributors, resellers, and commercial beekeepers, a practical procurement package may include:
- Stingless bee hive and honey-pot handling equipment
- Extraction and transfer systems
- Moisture-control equipment
- Gentle filtration
- Holding tanks
- Precision filling
- Capping and tamper-evident sealing
- Coding, labeling, and inspection equipment
A one-stop equipment source can simplify line compatibility, shorten installation time, and improve order fulfillment across multiple processing stages.
How to Apply This to Your Project
The equipment should be selected around moisture, viscosity, pot-based extraction, hygiene, and final distribution requirements.
- If your primary focus is premium raw honey: Choose gentle pot extraction, low-shear transfer, limited filtration, and sanitary filling that preserves the product’s natural sensory and bioactive characteristics.
- If your primary focus is shelf life and export distribution: Prioritize validated moisture control, airtight tamper-evident sealing, batch traceability, and inspection systems that reduce fermentation, leakage, and contamination risks.
- If your primary focus is scalable commercial production: Specify an integrated line with compatible extraction, filtration, filling, capping, and cleaning systems rather than adapting conventional Apis equipment piecemeal.
With the right process design, stingless bee honey’s higher moisture and unique composition can be managed as commercial advantages rather than operational liabilities.
Summary Table:
| Aspect | Stingless Bee Honey | Apis Honey |
|---|---|---|
| Moisture content | Typically ~30% or higher | Generally lower (<20%) |
| Viscosity | Low, more fluid | Thick, high viscosity |
| Storage | In cerumen pots | In vertical comb frames |
| Extraction | Requires puncturing/suctioning | Centrifugal extraction |
| Fermentation risk | High due to moisture | Lower |
| Bioactive compounds | Distinctive, potent | Varies, usually less |
| Production volume | Low (~2 kg/hive/year) | High |
Ensure your stingless bee honey line is built for success. At HONESTBEE, we provide a comprehensive range of specialized equipment—from pot extraction and moisture control to gentle filtration and precision filling—tailored for B2B buyers like distributors and commercial beekeepers. With our one-stop sourcing, rapid response, dedicated support, and ultra-fast delivery, you can achieve high-quality, shelf-stable products while maximizing your margins. Contact us today to discuss your requirements and get a customized solution. Contact us now.
Related Products
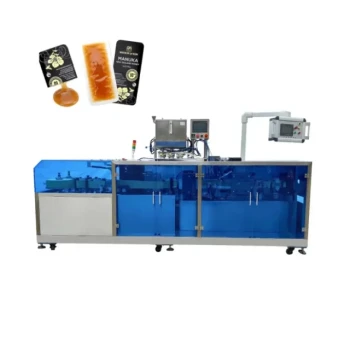
- Double Nozzle Small Honey Filling Machine Honey Sachet Packing Packaging Equipment
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Small Honey Filling Machine Sachet Packing Equipment Single Nozzle
- Automatic Single-Dose Snap & Squeeze Honey Sachets Packing Machine
- Heavy Duty Stainless Steel Honey Processing Machine Decrystallizing Tank
People Also Ask
- How does industrial honey-filling machinery support Robinia pseudoacacia stands? Maximize Your Acacia Honey Yield
- What value do retail packaging equipment and filling technologies provide in the honey distribution process? Maximize ROI
- What is honey filling equipment used for? Optimize Your Bottling with Precision Automation
- What role does precision filling equipment play in cost control? Maximize Honey Profits & Market Growth
- Why is high-precision honey filling equipment necessary? Secure the medicinal value and ROI of stingless bee honey.