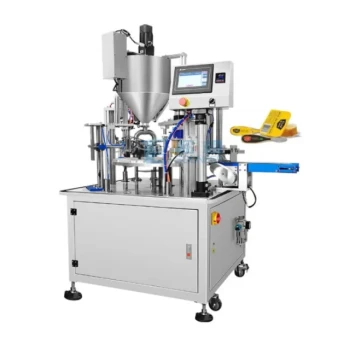
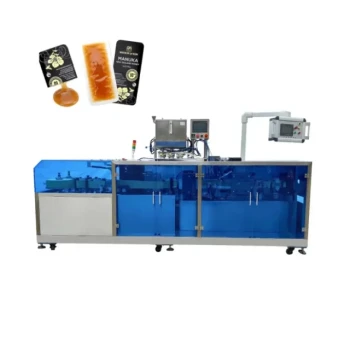
Industrial-grade automatic filling equipment is the technological cornerstone for transforming raw organic honey into a high-margin, export-ready commodity. By utilizing closed-loop systems and high-precision dosage control, this machinery eliminates the risk of secondary contamination while ensuring every unit meets strict international weight and measurement standards. For distributors and wholesalers, this technology represents the vital link between traditional apiary production and the rigorous demands of the premium global retail market.
Core Takeaway: Industrial-grade filling equipment secures the commercial value of organic honey by combining sterile, high-speed processing with precise measurement. This ensures a standardized, high-quality product that meets the traceability and hygiene requirements of the most demanding B2B supply chains.
Securing Organic Integrity and Product Safety
Closed-Loop Aseptic Environments
Modern automatic filling machines utilize a closed-loop system to move honey from storage tanks to final containers. This environment is critical for organic products as it prevents secondary contamination from human contact or airborne pollutants.
Preservation of Biological Activity
Honey is a delicate biological product sensitive to oxidation and excessive processing. High-quality automated systems are designed to maintain the natural biological activity and flavor profiles of organic honey by minimizing air exposure and ensuring gentle handling during the transfer process.
Advanced Hygienic Sealing
Beyond the filling process, industrial-grade equipment integrates advanced sealing technologies that provide a tamper-evident, airtight finish. This technical capability is essential for ensuring product longevity and maintaining safety standards throughout the long-distance shipping cycles common in international distribution.
Maximizing Commercial Scalability and Consistency
High-Precision Quantitative Control
B2B resellers depend on weight consistency to maintain trust with retail partners and adhere to strict consumer protection laws. Automated filling machines employ high-precision metering systems that guarantee every bottle contains the exact specified volume, eliminating the "giveaway" or under-filling common in manual operations.
High-Speed Production Throughput
The ability to rapidly convert biological yield into economic stock is a competitive necessity. Industrial-grade equipment significantly increases production line throughput, allowing large-scale beekeeping operations to process high volumes of honey during peak harvest seasons without bottlenecks.
Standardized Packaging for Premium Markets
Automation ensures that every unit is visually identical, from the fill level to the label placement. This aesthetic standardization is a prerequisite for entry into high-end retail markets, where packaging quality is often viewed as a proxy for the quality of the honey itself.
Facilitating Global Supply Chain Integration
Meeting International Export Standards
To enter the international export market, honey must meet diverse and complex quality traceability requirements. Automated systems often feature integrated data logging that helps beekeeping units document the filling process, providing the transparency required by global regulators.
Reducing Operational Overhead
By replacing labor-intensive manual filling with specialized machinery, producers can significantly reduce manual labor costs and fixed asset investments over time. For distributors, this leads to more stable pricing and a more reliable supply chain, as production is less dependent on the availability of manual labor.
Supporting Full-Spectrum Portfolios
Wholesalers benefit from one-stop sourcing when producers use versatile filling equipment capable of handling various container sizes and honey viscosities. This flexibility allows a single facility to produce a comprehensive product portfolio, from small retail jars to bulk commercial pails, all within the same technical ecosystem.
Understanding Technical Trade-offs
Capital Investment vs. Long-Term Yield
The primary hurdle for many operations is the initial fixed asset investment required for industrial-grade machinery. While the cost is higher than manual setups, the ROI is realized through increased efficiency, reduced waste, and access to higher-paying premium markets that reject non-standardized products.
Maintenance and Technical Expertise
Automated systems require a higher level of technical expertise for setup, calibration, and routine maintenance. Distributors should partner with suppliers who offer dedicated customer service and rapid response times to ensure that production downtime is minimized and order fulfillment remains efficient.
Complexity in Small-Batch Customization
While these machines excel at high-volume standardization, they may require significant downtime for recalibration when switching between drastically different packaging formats. Producers must balance the need for operational speed with the market demand for diverse packaging styles.
How to Apply This to Your Distribution Strategy
Making the Right Choice for Your Goal
- If your primary focus is High-End Retail Distribution: Prioritize suppliers using equipment with high-precision dosage and aseptic sealing to ensure premium shelf presence and safety.
- If your primary focus is Large-Scale Bulk Export: Focus on sourcing from partners with high-throughput machinery that can fulfill large orders with ultra-fast delivery times.
- If your primary focus is Brand Integrity and Traceability: Select producers who utilize automated data-logging systems to provide the transparency required for organic and origin-certified products.
By integrating industrial-grade automation into the honey value chain, distributors can guarantee a professional, standardized, and safe product that meets the highest global commercial standards.
Summary Table:
| Key Technical Feature | Commercial Benefit | Impact on B2B Value Chain |
|---|---|---|
| Closed-Loop System | Prevents secondary contamination | Guarantees organic integrity and product safety |
| Precision Dosage Control | Eliminates product waste/under-filling | Ensures weight consistency and legal compliance |
| High-Speed Throughput | Rapidly converts yield to stock | Enables ultra-fast delivery for large-scale orders |
| Aseptic Sealing | Extends shelf life and tamper evidence | Vital for long-distance international shipping |
| Integrated Data Logging | Provides full process transparency | Simplifies traceability for premium export markets |
Scale Your Honey Business with HONESTBEE
Are you looking to streamline your honey processing or expand your wholesale inventory? HONESTBEE offers a comprehensive one-stop sourcing solution for commercial apiaries and B2B distributors worldwide.
We provide a full spectrum of professional equipment, including high-precision honey-filling machines, specialized hive-making hardware, and a complete range of beekeeping consumables and cultural merchandise. By partnering with us, you benefit from:
- Industry Expertise: Decades of professional knowledge to guide your technical investments.
- Rapid Fulfillment: Ultra-fast delivery and efficient order processing to keep your supply chain moving.
- Exceptional Service: Dedicated support to ensure your machinery operates at peak performance.
Ready to enhance your profit margins and supply reliability? Contact HONESTBEE today to explore our wholesale offerings and premium trading services!
References
- Roberta Milardo. The Role of Knowledge and Innovation in Organic Farming Systems: A Systematic Literature Review. DOI: 10.3390/su17146563
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
- Commercial Rotary Honey Filling Machine for Production
- Double Nozzle Small Honey Filling Machine Honey Sachet Packing Packaging Equipment
- Small Honey Filling Machine Sachet Packing Equipment Single Nozzle
- Fully Automatic Honey Filling Packaging Machine for Processing Line
People Also Ask
- What are the common types of bottling machines used for honey? Choosing the Right Solution for Your Apiary
- How do high-precision honey filling machines ensure quality? Optimize Your Commercial Production with HONESTBEE
- What quality control role does professional honey filling equipment perform? Ensure Consistency and Product Stability
- What is a key feature of the new generation of the honey filling machine? The Advanced Electronic Control Unit
- How do honey filling machines work? Achieve Precision & Speed for Your Apiary