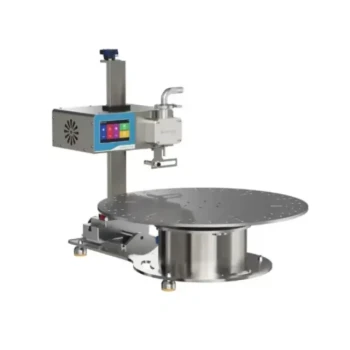
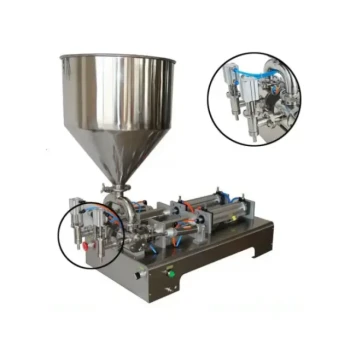
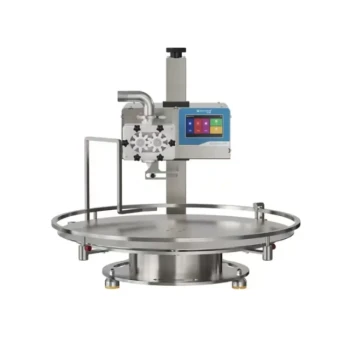
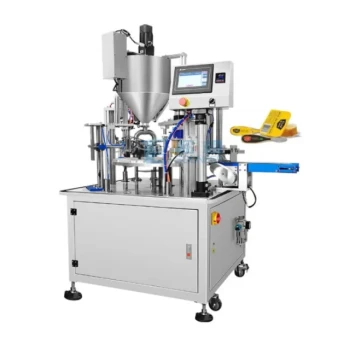
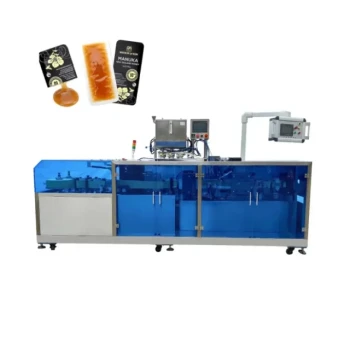
Professional honey filling and bottling lines provide the essential technical foundation for scaling production by ensuring high-precision metering, sterile packaging environments, and consistent product quality. These systems automate the transition from raw honey to retail-ready goods, utilizing advanced volumetric pumping and temperature controls to handle high-viscosity fluids without waste. By integrating these technologies, large-scale producers can meet the rigorous hygiene and weight standards required for international distribution and premium retail placement.
A professional bottling line is more than a speed upgrade; it is a quality assurance system that protects the honey’s physicochemical stability while maximizing operational efficiency. It bridges the gap between artisanal harvesting and industrial-scale commercialization.
Maximizing Operational Precision and Material Efficiency
Advanced Viscosity Management
Honey is a non-Newtonian fluid that presents unique challenges such as "wall-clinging" and overflow during the filling process. Professional lines use precision metering systems specifically designed for high-viscosity liquids to ensure every drop is accounted for. This technology minimizes raw material waste, which is a critical factor in maintaining profitability during large-scale runs.
Weight Consistency and Legal Compliance
Automated lines utilize high-precision volumetric pumping or weight sensors to achieve extreme consistency across thousands of units. This level of accuracy ensures that every bottle meets strict net-weight regulations, protecting distributors from legal non-compliance and consumer dissatisfaction. Consistency in filling levels also enhances the visual appeal of the product on retail shelves.
Labor Optimization and Throughput
Replacing manual or semi-automated processes with a fully automated line significantly reduces long-term labor requirements. This allows producers to focus their energy on supply chain reliability and quality control rather than repetitive manual tasks. The resulting increase in packaging speed is vital for meeting the rapid response times demanded by modern wholesalers.
Safeguarding Product Integrity and Hygiene
Sterile Environments and Contamination Control
Professional bottling lines operate within a closed-pipe design, which drastically reduces contact between the honey and the external environment. This prevents secondary contamination from microbes like yeast and airborne impurities, ensuring the product meets international food safety standards. For distributors, this means a more stable product with a significantly lower risk of costly recalls.
Maintaining Physicochemical Stability
Honey is sensitive to environmental factors; professional lines integrate filtration and temperature control systems to preserve its natural properties. By preventing overheating during the filling process, these machines ensure that nutritional components are not degraded and that moisture content remains within legal limits. This technical expertise results in a premium product that maintains its clarity and flavor over time.
Extension of Shelf Life
The standardization of the bottling process, combined with airtight sealing technology, effectively extends the shelf life of honey products. This is a crucial advantage for B2B resellers who manage long-distance logistics and large-scale inventory. A longer shelf life provides more flexibility in the supply chain and reduces the risk of inventory spoilage.
Understanding the Trade-offs and Challenges
Significant Initial Capital Investment
The primary barrier to implementing a professional honey filling line is the high upfront cost of industrial-grade machinery. While these systems offer long-term savings through reduced labor and waste, they require a substantial commitment of capital and a clear strategy for ROI.
Technical Expertise and Maintenance Requirements
Sophisticated automated systems demand specialized knowledge for setup, calibration, and ongoing maintenance. Producers must ensure they have access to professional industry expertise to prevent downtime. Any technical failure in an integrated line can stall the entire production process, making a dedicated service partner essential.
Making the Right Choice for Your Distribution Strategy
To thrive in the competitive honey market, your equipment or sourcing choices must align with your specific business objectives and the needs of your retail partners.
- If your primary focus is entering supermarket supply chains: Prioritize lines that offer certified sterile environments and high-precision sealing to meet rigorous retail audit requirements.
- If your primary focus is maximizing profit margins on high-volume orders: Invest in high-speed automated lines that feature precision metering to minimize material waste and reduce labor overhead.
- If your primary focus is brand consistency and premium positioning: Look for systems that offer superior aesthetics in filling and labeling, ensuring a professional image that justifies a higher price point.
By leveraging professional filling technology, producers and distributors can ensure their honey meets the highest global standards for quality, safety, and efficiency.
Summary Table:
| Advantage | Technical Feature | Business Impact |
|---|---|---|
| High Precision | Volumetric pumping & weight sensors | Minimizes material waste and ensures legal weight compliance. |
| Hygiene & Safety | Closed-pipe design & sterile environment | Prevents contamination and meets international food safety standards. |
| Operational Efficiency | Full automation & high throughput | Reduces labor costs and enables rapid response for high-volume orders. |
| Product Integrity | Integrated filtration & temp control | Preserves honey’s natural nutrients and extends shelf life for logistics. |
Scale Your Honey Distribution with HONESTBEE Expertise
Are you looking to optimize your supply chain or upgrade your production capabilities? HONESTBEE caters to commercial apiaries and B2B distributors with a comprehensive one-stop sourcing solution.
From high-precision honey-filling and hive-making machines to a full spectrum of beekeeping tools and essential consumables, we provide the hardware and expertise needed to dominate the market.
Why partner with HONESTBEE?
- Comprehensive Portfolio: Everything from specialized machinery to honey-themed merchandise.
- B2B Optimized: Dedicated support for wholesalers with premium trading services and OEM/ODM capabilities.
- Rapid Fulfillment: Ultra-fast delivery and efficient order processing to keep your inventory moving.
- Industry Expertise: Professional guidance to ensure your equipment meets rigorous retail audits.
Contact our team today to streamline your sourcing!
References
- Edymeiko de Souza Maciel, Gardênia Holanda Cabral. Overview of bee research in Roraima, Brazil. DOI: 10.18227/1982-8470ragro.v19i00.8471
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Automatic Honey Filling and Filtering Machine for Beekeeping Bottle Filling
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
- Double Nozzle Small Honey Filling Machine Honey Sachet Packing Packaging Equipment
- Semi Automatic Small Honey Bottle Filling Machine Honey Filler
People Also Ask
- Why are fully automatic honey filling and packaging lines essential? Boost Your Honey's Market Value and Quality
- What is a fully-automatic honey filler? Streamline Your Production with High-Precision Automation
- How do automated honey filling and packaging machines affect profitability? Boost Margins with HONESTBEE Technology
- How do automated honey filling and packaging machines contribute to the market value of honey products? Maximize Your ROI
- How do industrial-grade automated honey filling and packaging machines mitigate the risk of physical contamination?