Specialized hives are the foundational infrastructure of the Australian stingless bee industry. These scientifically engineered units provide a controlled environment that simulates natural tree cavities, supporting the complex construction of wax and propolis structures by Meliponini colonies. For commercial operators, these hives are the essential hardware required to transition from wild colony management to standardized, large-scale production of Sugarbag honey and geopropolis.
Specialized hives transform a wild resource into a scalable commercial asset by providing the uniformity needed for industrial management and sustainable harvesting. For distributors, these hives represent the core of a professional beekeeping supply chain, ensuring colony health and product traceability.
Replicating the Microenvironment for Colony Stability
Simulating Natural Habitats
Specialized hives are designed to mimic the microenvironment of natural tree hollows, which are the traditional nesting sites for Australian stingless bees. This simulation is critical because these bees are highly sensitive to temperature and humidity fluctuations. By providing a stable internal climate, the hives ensure the survival and reproduction of colonies, particularly those rescued from damaged or felled timber.
Protection from External Stressors
Unlike wild nesting sites, specialized artificial hives provide a fortified barrier against external predators and extreme weather conditions. This protection is vital for maintaining the health of the Trigona genus and other Meliponini species in commercial settings. A secure hive environment reduces colony stress, allowing the bees to focus energy on honey and propolis production rather than defense or repair.
Commercial Standardization and Industrial Scalability
The Impact of Standardized Machinery
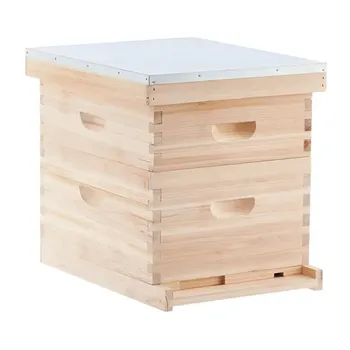
The use of specialized hive-making machinery allows for the large-scale production of uniform hive components. For distributors and wholesalers, this standardization is key to providing a reliable product portfolio that meets the needs of commercial apiaries. Uniformity in hive volume and structure ensures that beekeepers can predict yields and manage hundreds of colonies with the same operational protocols.
Optimizing Management Efficiency
Standardized hive boxes facilitate routine inspection and maintenance, which is the bottleneck of any large-scale operation. When every hive in an apiary is identical, management tasks become repetitive and faster, significantly reducing labor costs. This efficiency is what enables the establishment of pesticide-free, traceable production chains that satisfy modern market demands.
Enhancing Yield and Sustainable Propagation
Modular Design for Colony Splitting
One of the most significant roles of specialized hives is facilitating artificial colony splitting and propagation. Modular designs allow beekeepers to separate hive sections easily, encouraging the growth of new colonies without the risk of destroying the mother hive. This capability is essential for distributors looking to support the rapid expansion of the stingless bee market.
Precision Harvesting of Honey and Propolis
Advanced hive structures feature dedicated compartments that separate honey storage areas from geopropolis (resin) and brood areas. This allows beekeepers to harvest high-quality Sugarbag honey and geopropolis hygienically and non-destructively. Because the core structure of the hive remains intact during collection, the colony recovers faster, leading to more frequent and sustainable harvest cycles.
Understanding the Trade-offs and Pitfalls
Material Quality vs. Insulation
While specialized hives offer many benefits, the choice of materials involves significant trade-offs. Thinner, cheaper materials may reduce initial sourcing costs but often fail to provide the thermal insulation required for colony survival during heatwaves or frosts. Professional distributors must prioritize material density and thermal properties to ensure long-term customer satisfaction and colony health.
Complexity vs. Ease of Use
Increasingly complex hive designs can offer better product separation but may also increase the risk of improper assembly by end-users. Over-engineered hives can sometimes create "dead spaces" where pests like the small hive beetle can hide. It is vital to balance technical sophistication with a design that is intuitive for beekeepers to maintain and clean.
Making the Right Choice for Your Goal
When selecting specialized hives for a commercial portfolio, your choice should align with the specific operational objectives of your clients.
- If your primary focus is rapid market expansion: Prioritize modular, standardized hives produced by precision machinery to ensure consistent quality and ease of colony splitting.
- If your primary focus is high-value product extraction: Invest in specialized designs that feature dedicated honey supers and resin collectors to ensure the highest purity of Sugarbag honey and geopropolis.
- If your primary focus is conservation and rescue services: Select hives that specifically mimic the thermal mass of natural tree hollows to increase the survival rates of relocated wild colonies.
By providing the right hardware, distributors can empower beekeepers to achieve a perfect balance between commercial productivity and the long-term health of these vital pollinators.
Summary Table:
| Key Role | Commercial Benefit | Technical Feature |
|---|---|---|
| Habitat Simulation | Ensures colony survival & stability | Thermal insulation & microenvironment control |
| Standardization | Enables industrial-scale operations | Uniform hive-making machinery & components |
| Modular Design | Facilitates rapid colony propagation | Sectional boxes for easy splitting |
| Precision Harvesting | Increases honey & resin purity | Dedicated honey supers & resin collectors |
Scale Your Beekeeping Business with HONESTBEE
Are you a distributor or commercial apiary looking to dominate the Australian stingless bee market? HONESTBEE is your premier partner for one-stop sourcing. We provide the full spectrum of beekeeping hardware—from specialized hive-making machinery and honey-filling equipment to high-performance hives and essential consumables.
Why partner with us?
- Deep Industry Expertise: Specialized solutions for Meliponini cultivation.
- Rapid Fulfillment: Ultra-fast delivery to keep your supply chain moving.
- Distributor Support: High-margin wholesale offerings and premium trading services tailored to B2B resellers.
Ready to enhance your portfolio with industry-leading equipment? Contact our expert team today to request a quote!
References
- Kit Prendergast. An Evaluation of the Popularity of Australian Native Bee Taxa and State of Knowledge of Native Bee Taxonomy Among the Bee-Interested Public. DOI: 10.3390/insects16111149
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Australian Langstroth Beehive Boxes for Beekeeping Wholesales
- HONESTBEE Professional Hive Top Bee Feeder Feeding Solution
- Wholesales Dadant Size Wooden Bee Hives for Beekeeping
- High-Performance Langstroth Bee Hives for Global Professional Beekeeping
- Langstroth Honey Bee Box Hive Boxes for Different Depths
People Also Ask
- What are the primary advantages of using standardized Langstroth boxes? Scale Your Commercial Beekeeping Operation
- What are the differences between the three standard depths of Langstroth boxes? Choose the Best Size for Your Apiary
- What role do standardized Langstroth boxes play in commercial apiary management and honey bee research? | HONESTBEE Guide
- How many beehive boxes are needed when starting a new hive? A Guide to Proper Hive Setup
- What are the disadvantages of using a combination of deep and medium boxes? Avoid Costly Incompatibility Issues