Moisture content is one of the most important quality controls in commercial honey processing. Excess water allows sugar-tolerant wild yeasts to multiply, causing fermentation, sour or foul flavors, gas formation, container swelling, and—in severe cases—jar breakage. Commercial processors should test every batch with a calibrated honey refractometer before extraction, blending, filling, and distribution.
The practical target is stable, market-ready honey with moisture comfortably below 18%, while honey above 20% presents a serious fermentation risk. A calibrated optical refractometer is the primary testing instrument; a honey hydrometer can provide a secondary or field check when used correctly.
Why Moisture Control Determines Honey Stability
High moisture enables fermentation
Honey naturally contains water, but its high sugar concentration normally prevents most microorganisms from growing. When moisture rises, the sugar solution becomes less concentrated and osmophilic yeasts, including species associated with Zygosaccharomyces and Saccharomyces, can become active.
Fermentation produces carbon dioxide and alcohols, resulting in off-flavors, off-gassing, foaming, and pressure inside sealed containers.
Moisture affects shelf life and customer acceptance
Honey exceeding approximately 18% to 19% moisture has an increasing risk of fermentation, while honey above 20% is at severe risk of spoilage under typical storage conditions. Honey below 17.1% is generally considered highly resistant to fermentation, even when yeast is present.
These figures should be treated as practical risk levels rather than a substitute for applicable regulations, product specifications, or validated shelf-life testing.
Moisture influences processing performance
Water content affects honey’s viscosity, pumpability, filtration behavior, and filling consistency. A batch with excessive moisture may behave differently in pumps and filling machines, leading to inconsistent dispensing and more difficult process control.
Moisture is not the only factor affecting flow. The glucose-to-fructose ratio also influences crystallization, so processors should consider both composition and moisture when setting equipment parameters.
Which Equipment Should Be Used?
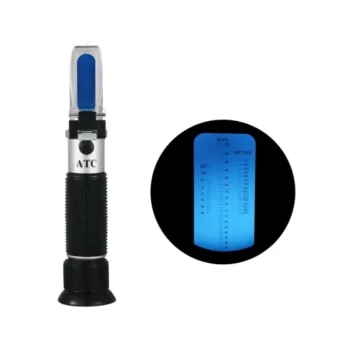
Calibrated honey refractometer
A honey refractometer is the primary instrument for commercial moisture testing. It measures the honey’s refractive index and converts that reading into an estimated moisture percentage using a honey-specific scale.
Optical refractometers are fast, require only a small sample, and are well suited to receiving inspection, process checks, and final approval before bottling.
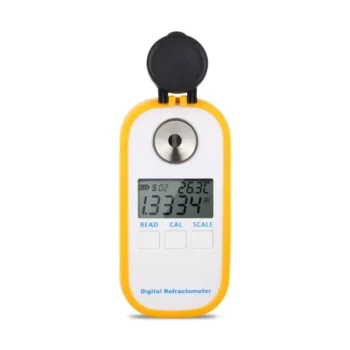
Digital refractometer
A digital honey refractometer is useful where multiple operators, high testing frequency, or traceable quality records are important. It reduces interpretation errors associated with reading an optical scale and can improve consistency across production shifts.
The instrument must still be designed or configured for honey. A general-purpose refractometer may not provide reliable results if its scale or temperature compensation is unsuitable for honey.
Honey hydrometer
A specialized honey hydrometer can be used as a secondary method, particularly for basic field or receiving checks. It estimates specific gravity, which correlates with water content.
Hydrometers require a sufficiently large, bubble-free sample and careful temperature control. They are generally less convenient than refractometers for routine commercial testing, especially when samples are viscous or crystallized.
How to Test Honey Reliably
Calibrate before measuring
Calibration is essential because an uncalibrated refractometer can create false confidence in a batch’s stability. Follow the instrument manufacturer’s procedure, typically using the specified calibration fluid or distilled water.
Calibration should be checked regularly and whenever the instrument is exposed to unusual temperatures, contamination, or heavy use.
Use a representative sample
Honey can vary within a tank, drum, or harvest lot. Mix or circulate the batch appropriately, then collect a representative sample rather than testing only the surface or the first material discharged.
Avoid air bubbles, wax particles, foam, and crystallized portions that do not represent the full batch. Clean the prism between samples to prevent carryover between lots.
Control sample temperature
Temperature affects refractive-index readings and honey viscosity. Allow the sample and instrument to reach the operating temperature specified by the equipment manufacturer, and use automatic temperature compensation only within its stated range.
Do not rely on an apparently precise reading if the sample is unusually hot, cold, crystallized, or poorly mixed.
Test at critical control points
Moisture should be checked:
- At receiving, before purchasing or accepting a honey lot.
- After harvesting or drying.
- Before extraction, filtration, and blending.
- Before filling and final packaging.
- During storage or investigation of swollen, leaking, or fermenting containers.
Maintaining records by lot provides an objective basis for release decisions, supplier evaluation, pricing, and customer claims.
How Commercial Operations Manage Excess Moisture
Reduce moisture before extraction
Honey is hygroscopic, meaning it readily absorbs moisture from humid air. Climate-controlled rooms and dehumidification can help reduce moisture in honey held in combs before extraction.
Warm, dry air may be circulated over combs, but process conditions must be controlled to avoid unnecessary heating or quality loss.
Use controlled heating when appropriate
Double-jacketed tanks or other controlled heating systems may be used to improve flow and remove some excess moisture. Heating can also reduce yeast activity, but it is not a replacement for moisture control.
Excessive or prolonged heat can damage natural flavor and enzymes and increase hydroxymethylfurfural (HMF) formation. Any heating program should therefore be validated against the product specification and regulatory requirements.
Protect honey from reabsorption
Drying a batch is not enough if the product is later exposed to humid air. Covered tanks, short transfer times, dehumidified processing areas, and properly sealed packaging help prevent moisture from returning before filling.
Understanding the Trade-offs
A low reading does not guarantee perfect product quality
Moisture is a major stability indicator, but it does not measure every quality attribute. Yeast load, storage temperature, contamination, adulteration, and handling conditions can also affect shelf life.
Moisture testing should therefore be part of a broader quality program rather than the sole release test.
Heating can control yeast but may reduce quality
Heating may help destroy yeast cells and improve processability, but it can alter aroma, flavor, enzymes, and HMF levels. The best approach is usually to control moisture early rather than depend on aggressive heating after the honey is already at risk.
“Below 22%” is not a universal commercial target
Some reference material cites 22% as a threshold for inhibiting yeast growth, but this is not a sufficiently conservative general target for commercial honey. Many market standards and commercial specifications use 20% as the maximum for ordinary honey, with fermentation risk rising earlier depending on yeast count and storage conditions.
Always confirm the applicable legal standard and buyer specification for the destination market, but do not treat 22% as a broadly safe release limit.
Equipment quality affects purchasing decisions
For distributors, wholesalers, and processors, the instrument itself is part of the quality system. A low-cost device with an unsuitable scale, poor calibration stability, or no service support can create costly acceptance and rejection errors.
Reliable sourcing should include the instrument, calibration materials, operating guidance, replacement parts, and responsive technical support.
Making the Right Choice for Your Goal
Select the testing method and supporting controls according to how the honey will be purchased, processed, and sold.
- If your primary focus is rapid batch release: Use a calibrated digital honey refractometer at receiving, before filling, and during final quality approval.
- If your primary focus is field or small-lot testing: Use a portable optical honey refractometer with proper calibration and temperature control.
- If your primary focus is secondary verification: Use a specialized honey hydrometer, while recognizing its greater sample-volume and handling requirements.
- If your primary focus is shelf stability: Set a conservative moisture specification below the relevant market limit and combine refractometer results with sanitation, yeast-risk, and storage controls.
- If your primary focus is commercial sourcing and resale: Choose suppliers that can provide calibrated equipment, documentation, technical assistance, and fast fulfillment across the full testing and processing workflow.
With accurate moisture data and disciplined process control, commercial honey operators can protect stability, reduce waste, and release more consistent product with confidence.
Summary Table:
| Equipment | Use Case | Advantages | Limitations |
|---|---|---|---|
| Optical Honey Refractometer | Quick receiving, process, and final checks | Fast, small sample, honey-specific scale | Manual reading errors; requires calibration and temperature control |
| Digital Honey Refractometer | High-frequency testing, multi-operator, traceable records | Reduced interpretation errors, consistency, data logging | Higher cost; must be configured for honey |
| Honey Hydrometer | Secondary field or receiving checks | Simple principle, no power needed | Requires large bubble-free sample, careful temperature control, less convenient for viscous honey |
Ensure your honey's stability and market quality with professional testing equipment. At HONESTBEE, we supply calibrated optical and digital honey refractometers plus hydrometers, along with full-spectrum beekeeping tools and processing machinery. As your one-stop wholesale partner, we offer rapid response, dedicated service, and ultra-fast fulfillment for distributors, wholesalers, and commercial apiaries. Need reliable supply and expert guidance? Contact us today to discuss your requirements and secure your honey quality.
Related Products
- Digital Honey Refractometer for Precision Measurement of Optimal Honey Quality
- Precision Honey Refractometer Instrument for Quality Assessment
- High Quality Honey Dehumidifier Dryer Thickening Machine for Beekeeping
- Honey Concentrating and Filtering Dehumidifier Machine 2T Capacity for Honey
- 0.5T Capacity Honey Dehumidifier Dryer with Vacuum Heating and Thickening Filtering Machine
People Also Ask
- What role do high-precision refractometers play in determining the maturity and quality of honey? Ensure Honey Purity.
- Do the color and viscosity of honey affect its refractometer reading? Mastering Moisture Measurement Accuracy
- What is the best way to store a honey refractometer? Preserve Accuracy and Extend Its Lifespan
- What is a honey refractometer? The Essential Tool for Perfect Honey Quality
- How is the reading taken from a honey refractometer? A Guide to Accurate Moisture Measurement