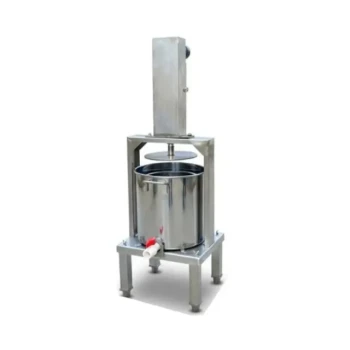
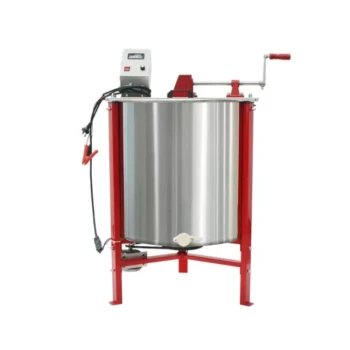
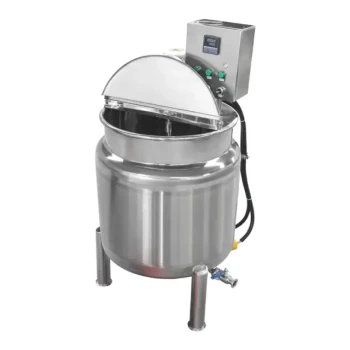
Professional honey harvesting and filling equipment is the critical infrastructure required to scale from local apiaries to global commercial distribution.
These systems provide the precision needed to preserve the biological integrity of honey while maximizing output efficiency. By utilizing centrifugal extraction to save wax combs and automated dosing to ensure legal net weights, professional machinery transforms a raw natural resource into a standardized, high-margin commodity.
High-yield honey production depends on equipment that balances high-speed output with the delicate handling of heat-sensitive nutrients. For distributors and wholesalers, this technology ensures a consistent, contaminant-free supply chain that meets the rigorous safety and quality standards of the international market.
Maximizing Apiary Efficiency and Colony Health
The Impact of Centrifugal Extraction
Professional centrifugal extractors allow for the separation of honey while keeping the wax combs intact. This significantly reduces the energy the bee colony must spend on rebuilding combs, allowing them to focus entirely on honey production.
Accelerating the Harvest Cycle
By preserving the comb structure, beekeepers can return frames to the hives almost immediately. This leads to faster turnaround times and higher total yields over a single season, providing a more reliable volume for wholesalers.
Reducing Colony Disturbance
Professional-grade machinery is designed to operate with minimal vibration and noise. This keeps the colony's stress levels low, ensuring long-term apiary health and consistent output for commercial-scale operations.
Preserving Product Integrity and Biological Activity
Advanced Temperature and HMF Control
Honey is a heat-sensitive substance; excessive warmth during processing can increase Hydroxymethylfurfural (HMF) levels, which degrades quality. Professional equipment uses precise temperature control to maintain the honey's natural nutritional profile and shelf stability.
Physical Filtration Without Nutrient Loss
Commercial filtration systems use physical means to remove impurities like bee parts or large wax particles. This ensures the honey remains pure while retaining its natural biological activity and enzymes, which are critical for premium "raw" honey labeling.
Preventing Moisture Absorption
Honey is hygroscopic, meaning it absorbs moisture from the air, which can lead to fermentation and spoilage. Professional filling lines utilize closed-pipe designs to minimize air contact, preserving the honey's specific viscosity and preventing loss of stock.
Ensuring Regulatory Compliance and Marketability
Precision Dosing and Net Weight Accuracy
For B2B resellers, weight discrepancies are a major legal and financial risk. Automated filling machines utilize precise volumetric or weight-based dosing to ensure every jar meets standardized net weight requirements for retail.
Maintaining Hygiene with Anti-Drip Technology
Modern filling heads are equipped with anti-drip mechanisms that keep the production environment clean. This prevents secondary contamination and ensures that the finished product meets the strict hygiene standards of modern food safety regulations.
Standardizing for High-End Markets
To compete in high-end dietary supplement or organic markets, product consistency is non-negotiable. Professional equipment ensures that honey from various regions can be processed to a uniform specification, increasing consumer confidence and brand value.
Understanding the Trade-offs
High Initial Capital Expenditure
The primary hurdle for many operations is the high upfront cost of industrial-grade machinery. However, for distributors, this investment is offset by reduced material loss and the ability to fulfill much larger orders.
Technical Expertise and Maintenance
Professional systems require specialized knowledge to operate and maintain, particularly when handling high-viscosity fluids. Partnering with a supplier that offers deep industry expertise and rapid response times is essential to minimize downtime.
Infrastructure and Space Requirements
Automated lines require significant facility space and power infrastructure compared to manual methods. Producers must balance the efficiency gains of automation against the increased overhead of a larger production footprint.
Making the Right Choice for Your Goal
As a distributor or wholesaler, selecting the right equipment partner is about more than just hardware; it is about securing your supply chain's reliability.
- If your primary focus is rapid market entry: Seek a partner offering one-stop sourcing of comprehensive, full-spectrum product portfolios to simplify your procurement.
- If your primary focus is premium brand positioning: Prioritize equipment that features advanced HMF control and closed-system filling to guarantee the highest nutritional integrity.
- If your primary focus is high-volume fulfillment: Invest in automated lines with ultra-fast delivery and high-precision dosing to maximize throughput and minimize waste.
- If your primary focus is organic certification: Ensure your equipment utilizes fully enclosed, easy-to-sanitize environments to meet strict traceability and safety requirements.
Choosing the right professional equipment is the definitive step toward transforming a local apiary into a powerhouse of high-yield commercial production.
Summary Table:
| Feature | Commercial Benefit | Impact on Profitability |
|---|---|---|
| Centrifugal Extraction | Preserves wax combs for faster reuse | Increases annual yield per colony |
| Precision Dosing | Ensures legal net weight accuracy | Eliminates product waste and legal risks |
| HMF Temperature Control | Maintains biological integrity & enzymes | Commands premium pricing for high-quality honey |
| Closed-Pipe Filling | Prevents moisture absorption & oxidation | Extends shelf life and reduces spoilage |
| Anti-Drip Technology | Maintains sterile, clean environment | Lowers labor costs and contamination risk |
Scale Your Honey Distribution with HONESTBEE
Are you a distributor, wholesaler, or B2B reseller looking to secure a reliable, high-performance supply chain? HONESTBEE is your premier one-stop sourcing partner for the full spectrum of commercial beekeeping technology.
From industrial honey-filling machines and hive-making hardware to professional-grade consumables and cultural merchandise, we provide the tools you need to maximize profit margins and operational efficiency.
Why Partner with HONESTBEE?
- Comprehensive Portfolio: Full-spectrum machinery and equipment for every stage of production.
- Deep Industry Expertise: Professional guidance tailored to large-scale apiaries.
- Rapid Fulfillment: Ultra-fast delivery and dedicated support to keep your orders moving.
- OEM/ODM Support: Customized solutions to strengthen your brand’s market position.
Ready to enhance your competitive edge? Contact our team today to discuss wholesale opportunities!
References
- Xinying Qu, Xiao Chen. Investigation and Study on the Biology and Morphology of Apis florea and Apis dorsata in Southern China. DOI: 10.3390/life15030341
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
- Automatic Honey Filling and Filtering Machine for Beekeeping Bottle Filling
- Economy Small Honey Filling Machine Honey Bottle Filler Packaging Machine
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Commercial Rotary Honey Filling Machine for Production
People Also Ask
- What are the common types of bottling machines used for honey? Choosing the Right Solution for Your Apiary
- How do high-precision honey filling machines ensure quality? Optimize Your Commercial Production with HONESTBEE
- What quality control role does professional honey filling equipment perform? Ensure Consistency and Product Stability
- How do honey filling and processing machines aid native bee product conservation? Boost Value with HONESTBEE Technology
- What is a key feature of the new generation of the honey filling machine? The Advanced Electronic Control Unit