Professional honey processing facilities are the engine of market competitiveness, transforming raw agricultural goods into standardized, high-value commodities that meet rigorous global standards. By centralizing advanced filtration, moisture control, and automated packaging, these facilities provide the consistency and regulatory compliance necessary for distributors to access premium retail markets and international export channels.
Core Takeaway: A professional processing facility mitigates the risks of quality variance and contamination, enabling B2B resellers to offer a stable, certified, and shelf-stable product that commands higher margins in a crowded global marketplace.
Elevating Product Standards for Global Trade
Achieving Regulatory and Health Certifications
Professional facilities provide the controlled, hygienic environments required to secure government health certifications and international regulatory approvals. Without these formal credentials, honey products are often restricted from entering premium markets or crossing international borders.
Standardizing Physical and Sensory Quality
Specialized equipment like centrifugal extractors and high-precision filters ensures that every batch meets uniform standards for clarity, color, and fluidity. This industrial standardization is critical for building consumer trust, as roughly 62.3 percent of consumers specifically prefer the visual purity of processed honey over raw, unrefined alternatives.
Ensuring Biochemical Stability
Advanced processing includes precise moisture control and dehydration to prevent the natural fermentation and spoilage of honey. By stabilizing the product’s chemical indicators, facilities ensure that the honey remains shelf-stable during long-term storage and the rigors of international transportation.
Strengthening the B2B Supply Chain
Enabling One-Stop Sourcing Capabilities
A professional facility acts as a centralized hub, offering a comprehensive product portfolio that ranges from raw bulk supply to retail-ready bottled products. For wholesalers, this eliminates the need to manage multiple vendors, streamlining the procurement process through a single, expert partner.
Rapid Response and Efficient Fulfillment
Automated processing and bottling lines allow for ultra-fast delivery and order fulfillment, even at high volumes. This mechanical efficiency translates into shorter lead times, allowing distributors to respond quickly to market fluctuations and urgent restocking needs.
Leveraging Deep Industry Expertise
Beyond simple processing, these facilities house professional technical knowledge regarding honey varieties and global food safety trends. This expertise helps B2B partners navigate complex import/export requirements, reducing the risk of costly shipment rejections or compliance failures.
Understanding the Trade-offs
Balancing Processing with Nutritional Integrity
While intensive processing ensures purity and clarity, excessive heat can damage heat-sensitive enzymes and delicate flavor profiles. High-tier facilities must utilize controlled heating mechanisms to remove impurities without compromising the natural bioactive components that drive the "premium" health-food narrative.
The Investment Gap in Small-Scale Production
The transition from hobbyist beekeeping to commercial-grade processing requires significant capital investment in specialized machinery. While this raises the barrier to entry, it is the only viable path to achieving the standardized physicochemical indicators required for formal retail distribution.
How to Apply This to Your Business Strategy
Strategic Alignment for Market Success
- If your primary focus is entering high-end retail: Prioritize facilities that hold recognized international quality certifications and offer superior clarity through high-precision filtration.
- If your primary focus is supply chain efficiency: Partner with a facility that offers integrated bottling and automated fulfillment to ensure rapid response times and consistent stock availability.
- If your primary focus is preserving nutritional value: Seek out processing partners who utilize low-heat dehydration and "gentle" filtration techniques to maintain the honey's natural biochemical profile.
Investing in professionally processed honey is the most effective way to ensure long-term profitability, product safety, and a dominant position in the global honey trade.
Summary Table:
| Key Feature | Functional Benefit | Market Impact |
|---|---|---|
| Moisture Control | Prevents fermentation and spoilage | Extended shelf life and global export stability |
| Advanced Filtration | Removes impurities while ensuring clarity | Higher consumer trust and premium retail pricing |
| Automated Bottling | Rapid fulfillment and high-volume output | Shorter lead times and reliable supply for wholesalers |
| Regulatory Compliance | Meets international food safety standards | Access to restricted high-end international markets |
Scale Your Honey Business with HONESTBEE
Maximize your market potential with HONESTBEE, your premier partner for one-stop beekeeping and processing solutions. We cater specifically to commercial apiaries and B2B distributors, offering a comprehensive wholesale portfolio that includes:
- Advanced Machinery: Specialized honey-filling lines and professional hive-making machines.
- Full-Spectrum Equipment: Industrial extractors, filtration systems, and essential consumables.
- B2B Support: Rapid response times, deep industry expertise, and reliable fulfillment to protect your margins.
Whether you are looking to upgrade your facility's efficiency or expand your product range with premium hardware, HONESTBEE delivers the quality and speed you need to stay ahead.
Contact our experts today to optimize your supply chain!
References
- R. S. S. Silva, Denise de Lima Belisario. Perfil socioeconômico e tecnológico dos apicultores do norte de Minas. DOI: 10.55905/revconv.17n.9-410
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
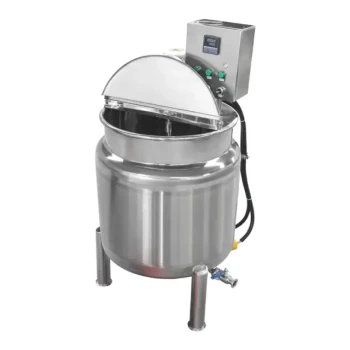
- Double Wall Honey Heating Stirring Homogenizer Mixing Machine with Various Capacity
- Honey Concentrating and Filtering Dehumidifier Machine 2T Capacity for Honey
- Electric Double Wall Honey Filtering Machine Purifier Equipment for Honey Processing Plant
- 0.5T Capacity Honey Dehumidifier Dryer with Vacuum Heating and Thickening Filtering Machine
- Heavy Duty Stainless Steel Honey Processing Machine Decrystallizing Tank
People Also Ask
- What impact do homogenizers or oscillating equipment have on honey microbial detection? Ensure Testing Accuracy
- Why is thorough mechanical stirring and homogenization emphasized in honey processing? Ensure Sample Accuracy
- How do heating equipment and homogenizers liquefy crystallized honey? Expert Guide to Professional Honey Processing
- How does the honey mixer handle different types of honey? Master Viscosity for Perfect Blends
- What are the main components of the honey mixer? Engineered for Gentle, Efficient Honey Processing