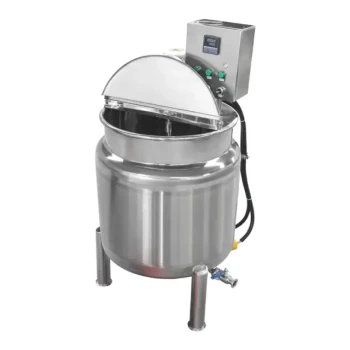
Automated honey filling technology is the cornerstone of modern food safety, utilizing sealed piping systems and high-precision volumetric pumps to create a sterile, contact-free path from storage to the final container. By eliminating manual handling and external air exposure, these machines ensure that honey products remain free from secondary contamination and maintain their natural biological integrity.
Industrial automatic honey filling machines enhance food safety by replacing manual processes with enclosed, sterile systems that prevent microbial ingress and cross-contamination. This technology ensures every unit meets strict international hygiene standards and consistent weight requirements, protecting both the product's quality and the distributor's reputation.
Eliminating Manual Contamination Risks
The Sterile Path from Tank to Bottle
The primary safety benefit of automation is the removal of human contact from the packaging cycle. Manual filling exposes honey to skin contact, respiratory droplets, and hair, all of which are significant vectors for bacteria.
Automated systems utilize sealed piping and closed-loop designs to move honey directly from bulk storage into bottles. This isolation ensures the product remains as pure as it was when it left the extraction facility.
High-Precision Volumetric Pump Control
Precision is not just about profit; it is about hygienic consistency. Automated volumetric pumps deliver the exact required amount of honey without the spills or "over-filling" common in manual operations.
Reducing drips and spills prevents honey residue from accumulating on the outside of the bottle or the conveyor. This keeps the entire production environment cleaner and prevents the growth of mold or attraction of pests.
Protecting the Biological Integrity of Honey
Preventing Moisture Absorption and Fermentation
Honey is hygroscopic, meaning it naturally absorbs moisture from the air. High moisture content can lead to unwanted fermentation and the growth of yeast, which ruins the product.
Industrial machines utilize enclosed filling heads that minimize the time the honey is exposed to ambient air. By shortening the exposure window, these machines preserve the honey’s low moisture levels and shelf stability.
Preserving Natural Enzymes and Aromas
Honey contains delicate natural enzymes like amylase and catalase, as well as volatile aromatic compounds. Exposure to oxygen and fluctuating environments during slow manual filling can cause these elements to degrade.
Automated systems isolate the honey from air contact, ensuring that the natural flavor profile and health benefits remain intact for the end consumer. This level of quality control is essential for distributors targeting the premium or medicinal honey markets.
Maintaining Batch Purity and Compliance
Advanced Clean-In-Place (CIP) Systems
For wholesalers managing various honey types, preventing cross-contamination is a critical logistical challenge. Industrial machines are equipped with Clean-In-Place (CIP) technology, which allows for thorough cleaning without dismantling the machine.
These systems use high-efficiency rinsing to remove pesticide or metal residues from previous batches. This ensures that every shipment meets the stringent safety and hygiene standards required for international trade.
Meeting International Weight and Labeling Standards
Food safety regulations often include strict "Net Weight" requirements to prevent consumer fraud. Automated metering ensures that every bottle is standardized and compliant with global trade laws.
For B2B resellers, this consistency reduces the risk of regulatory fines or shipment rejections at customs. It provides a reliable, "plug-and-play" inventory that is ready for immediate distribution.
Understanding the Trade-offs
Initial Capital Investment vs. Long-term Gains
Transitioning to fully automated filling requires a significant upfront investment compared to semi-automatic or manual setups. However, the reduction in material loss (waste) and labor costs typically offsets this over time.
Technical Expertise and Maintenance Requirements
These machines are sophisticated instruments that require regular calibration and specialized maintenance. A distributor must ensure their sourcing partner provides adequate technical support to prevent downtime.
Flexibility Limitations
While high-speed machines are incredibly efficient, they may require specific changeover parts for different bottle shapes or honey viscosities. Large-scale automation is best suited for standardized product lines rather than highly diverse, small-batch artisanal runs.
Making the Right Choice for Your Distribution Goals
As a distributor or wholesaler, your choice of equipment—or your choice of a manufacturing partner—directly impacts your supply chain reliability and brand trust.
- If your primary focus is international export: Prioritize machines with integrated CIP systems and enclosed filling zones to ensure compliance with strict foreign food safety audits.
- If your primary focus is high-volume retail fulfillment: Look for high-speed industrial-grade pumps that offer "drip-proof" technology to maintain a clean, retail-ready outer package.
- If your primary focus is premium or medicinal honey: Invest in systems that emphasize "air-free" filling to protect the delicate enzyme activities and natural antioxidants of the honey.
By integrating automated filling technology into your production line, you ensure a safe, standardized, and high-quality product that meets the rigorous demands of the global marketplace.
Summary Table:
| Safety Feature | Technical Mechanism | Impact on Honey Quality |
|---|---|---|
| Manual Removal | Sealed piping & closed-loop designs | Eliminates human-borne bacteria & contaminants. |
| Precision Dosing | High-precision volumetric pumps | Prevents spills, mold growth, and pest attraction. |
| Atmospheric Shield | Enclosed filling heads | Prevents fermentation by blocking moisture absorption. |
| Integrity Protection | Reduced air exposure | Preserves delicate natural enzymes and volatile aromas. |
| Purity Control | Clean-In-Place (CIP) technology | Eliminates cross-contamination and pesticide residues. |
Partner with HONESTBEE for Professional Packaging Excellence
Elevate your production standards with HONESTBEE, your premier partner for one-stop sourcing in the beekeeping industry. We cater specifically to commercial apiaries, distributors, and B2B resellers, providing a comprehensive full-spectrum product portfolio—from high-precision honey-filling machines and hive-making hardware to essential consumables and cultural merchandise.
Why Choose HONESTBEE?
- Deep Industry Expertise: Specialized solutions tailored to global food safety and trade standards.
- Operational Efficiency: Ultra-fast delivery and rapid response times to keep your supply chain moving.
- Premium Support: Dedicated customer service focused on maximizing your profit margins and operational reliability.
Ready to secure your product's purity and scale your distribution? Contact our expert team today to explore our wholesale offerings and OEM/ODM support!
References
- Rüksane Çelik, Ersin Karakaya. The Opinions of Diyarbakır Provincial Center Consumers on the Quality of Honey on the Market and the Factors Affecting Their Honey Consumption Preferences. DOI: 10.30910/turkjans.1452609
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Precision Durable Efficient HONESTBEE Rotary Honey Filling Machine
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Automatic Honey Filling and Filtering Machine for Beekeeping Bottle Filling
- Precision Automated Packaging Turntable Honey Spoon Filling Sealing Packing Machine
- Automatic Single-Dose Snap & Squeeze Honey Sachets Packing Machine
People Also Ask
- What quality control role does professional honey filling equipment perform? Ensure Consistency and Product Stability
- How do honey filling and processing machines aid native bee product conservation? Boost Value with HONESTBEE Technology
- How do high-precision honey filling machines ensure quality? Optimize Your Commercial Production with HONESTBEE
- How do honey filling machines work? Achieve Precision & Speed for Your Apiary
- What are the common types of bottling machines used for honey? Choosing the Right Solution for Your Apiary