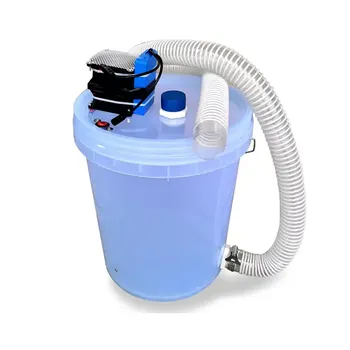
The primary function of a portable vacuum honey harvester is to extract honey from stingless bee hives using controlled negative pressure. This mechanized process allows for the efficient, hygienic, and non-destructive removal of honey directly from delicate cerumen pots, ensuring the highest standards of purity for the final product.
Core Takeaway: By replacing manual squeezing with negative pressure technology, these harvesters preserve the integrity of the hive and eliminate external contaminants, making them an essential tool for suppliers focusing on premium, high-purity stingless bee honey.
Maximizing Purity and Efficiency in Honey Collection
The Mechanics of Negative Pressure
A portable vacuum honey harvester operates by creating negative pressure within a closed collection system. This suction draws the honey directly from the small, intricate honey pots of stingless bees without requiring the operator to break or crush the hive structure.
This method is particularly critical for stingless bee species like Heterotrigona itama, which produce smaller volumes of honey in complex architectural environments. By using a mechanized suction pump, producers can significantly increase collection speed compared to traditional manual methods.
Eliminating Environmental Contaminants
Traditional harvesting often involves manual squeezing or "pressing," which exposes the raw honey to air, debris, and human contact. The vacuum harvester provides a closed extraction environment that minimizes the risk of microbial contamination.
For B2B distributors, this translates to a more stable product with a longer shelf life and higher market value. The uninterrupted hygiene chain ensures that the honey retains its original nutritional profile and natural enzymes.
Protecting Hive Infrastructure and Colony Health
Non-Destructive Extraction Technology
Stingless bees store their honey in delicate wax pots rather than the sturdy hexagonal combs found in honeybee hives. The primary function of the vacuum tool is to protect these fragile structures from physical damage during the harvest.
Because the suction is localized and controllable, the colony suffers less stress and can recover more quickly. This sustainable approach ensures the long-term productivity of the hive, which is a vital consideration for wholesalers securing long-term supply contracts.
Specialized Application for Intricate Hives
The intricate hive architecture of stingless bees makes manual extraction labor-intensive and wasteful. The portable vacuum device uses specialized suction lines to reach into small crevices that would otherwise be inaccessible.
This level of precision engineering allows for maximum yield per hive. By optimizing the volume collected from each colony, producers can maintain a more consistent and reliable inventory for their global partners.
Understanding the Trade-offs and Implementation Risks
Suction Calibration and Hive Stress
While negative pressure is efficient, incorrect calibration can lead to "over-suction," which may inadvertently harm the bees or collapse the internal pots. Professional-grade equipment must feature adjustable pressure settings to account for different species and honey viscosities.
Technical expertise is required to ensure the vacuum level is high enough to move the viscous honey but low enough to maintain hive integrity. Distributors should prioritize sourcing equipment that offers precise control to minimize these risks.
Maintenance and Sterilization Requirements
The very benefit of a closed system—hygiene—is dependent on rigorous cleaning protocols. If the internal lines of the vacuum harvester are not properly sterilized between uses, they can become breeding grounds for bacteria.
Wholesalers must ensure their suppliers adhere to strict maintenance schedules. A failure in equipment hygiene can compromise an entire batch of honey, leading to significant financial losses and damage to brand reputation.
Making the Right Choice for Your Business Goal
When sourcing honey harvesting technology for your portfolio, align your equipment selection with your specific operational objectives. Our deep professional industry expertise and full-spectrum product portfolio are designed to meet these diverse needs.
- If your primary focus is maximizing product purity: Invest in high-end vacuum systems with food-grade, antimicrobial suction lines that ensure a completely closed extraction loop.
- If your primary focus is scaling production volume: Prioritize portable electric models with high-capacity batteries and rapid-fill collection containers to decrease downtime between hives.
- If your primary focus is hive sustainability and long-term yield: Select devices with precision-controlled negative pressure gauges to prevent structural damage to delicate stingless bee colonies.
The adoption of portable vacuum technology is the definitive step toward professionalizing the stingless bee honey supply chain and ensuring premium quality for the global market.
Summary Table:
| Key Feature | Primary Function | Business Benefit |
|---|---|---|
| Negative Pressure | Mechanized extraction from delicate pots | Higher efficiency & reduced labor costs |
| Closed System | Eliminates exposure to air and debris | Superior purity & longer shelf life |
| Non-Destructive Tech | Protects fragile cerumen/wax structures | Sustainable hive health & long-term yield |
| Precision Suction | Accesses intricate, small hive crevices | Maximized honey volume per colony |
Elevate Your Wholesale Supply Chain with HONESTBEE
Are you looking to scale your stingless bee honey production with professional-grade equipment? HONESTBEE is your premier one-stop sourcing partner, catering specifically to commercial apiaries and B2B distributors.
We provide a comprehensive full-spectrum product portfolio, including specialized vacuum harvesters, honey-filling machines, and essential industry consumables. Partnering with us means gaining access to:
- Deep Industry Expertise: Equipment tailored for high-purity honey production.
- Premium Trading Services: OEM/ODM support to strengthen your brand identity.
- Efficient Fulfillment: Ultra-fast delivery and rapid response times to keep your inventory moving.
Boost your profit margins and ensure supply reliability with the industry experts. Contact our wholesale team today to discuss your bulk equipment needs!
References
- I. Gede Pasek Mangku, Mia Bella R. Fresnido. Vacuum evaporation optimization of Bali local honey for quality enhancement. DOI: 10.26656/fr.2017.8(6).018
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Honey Concentrating Vacuum Heating Thickening Machine Dehumidifier for Honey
- 0.5T Capacity Honey Dehumidifier Dryer with Vacuum Heating and Thickening Filtering Machine
- Stainless Steel Pivoting Honey Uncapping Fork with Plastic Handle
- All-Stainless Steel Pivoting Honey Uncapping Fork for Beekeeping
- HONESTBEE 6 Frame Self Reversing Electric Honey Extractor for Beekeeping
People Also Ask
- What are the advantages of using a honey concentrator machine in apiculture? Boost Quality & Shelf Life
- What should be observed during the feeding process of the honey concentrator? Master Honey Processing Efficiency
- What are the benefits of a honey concentrator? Elevate Your Honey Quality and Market Value
- What electrical safety precaution is necessary when operating the honey concentrating equipment? Essential Grounding Tips
- What are the main functions of the honey concentrating equipment? Essential Machinery for Commercial Quality