Stringent quality standards directly shape both how commercial honey is processed and which equipment businesses can responsibly purchase. Regulatory requirements for purity, pesticide residues, moisture, HMF, hygiene, labeling, and adulteration prevention mean that commercial operators need food-grade, sanitary, and precisely controlled systems. The right equipment must protect the honey’s composition while also producing consistent, traceable, and market-ready packs for wholesale, retail, and international distribution.
Honey equipment is a compliance investment, not merely a production upgrade. Every stage, from extraction and filtration to heating, storage, filling, and sealing, must reduce contamination and adulteration risks without damaging heat-sensitive quality characteristics.
Why Regulations Change Commercial Honey Processing
Purity Must Be Demonstrable
Commercial honey must satisfy defined chemical and physical parameters rather than rely solely on visual inspection or supplier claims. Testing may assess moisture, sucrose and other sugar levels, HMF, acidity, pollen content, pesticide residues, and evidence of adulteration.
Standards differ by country, grade, and certification scheme. Requirements associated with systems such as FSSAI, AGMARK, BIS, international food codes, or private buyer specifications should therefore be verified for the target market before equipment is selected.
Adulteration Prevention Requires Process Control
Adulteration can involve the addition of sugar syrups, excess water, undeclared ingredients, or lower-grade honey. A controlled processing environment cannot replace laboratory testing, but it can prevent avoidable quality variation and reduce opportunities for uncontrolled handling.
Commercial operators should begin with traceable honey from managed apiaries and maintain records through extraction, processing, blending, filling, and shipment. Equipment that supports repeatable settings and batch documentation strengthens this control system.
Market Access Depends on More Than the Honey Itself
Distributors and wholesalers often need products that meet documented food-safety, packaging, labeling, and certification requirements. A producer may have acceptable raw honey but still lose access to formal retail or export channels because the processing room, packaging system, or records are inadequate.
For B2B buyers, a supplier’s ability to provide compliant equipment, spare parts, technical support, and rapid fulfillment can be as important as the machine’s nominal capacity.
How Standards Influence Equipment Selection
Food-Grade Construction Is Fundamental
Honey-contact surfaces should be manufactured from hygienic, food-grade materials, commonly sanitary stainless steel. Equipment should be designed for effective cleaning, with minimal dead zones, accessible contact areas, and components that do not introduce contaminants or unwanted flavors.
Storage tanks, settling tanks, extractors, filters, pumps, and filling systems must be evaluated as one hygienic process line. A compliant filling machine cannot compensate for contamination introduced by an unsuitable upstream tank or transfer system.
Temperature Control Protects Quality
Heat can reduce sensory and functional quality and may increase HMF when honey is exposed to excessive temperatures or held hot for too long. This is particularly important for premium, therapeutic, or standardized honeys where natural enzymes, volatile aromas, and other bioactive characteristics are commercially significant.
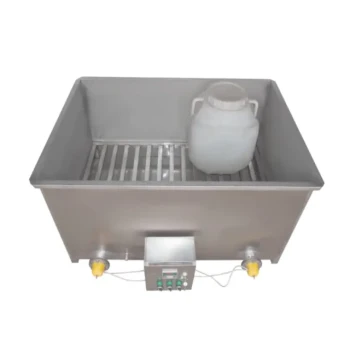
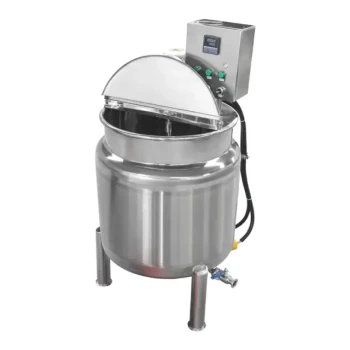
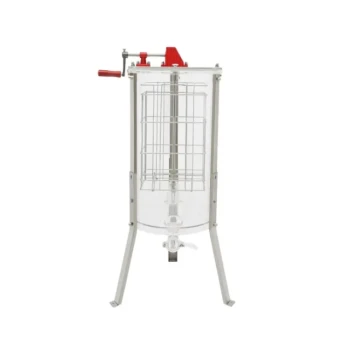
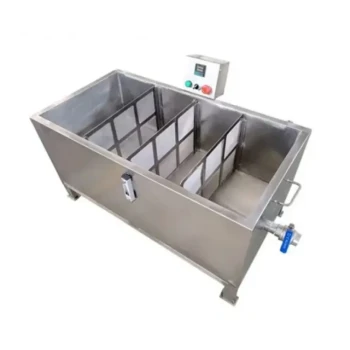
Commercial systems should therefore provide controlled, measurable, and repeatable heating rather than uncontrolled high-temperature exposure. Temperature-controlled extractors, warming units, straining systems, and holding tanks help operators liquefy honey while limiting unnecessary thermal stress.
Filtration Must Match the Product Specification
Filtration removes wax particles, bee parts, and other physical impurities, improving appearance and consistency. However, filtration intensity must be appropriate for the product and its labeling or certification requirements.
A system designed for coarse impurity removal may be suitable for conventional honey, while premium or specialty products may require a carefully specified filtration approach that preserves relevant natural characteristics. Equipment should be selected according to the buyer’s product standard, not simply the finest available filter rating.
Moisture Control Limits Spoilage Risk
Excess moisture can increase the risk of fermentation and spoilage. Commercial processing may therefore require moisture measurement, controlled storage, and suitable dehumidification or handling practices, depending on the incoming honey and applicable specification.
The references identify premium limits around 20% moisture and broader commercial expectations below 21%, but these figures are not universal substitutes for the governing market standard. Operators should use calibrated testing equipment and confirm the exact limit for the intended grade and jurisdiction.
Filling and Sealing Need Precision
Honey is viscous and can be difficult to fill consistently without suitable controls. Automated filling machines improve volume accuracy, reduce manual handling, and support repeatable production for jars, bottles, sachets, or larger wholesale containers.
Sanitary filling and sealing also protect the product from ambient humidity, dust, and microbial contamination. For distributors, consistent fill levels and reliable seals reduce complaints, improve shelf presentation, and support efficient order fulfillment.
The Processing Infrastructure Behind Compliance
Start With Verified Apiary Sourcing
Honey from managed colonies provides a more controllable starting point than crude honey squeezed from uncontrolled or wild sources. Commercial buyers should assess beekeeper traceability, harvest practices, floral source claims, and available laboratory documentation.
Equipment should not be used to conceal poor raw-material quality. Processing can remove physical impurities and standardize handling, but it cannot reliably transform adulterated or chemically noncompliant honey into legitimate premium honey.
Build in Laboratory Verification
Laboratory testing is necessary to verify purity and chemical composition before packaging, especially for unifloral, therapeutic, premium, or export products. Testing may also be required after blending or when a batch falls outside expected parameters.
Processing facilities should define where samples are taken, how batches are identified, and what happens when results fail specification. Equipment suppliers serving commercial operators should be able to support these procedures with hygienic sampling points, batch controls, and technical documentation.
Separate Processing From General Premises
Food-safety rules commonly require a dedicated, sanitary processing room separated from living or unsuitable spaces. The facility should support cleaning, pest control, controlled personnel movement, and protection from environmental contamination.
This requirement affects equipment layout as much as machine selection. Tanks, extractors, filters, and fillers need sufficient access for cleaning and maintenance without disrupting the hygienic flow of production.
Design for Cleaning and Maintenance
A machine’s purchase price is only one part of its commercial value. Operators should examine cleaning time, disassembly requirements, gasket and seal availability, corrosion resistance, spare-part access, and local service capability.
For resellers and distributors, dependable after-sales support is a practical compliance feature. A machine that remains idle because a food-contact seal or control component is unavailable can interrupt production and compromise delivery commitments.
Understanding the Trade-offs
Automation Versus Capital Cost
Automated filling and processing systems require more initial investment than manual equipment. They can, however, improve fill accuracy, reduce labor dependence, strengthen hygiene, and deliver more consistent output at commercial volumes.
The correct decision depends on throughput, product range, labor availability, compliance risk, and expected growth. Overly complex equipment can be inefficient for a small operation, while undersized manual systems can become a bottleneck for a growing distributor or packing facility.
Gentle Processing Versus Throughput
Lower-temperature, carefully monitored processing protects quality but may require longer residence times or more controlled handling. Aggressive heating can move honey through equipment faster, yet it may damage heat-sensitive characteristics and increase HMF.
Commercial operators should prioritize measurable process control over maximum speed. A stable process that consistently meets specification is more valuable than high nominal capacity that produces variable batches.
Fine Filtration Versus Natural Characteristics
More intensive filtration can create a cleaner-looking product and simplify certain packaging requirements. It may also remove naturally occurring particles or characteristics that matter for specialty products, origin claims, or customer expectations.
The filtration system should reflect the intended product identity. Standardized retail honey, raw-style honey, and premium specialty honey may require different process configurations.
Standardization Versus Product Differentiation
Blending and moisture control can produce consistent commercial batches, which is useful for wholesalers and large retailers. Excessive standardization may reduce the sensory distinctions associated with floral origin, region, or harvest season.
Producers should decide whether their market prioritizes uniformity, provenance, specialty attributes, or a combination. That decision should guide tank capacity, blending capability, filtration, and testing requirements.
Certification Versus Operational Complexity
Certifications such as kosher approval can expand market access, but certification may assess raw materials, cleaning practices, production procedures, and equipment. The machinery must be compatible with the certifying body’s requirements rather than merely described as food-grade.
Certification should be considered before purchasing the line. Retrofitting equipment or changing production procedures later can be more disruptive than selecting compatible components from the outset.
Making the Right Choice for Your Goal
The best equipment package is the one that aligns regulatory requirements, product positioning, production volume, and service support.
- If your primary focus is regulatory compliance: Choose food-grade, hygienically designed equipment with controlled temperature management, precise filling, cleanable contact surfaces, and documentation that supports inspections and certification.
- If your primary focus is premium or therapeutic honey: Prioritize gentle thermal handling, suitable filtration, controlled storage, and laboratory verification that protects enzymes, aroma, HMF limits, and other defined product characteristics.
- If your primary focus is wholesale consistency: Invest in accurate automated filling, dependable settling and filtration systems, batch controls, and standardized containers that support repeatable volumes and efficient distribution.
- If your primary focus is market expansion: Select modular equipment and a supplier capable of rapid delivery, spare-parts support, technical guidance, and configurations compatible with the regulations and certifications of your target markets.
- If your primary focus is cost control: Match capacity and automation to actual throughput while avoiding compromises in food-contact materials, sanitation, temperature control, and quality testing.
The right commercial honey equipment turns regulatory obligations into repeatable quality, stronger buyer confidence, and dependable access to demanding markets.
Summary Table:
| Aspect | Impact | Equipment Solution |
|---|---|---|
| Purity | Must meet chemical/physical parameters | Food-grade stainless steel, hygienic design |
| Adulteration | Need controlled processing | Traceable batch records, precise temperature control |
| Temperature | Heat can damage honey | Temperature-controlled extractors, warming tanks |
| Filtration | Must match product spec | Adjustable filtration systems |
| Moisture | Risk of spoilage | Moisture meters, controlled storage |
| Filling/Sealing | Accuracy and hygiene | Automated fillers, sanitary seals |
| Cleaning | Prevent contamination | Easy-to-clean, accessible components |
| Certification | Market access | Equipment compatible with certifying bodies |
Partner with HONESTBEE for compliant honey processing equipment. We supply food-grade stainless steel extractors, temperature-controlled tanks, precise fillers, and filtration systems. Our fast delivery and expert support ensure your operation meets global standards. Contact us today for a tailored solution that protects honey quality and builds buyer trust. Get in touch.
Related Products
- Electric Double Wall Honey Filtering Machine Purifier Equipment for Honey Processing Plant
- 0.5T Capacity Honey Dehumidifier Dryer with Vacuum Heating and Thickening Filtering Machine
- Heavy Duty Stainless Steel Honey Processing Machine Decrystallizing Tank
- Double Wall Honey Heating Stirring Homogenizer Mixing Machine with Various Capacity
- Economy Honey Homogenizer Mixer and Melting Machine for Beekeeping
People Also Ask
- What is the process of filtering honey? A Guide to Clean, Pure, and Market-Ready Honey
- What types of equipment are used in honey filtering? Build an Efficient System for Pure, Marketable Honey
- What is the overall importance of using the right equipment in honey filtering? Boost Quality & Marketability
- What is a potential concern associated with filtering honey? Balancing Clarity and Pollen Preservation
- What role do professional honey harvesting and filtering equipment play in meeting honey market quality standards? Boost ROI