Specialized honey fermentation and brewing equipment increases the commercial value of honey by transforming raw commodities into high-margin, shelf-stable products like mead and standardized retail honey. This technology ensures product consistency, improves sensory qualities such as clarity and fluidity, and allows honey to meet the rigorous grading standards required for high-end retail distribution.
The core value of specialized honey equipment lies in its ability to bridge the gap between raw apiary output and the demands of the global supply chain. By enabling product diversification and industrial-scale standardization, this equipment maximizes profitability for distributors and ensures a consistent, high-quality inventory.
Driving Market Diversification and High-Value Mead Production
Expanding Downstream Market Opportunities
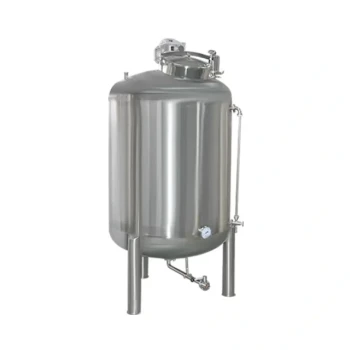
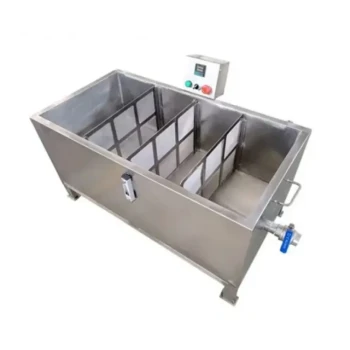
Specialized fermentation tanks and brewing systems allow for the conversion of honey into mead, a high-value alcoholic beverage. This diversification provides distributors with access to the craft beverage market, moving beyond the traditional food and sweetener sectors.
Enhancing Industrial Consistency
Temperature-controlled fermentation and professional brewing equipment ensure that every batch of mead maintains a uniform flavor profile. This industrial consistency is critical for building brand loyalty and securing long-term contracts with major retail chains.
Capturing Premium Pricing
By adding value through fermentation, the price-per-unit of the raw honey is significantly amplified. This transition from a bulk commodity to a specialized consumer good allows for higher margins across the entire distribution network.
Industrial Standardization: From Raw Material to Retail-Ready Asset
Improving Sensory Qualities and Consumer Preference
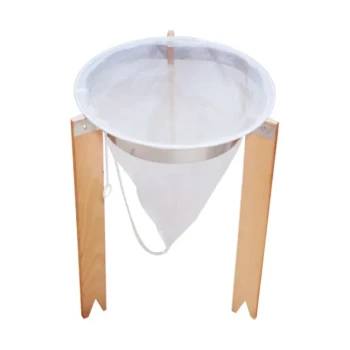
Professional filtration and moisture control units remove impurities like wax and larvae fragments while stabilizing moisture content. Data indicates that 62.3% of consumers prefer processed honey due to its superior transparency and fluidity, directly impacting the final retail price.
Meeting Strict Regulatory and Retail Standards
Industrial-grade processing ensures that honey meets the hygiene and safety requirements necessary for formal distribution. Specialized equipment eliminates physical impurities and prevents secondary contamination, making the product "shelf-ready" for high-end markets.
Extending Shelf Life for Global Distribution
Advanced moisture control and airtight packaging technology significantly extend the shelf life of honey products. For wholesalers and distributors, this reduced spoilage risk is vital for managing long-distance logistics and large-scale inventory.
Operational Efficiency and Supply Chain Reliability
Scaling with Automated Packaging
Automated filling machines utilize precise quantitative technology to ensure weight consistency and rapid order fulfillment. This mechanization allows beekeeping operations to scale up to meet the high-volume demands of large-scale retail contracts.
One-Stop Sourcing and Rapid Response
Distributors benefit most from partners who utilize a full-spectrum portfolio of processing equipment. Specialized machinery enables a "one-stop" sourcing model where raw, processed, and fermented honey products can be fulfilled from a single, expert provider.
Precision Metering and Brand Integrity
Modern filling and sealing machinery protect the integrity of the brand by ensuring every jar is identical in volume and quality. This level of precision is essential for maintaining the professional reputation of B2B resellers in competitive markets.
Understanding the Trade-offs and Limitations
Capital Intensity vs. Long-Term Yield
The primary drawback of specialized equipment is the significant initial capital investment required for procurement and setup. While these costs are high, they are generally offset by the increased marketability and higher price points of the finished goods.
Technical Expertise and Maintenance
Operating sophisticated fermentation and filtration systems requires specialized training and regular technical maintenance. Without a commitment to professional oversight, the equipment may underperform, leading to inconsistencies that negate its commercial value.
Processing vs. Raw Natural Appeal
While 62.3% of consumers prefer processed honey, there remains a niche market for raw, "unfiltered" products. Distributors must balance their inventory between standardized industrial products and artisanal raw options to capture the full spectrum of market demand.
Making the Right Choice for Your Goal
When selecting honey products or processing partners, your equipment standards should align with your specific commercial objectives:
- If your primary focus is high-volume retail distribution: Prioritize products processed with automated filtration and moisture control systems to ensure shelf stability and uniform appearance.
- If your primary focus is expanding into the luxury or craft beverage sector: Invest in partnerships that utilize professional-grade mead fermentation tanks to capture high-margin niche markets.
- If your primary focus is supply chain efficiency and reliability: Seek suppliers with integrated, one-stop processing and packaging capabilities to ensure rapid fulfillment and consistent weight accuracy.
The strategic implementation of specialized equipment is the definitive factor in transforming honey from a simple farm output into a sophisticated, high-value commercial asset.
Summary Table:
| Equipment Category | Key Commercial Function | Strategic Advantage |
|---|---|---|
| Fermentation Systems | Mead & Craft Beverage Production | Access high-margin niche markets |
| Moisture & Filtration | Industrial Standardization | Meets global retail & safety standards |
| Automated Packaging | Quantitative Filling & Sealing | Rapid fulfillment & brand consistency |
Scale Your Honey Business with HONESTBEE’s Professional Solutions
Are you a distributor or B2B reseller looking to maximize profit margins and ensure supply chain reliability? HONESTBEE is your premier partner for one-stop beekeeping sourcing. We provide a full-spectrum portfolio, from honey-filling machines and hive-making equipment to essential consumables and cultural merchandise.
Why partner with HONESTBEE?
- Comprehensive Portfolio: Access a complete array of beekeeping tools, specialized hardware, and machinery.
- Unmatched Efficiency: Benefit from ultra-fast delivery and rapid response times to meet high-volume market demands.
- Professional Expertise: Leverage our deep industry knowledge to ensure your products meet the highest certification and grading standards.
- Premium Service: Dedicated support tailored to the needs of commercial apiaries and wholesalers.
Ready to enhance your inventory with high-value honey processing technology?
Contact HONESTBEE today to optimize your wholesale operations!
References
- Віктор Арісович Чалаван. ВСЕРОСІЙСЬКІ З’ЇЗДИ БДЖОЛЯРІВ ПОЧАТКУ ХХ СТ. ЯК ВАЖЛИВИЙ ІНСТРУМЕНТ ДЛЯ ВИРІШЕННЯ ГАЛУЗЕВИХ ПИТАНЬ. DOI: 10.31392/vah-2024.49-50.24
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Manual Honey Filling Machine Bottling Machine for Honey
- Double Nozzle Small Honey Filling Machine Honey Sachet Packing Packaging Equipment
- Small Honey Filling Machine Sachet Packing Equipment Single Nozzle
- Fully Automatic Honey Filling Packaging Machine for Processing Line
- Economy Small Honey Filling Machine Honey Bottle Filler Packaging Machine
People Also Ask
- What is a manual honey filler and where is it used? The Essential Guide for Small-Scale Honey Bottling
- What is a manual filling machine? The Ultimate Guide for Small-Batch Producers
- What are the benefits of utilizing professional honey filling machines? Scale Your Production with Precision
- What types of filling mechanisms are used in honey filling machines? Find the Best Tech for Your Viscosity
- What are the main differences between automated and manual honey filling? Scale Your Bottling Operation