Professional honey harvesting and filtering equipment are the technical foundation for commercial viability in the global honey trade. These specialized tools remove physical impurities such as wax, larvae, and debris while managing moisture levels to prevent spoilage and fermentation. By standardizing the purity, clarity, and physicochemical stability of the honey, this equipment ensures products meet the rigorous food safety and sensory standards required by supermarkets, pharmacies, and international export markets.
Core Takeaway: Professional equipment transforms raw, inconsistent honey into a standardized, high-clarity commodity that satisfies international regulatory and retail requirements. For distributors and wholesalers, providing or utilizing these systems is the essential step for securing access to high-margin markets and ensuring supply chain reliability.
Achieving Compliance with Global Quality Standards
Ensuring Physical Purity and Clarity
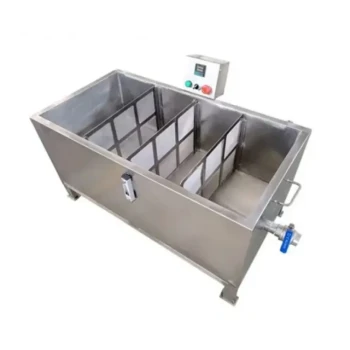
Professional filtration systems use multi-stage physical screening to remove beeswax residue, bee parts, and forest debris. This process significantly improves the color uniformity and transparency of the honey, which is a primary requirement for entering formal retail channels.
Utilizing Centrifugal Force for Extraction
Unlike manual squeezing, professional extraction machines use centrifugal force to separate ripened honey from the comb. This method preserves the integrity of the honeycomb and minimizes the initial introduction of impurities, maintaining the honey’s natural hygiene and bio-active content.
Physicochemical Parameter Control
High-quality processing machinery helps manage moisture content and prevents phase separation or layering. By maintaining consistent internal structures, the equipment ensures the honey meets the strict physicochemical parameters required for premium grading and international export labels.
Strategic Market Advantages for Distributors
Unlocking High-End Retail and Export Channels
Raw or crude honey is often restricted to local markets due to its high impurity levels and variable shelf life. Professional filtering is the key technical bridge that allows distributors to supply sophisticated consumer segments and meet the strict entry requirements of international trade.
Extending Shelf Life and Marketability
Effective filtration and temperature control prevent uneven crystallization and sediment formation over time. This extends the product's shelf life and maintains its aesthetic appeal on retail shelves, directly increasing the market competitiveness of the honey brand.
Protecting the Nutritional Profile
Advanced systems are designed to remove debris while preserving essential nutrients and enzymes. This allows wholesalers to market their honey as a premium, "pure" product that retains its natural health benefits while meeting modern food safety protocols.
Understanding the Trade-offs and Pitfalls
Balancing Throughput with Filtration Fineness
Using ultra-fine filters can achieve extreme clarity but may significantly slow down production speeds and increase pressure on the machinery. Distributors must choose equipment that balances the need for high-volume order fulfillment with the specific clarity standards of their target market.
Thermal Processing Risks
While temperature-controlled systems are vital for preventing crystallization, excessive heat can damage the honey’s delicate enzymes and darken its color. It is critical to use professional-grade equipment with precise sensors to avoid "cooking" the honey and lowering its market grade.
Initial Capital Investment vs. Long-Term Yield
Professional machinery requires a higher upfront cost compared to manual methods. However, the reduction in waste and the ability to command higher price points in premium markets typically offset these initial expenses for serious commercial operations.
How to Apply This to Your Distribution Strategy
Making the Right Choice for Your Goal
- If your primary focus is international export: Prioritize multi-stage centrifugal extractors and fine filtration systems that guarantee compliance with international physicochemical and purity standards.
- If your primary focus is rapid order fulfillment: Invest in high-capacity, automated processing lines that offer a comprehensive "one-stop" solution from extraction to bottling to minimize lead times.
- If your primary focus is premium "raw" branding: Select low-heat, gravity-assisted or coarse-filtration equipment that removes major debris while maximizing the retention of pollen and bio-active compounds.
By integrating professional harvesting and filtering technology into your supply chain, you ensure a consistent, high-quality product that meets the expectations of the most demanding global buyers.
Summary Table:
| Key Equipment Feature | Primary Function | Strategic Market Benefit |
|---|---|---|
| Multi-stage Filtration | Removes wax, larvae, and debris | Ensures visual clarity for high-end retail entry |
| Centrifugal Extraction | Efficiently separates honey from combs | Preserves bio-active content and natural hygiene |
| Moisture Control | Regulates water levels | Prevents fermentation and extends product shelf life |
| Automated Processing | High-speed filling and grading | Facilitates rapid order fulfillment and scalability |
Scale Your Honey Distribution Business with HONESTBEE
Are you a distributor or B2B reseller looking to dominate the global honey market? HONESTBEE is your strategic partner for one-stop sourcing of premium beekeeping technology. From specialized hive-making and honey-filling machinery to a full spectrum of industry consumables, we provide the tools you need to ensure international quality compliance and maximize profit margins.
Why Partner with HONESTBEE?
- Comprehensive Portfolio: Full-spectrum hardware, machinery, and cultural merchandise.
- Rapid Fulfillment: Ultra-fast delivery and efficient order processing to keep your supply chain moving.
- Industry Expertise: Professional guidance on OEM/ODM support and certification requirements.
- Exceptional Service: Dedicated support to help you capture high-margin export opportunities.
Ready to elevate your inventory? Contact our expert team today to receive a customized wholesale quote and discover how our equipment can drive your business growth.
References
- Hezron Tirok, Andrew Kimwolo. Effect of Information Materials Provision on Implementation of Bee-Keeping Projects in Baringo County, Kenya. DOI: 10.37284/eajbe.7.1.2184
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Electric Double Wall Honey Filtering Machine Purifier Equipment for Honey Processing Plant
- Professional Stainless Steel Honey Filtering Machine with Water Bath Heating for Beekeeping
- 0.5T Capacity Honey Dehumidifier Dryer with Vacuum Heating and Thickening Filtering Machine
- Professional Stainless Steel Honey Filter with Support Handle
- Honey Concentrating and Filtering Dehumidifier Machine 2T Capacity for Honey
People Also Ask
- What is the process of filtering honey? A Guide to Clean, Pure, and Market-Ready Honey
- What types of equipment are used in honey filtering? Build an Efficient System for Pure, Marketable Honey
- What is the overall importance of using the right equipment in honey filtering? Boost Quality & Marketability
- How should honey filtering equipment be properly maintained? Extend Equipment Life & Protect Honey Purity
- What are the benefits of drying honey filtering equipment after use? Protect Your Honey Quality & Equipment Investment