Precision filtration systems are the critical final gatekeeper in honey post-processing, ensuring the total removal of wax particles, bee fragments, and environmental dust. By utilizing multi-stage fine-pore meshes, these systems elevate raw honey into a shelf-ready, high-purity commercial asset that meets strict international hygiene standards while preserving its natural nutritional profile.
Core Takeaway: Precision filtration is essential for transforming raw honey into a stable, transparent, and compliant product by removing physical contaminants that trigger spoilage and crystallization. For B2B resellers, this technology is the foundation of product reliability and brand trust.
Enhancing Commercial Marketability and Visual Appeal
Achieving Crystal-Clear Transparency
In the global marketplace, transparency is a proxy for quality. Precision filtration removes microscopic impurities and larval residues that cause cloudiness, ensuring the honey meets the high-end sensory expectations of professional buyers.
Maintaining Nutritional Integrity
Expertly configured systems allow for the removal of debris without stripping the honey of its natural chemical composition. This balance ensures that the product remains "pure" and "natural" on the label, which is a key selling point for premium wholesalers.
Ensuring Uniform Texture
Standardized filtration at the end of the production line guarantees a uniform texture and color. This consistency is vital for distributors who must provide predictable quality across large-scale, recurring orders.
Mitigating Biological Risks and Ensuring Compliance
Reducing Microbial Contamination
Physical debris like dust and bee fragments often carry microbial risks, including botulinum spores. By removing these carriers, precision filtration significantly lowers the risk of contamination, protecting the reseller from costly recalls.
Meeting Global Regulatory Standards
High-precision equipment is designed to comply with strict regulations, such as EU Council Directive 2001/110/EC. These standards prohibit foreign matter in honey while requiring that natural pollen content remain largely intact.
Preventing Spoilage and Fermentation
In specific varieties like stingless bee honey, high moisture and organic solids can trigger fermentation. Precision filtration removes the solid triggers for spoilage, ensuring the honey remains stable during long-term transit and storage.
Protecting Shelf-Life and Physical Stability
Inhibiting Premature Crystallization
Physical impurities often act as "seeds" or nuclei that accelerate crystallization. By stripping out these particles, filtration extends the liquid shelf-life of the honey, preventing it from turning into an unmarketable solid block in the warehouse.
Enhancing Long-Term Physicochemical Stability
Removing suspended solids ensures that the honey's physical properties remain unchanged over time. This stability is a core requirement for efficient order fulfillment, as it reduces the need for re-processing or heating prior to retail bottling.
Synergistic Settling and Filtration
Advanced processing lines combine precision filtration with gravitational settling tanks. This dual approach removes both solid particles and air bubbles, resulting in a dense, clear product with superior pourability.
Understanding the Trade-offs and Pitfalls
The Risk of Over-Filtration
Excessive filtration can remove natural pollen grains, which may lead to legal challenges regarding the product's origin or classification as "honey" in certain jurisdictions. It is critical to select the correct micron rating to balance purity with authenticity.
Thermal Impact on Quality
Some filtration processes require the honey to be slightly warmed to reduce viscosity. If not managed with professional industry expertise, excessive heat can damage the honey's enzymes and darken its color, degrading its market value.
Maintenance and Mesh Integrity
Lower-quality filter elements can fail under pressure, leading to "bypass" where contaminants leak into the final batch. Sourcing from a partner with a comprehensive product portfolio and rigorous quality control is essential to avoid these production gaps.
Strategic Sourcing for Your Inventory
Selecting the right filtration partner is not just about the equipment; it is about the reliability of the supply chain and the expertise behind the product.
- If your primary focus is Rapid Market Entry: Prioritize suppliers offering ultra-fast delivery and one-stop sourcing to ensure your inventory is never depleted.
- If your primary focus is Regulatory Compliance: Seek out partners with deep professional expertise who can provide certified, multi-stage stainless steel filtration systems that meet EU and FDA standards.
- If your primary focus is Product Premiumization: Focus on high-precision systems that guarantee maximum transparency and shelf-stability to appeal to high-end retail distributors.
By integrating precision filtration into your quality control standards, you ensure a high-purity, stable product that minimizes risk and maximizes profit potential across the global supply chain.
Summary Table:
| Key Benefit | Impact on Honey Quality | Value for Distributors & Wholesalers |
|---|---|---|
| Physical Purity | Removes wax, bee fragments, and dust | Enhances visual transparency and premium market appeal |
| Microbial Safety | Filters out solid carriers of bacteria/spores | Reduces risk of contamination and costly product recalls |
| Shelf-Life Extension | Eliminates nuclei that trigger crystallization | Prevents solidification and ensures long-term pourability |
| Global Compliance | Meets EU/FDA standards for foreign matter | Facilitates smooth international trade and customs clearance |
| Stability | Removes organic solids that cause fermentation | Ensures consistent product quality during long-distance transit |
Scale Your Honey Distribution with HONESTBEE Expert Solutions
Partner with HONESTBEE to elevate your product quality and streamline your supply chain. As a premier partner for commercial apiaries and B2B resellers, we offer a one-stop sourcing experience for the full spectrum of beekeeping tools, machinery, and consumables.
Our professional-grade precision filtration and honey-filling machines are designed to help you meet strict international standards while maximizing profit margins. By choosing HONESTBEE, you gain access to:
- Deep Industry Expertise: Tailored advice on OEM/ODM support and regulatory compliance.
- Rapid Fulfillment: Ultra-fast delivery times to keep your inventory ready for market demand.
- Comprehensive Portfolio: From hive-making hardware to honey-themed cultural merchandise.
Ready to enhance your product reliability and brand trust? Contact our team today to discover how our wholesale offerings can grow your business!
References
- Sibani Moharana, Surya Narayan Pradhan. Contaminants in Honey: A Comprehensive Review of Sources, Risks, and Detection Methods. DOI: 10.7759/s44388-025-06985-5
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
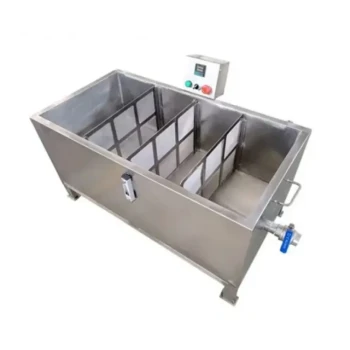
- Electric Double Wall Honey Filtering Machine Purifier Equipment for Honey Processing Plant
- Professional Stainless Steel Honey Filtering Machine with Water Bath Heating for Beekeeping
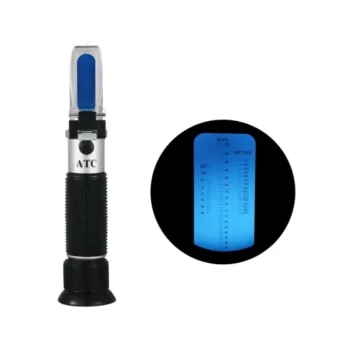
- Precision Honey Refractometer Instrument for Quality Assessment
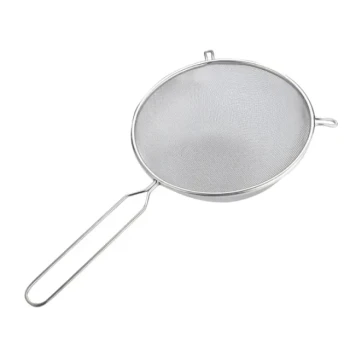
- Professional Stainless Steel Honey Filter with Support Handle
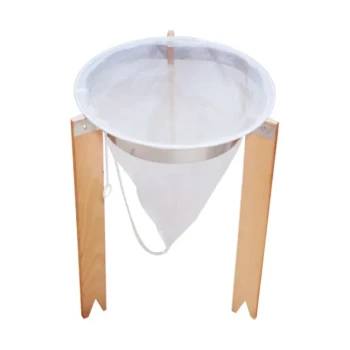
- Professional Honey Filter with Tripod Support Stand
People Also Ask
- What is the process of filtering honey? A Guide to Clean, Pure, and Market-Ready Honey
- What types of equipment are used in honey filtering? Build an Efficient System for Pure, Marketable Honey
- What is the overall importance of using the right equipment in honey filtering? Boost Quality & Marketability
- Why is filtering important in honey processing, and what equipment is used? A Guide to Quality & Efficiency
- How should honey filtering equipment be properly maintained? Extend Equipment Life & Protect Honey Purity