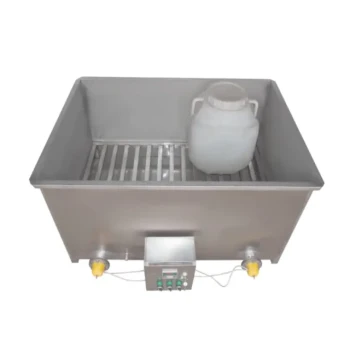
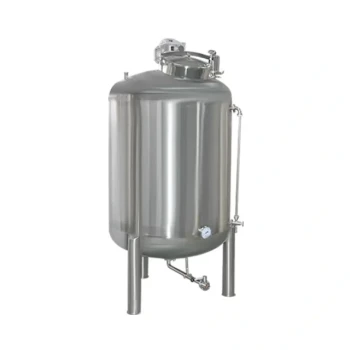
Professional honey clarification and settling tanks are essential because they provide the necessary static environment for gravity-based purification. By allowing the honey to rest, these tanks facilitate the natural separation of air bubbles, fine wax debris, and larval remains that mechanical filtration might miss. This process ensures the final product meets the highest commercial grading standards for clarity and transparency before it reaches the packaging line.
The use of industrial settling tanks is a critical quality-control step that transforms raw extracted honey into a high-purity, market-ready product by leveraging physical sedimentation to remove impurities without damaging the honey’s nutritional integrity.
Optimizing the Physical Sedimentation Process
Leveraging Density and Gravity
Settling tanks utilize the principle of density differences to achieve natural clarification. In a static environment, air bubbles and low-density impurities like wax particles rise to the surface to form a "scum layer," while heavier micro-particles sink to the bottom.
This stratification allows for the easy removal of foreign matter, ensuring the liquid remains crystal clear. Without this resting period, packaged honey often appears cloudy or develops an unsightly foam layer at the top of the jar.
Precision Temperature Management
Professional tanks are designed to maintain a controlled environment, typically between 25 and 30 degrees Celsius. This specific temperature range reduces the honey's viscosity, allowing impurities to move through the liquid more efficiently.
By managing the climate within the tank, producers achieve high-purity results without resorting to excessive heat. This protects the delicate enzymes and nutritional components that B2B buyers and health-conscious consumers demand.
Commercial Value and Operational Excellence
Enhancing Market Grading
The visual quality of honey is a primary factor in its commercial market value. Distributors and wholesalers require honey that is free of suspended impurities to meet strict retail grading requirements.
Using professional clarification equipment ensures that every batch is consistent in its transparency. This consistency builds brand trust and allows resellers to command premium prices in competitive markets.
Improving Production Analytics
Clarification and settling tanks play a vital role in production analysis and yield accuracy. By removing non-honey substances before the final weighing, producers can provide distributors with precise data on the actual volume of pure honey.
This level of professional industry expertise ensures that inventory records are accurate. It also prevents impurities from interfering with the physical stability of the honey during long-term storage or international transit.
Understanding the Trade-offs
Time vs. Throughput
The primary trade-off in the clarification process is the required standing time. Achieving maximum purity often requires the honey to sit for 24 hours or longer, which can create a bottleneck in high-volume fulfillment cycles.
To mitigate this, sophisticated sourcing partners use large-capacity tank portfolios. This allows for a continuous workflow where multiple batches can settle simultaneously, ensuring ultra-fast delivery without compromising on clarity.
The Risk of Over-Processing
While high heat can speed up the settling process, it risks increasing HMF (hydroxymethylfurfural) levels, which can downgrade the honey’s quality. Professional-grade tanks avoid this pitfall by using gentle, indirect heating elements.
Relying on gravity and time rather than extreme heat preserves the honey's original sensory profile. For distributors, this means a product that retains its natural aroma and flavor, leading to higher customer satisfaction.
Selecting the Right Solution for Your Portfolio
Strategic Advice for Distributors and Wholesalers
Choosing the right processing standards is critical for maintaining a competitive edge in the honey trade. Your sourcing strategy should align with your specific market segment and customer expectations.
- If your primary focus is premium retail distribution: Ensure your suppliers use multi-stage sedimentation and skim off all surface impurities to guarantee a "jewel-like" clarity in the jar.
- If your primary focus is high-volume food service: Look for partners with extensive tank capacities that can fulfill large orders rapidly while still providing the necessary 24-hour settling time.
- If your primary focus is organic or health-oriented markets: Prioritize suppliers who use low-temperature clarification to ensure that the honey's bioactive properties remain intact.
By integrating professional clarification and settling into your quality standards, you ensure a product that is as pure and stable as it is visually appealing.
Summary Table:
| Key Feature | Process Benefit | Impact on Commercial Value |
|---|---|---|
| Gravity Sedimentation | Removes wax debris and air bubbles | Ensures crystal-clear, premium retail appearance |
| Precision Temp. Control | Maintains honey at 25-30°C | Preserves delicate enzymes and nutritional integrity |
| Static Environment | Facilitates natural stratification | Prevents unsightly foam layers in the final package |
| Impurity Skimming | Removes surface scum layers | Guarantees consistent high-purity grading per batch |
| Volume Accuracy | Removes non-honey substances | Provides precise yield data for inventory management |
Optimize Your Supply Chain with HONESTBEE
Partner with HONESTBEE to access a one-stop sourcing powerhouse designed for commercial apiaries, wholesalers, and B2B resellers. We supply a comprehensive full-spectrum product portfolio—ranging from specialized honey-filling and hive-making machines to essential industry consumables and honey-themed cultural merchandise.
By choosing HONESTBEE, you benefit from our deep professional industry expertise, rapid response times, and ultra-fast delivery, ensuring your inventory is always stocked and market-ready. Our premium trading services are tailored to help distributors maximize profit margins and maintain supply reliability with ease.
Ready to elevate your beekeeping wholesale operations? Contact us today for a custom quote!
References
- Hakan İNCİ, Osman TOPLUK. Bingöl İli Arıcılık İşletmelerinin Yapısal Özellikleri. DOI: 10.30910/turkjans.1174465
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Stainless Steel Honey Storage and Settling Tank with Double Strainer
- Heavy Duty Stainless Steel Honey Processing Machine Decrystallizing Tank
- Stainless Steel Honey Storage Tank with Lid for Honey
- Professional Honey Storage Tank with Agitation System
- Stainless Steel Uncapping Tank with Stand and Strainer
People Also Ask
- What economic role do honey storage tanks play? Boost Your Revenue Through Strategic Inventory Management
- What roles do industrial honey storage tanks and filtration meshes play in processing? Ensure Purity & Consistency
- What is the purpose of a honey storage tank? Streamline Your Honey Processing for Quality & Efficiency
- What role do settling tanks play in honey production? Achieve Pure, High-Clarity Honey Naturally
- Why are large settling tanks used in the honey clarification process? Achieve Natural Purity & Batch Consistency