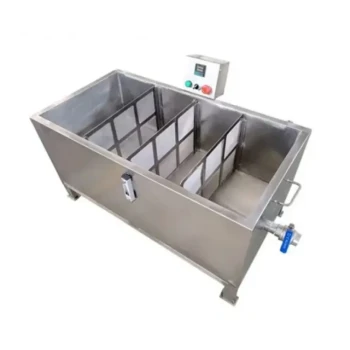
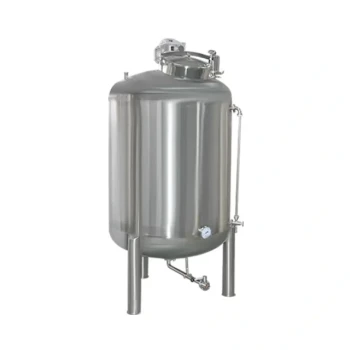
Ensuring honey quality at scale requires a synergy between mechanical purity and thermal precision. Industrial-grade filtration systems remove physical impurities like wax and larvae remains to guarantee clarity, while precision heating reduces viscosity for efficient processing. This dual approach prevents the formation of harmful by-products like hydroxymethylfurfural (HMF) and preserves the delicate natural enzymes that define premium honey.
Professional honey processing relies on specialized equipment to balance high-volume throughput with the preservation of biological integrity, ensuring every batch meets international safety and aesthetic standards.
The Role of Industrial-Grade Filtration in Marketability
Achieving Superior Visual Clarity and Texture
Industrial filtration utilizes multi-stage precision mesh to eliminate beeswax debris, air bubbles, and organic residues. This process is vital for distributors because it significantly improves the sensory evaluation and visual appeal of the product on retail shelves.
Beyond aesthetics, removing these particles is a functional necessity. By eliminating microscopic "seeds" of crystallization, such as pollen clumps or dust, filtration delays the crystallization process, extending the liquid shelf life of the honey during transport and storage.
Balancing Purity with Regulatory Compliance
While filtration removes unwanted sediment, expert processing ensures that the honey is not "over-filtered." Standardized production must remain compliant with regulations like the EU Honey Directive, which protects the natural integrity of the product.
A sophisticated sourcing partner understands how to calibrate filtration levels to meet specific market standards, such as the PN-88/A-77626. This technical expertise ensures that the honey remains a "natural" product while meeting the high purity requirements of global commercial exports.
Precision Heating: Protecting Nutritional Value
Safe Liquefaction and Viscosity Control
Honey is naturally thick, making large-scale filtration and automated bottling difficult without heat. Precision temperature-controlled systems allow for the liquefaction of honey by maintaining a narrow temperature range that reduces viscosity without damaging the product.
This "micro-heating" approach ensures the honey meets the fluid performance requirements necessary for high-speed industrial filling lines. For wholesalers, this translates to consistent product uniformity and efficient order fulfillment across large volumes.
Preventing HMF Formation and Enzyme Loss
Excessive or uncontrolled heat treatment leads to the irreversible formation of 5-Hydroxymethylfurfural (HMF), a potential carcinogen and a key indicator of poor quality. Precision systems prevent HMF spikes, ensuring the honey remains safe and legally compliant for sale.
Furthermore, these systems are designed to preserve active enzymes and natural antioxidant properties. By protecting the honey’s biological "fingerprint," processors ensure that the final product retains its status as a high-value, nutritional superfood.
Understanding the Trade-offs and Pitfalls
The Risk of Over-Processing
The greatest challenge in honey processing is the trade-off between shelf stability and natural content. While fine filtration creates a crystal-clear product that stays liquid longer, it can also remove natural pollen, which some markets use for origin tracing and quality verification.
Equipment Calibration and Maintenance
Inadequate maintenance of heating elements can lead to "hot spots" within a batch, causing localized overheating even if the average temperature seems correct. Distributors should partner with suppliers who utilize automated monitoring systems to ensure thermal consistency across the entire production run.
Choosing the Right Processing Standards for Your Market
As a B2B partner, understanding these technical nuances allows you to select products that align with your specific distribution goals and regional regulations.
- If your primary focus is long shelf life and retail "sparkle": Prioritize honey processed through fine, multi-stage filtration systems that remove all precursors to crystallization.
- If your primary focus is high-end health and wellness markets: Ensure your supplier utilizes low-temperature precision heating to guarantee maximum enzyme retention and low HMF levels.
- If your primary focus is international export and compliance: Choose a partner with deep industry expertise who can provide certificates of analysis proving adherence to the EU Honey Directive.
By integrating advanced filtration and thermal control, processors deliver a safe, stable, and nutritionally intact product that satisfies both regulatory bodies and the end consumer.
Summary Table:
| Processing Feature | Primary Function | Key Benefit for Distributors |
|---|---|---|
| Multi-stage Filtration | Removes wax, debris, and air bubbles | Superior visual clarity and extended liquid shelf life. |
| Precision Heating | Reduces viscosity for flow control | Efficient high-speed filling and consistent uniformity. |
| Thermal Monitoring | Prevents HMF formation | Ensures safety compliance and low chemical degradation. |
| Enzyme Preservation | Maintains biological integrity | Retains high-value nutritional status and health benefits. |
Scale Your Honey Business with HONESTBEE Expertise
Are you looking to optimize your honey processing line or expand your wholesale inventory? HONESTBEE is your premier partner for one-stop beekeeping solutions. We cater specifically to commercial apiaries and B2B distributors, offering a full spectrum of high-performance beekeeping tools, specialized honey-filling machinery, and essential industry consumables.
Why partner with us?
- Deep Industry Expertise: We ensure your equipment meets global standards like the EU Honey Directive.
- Comprehensive Portfolio: From hive-making hardware to honey-themed merchandise, we supply everything you need.
- Rapid Fulfillment: Benefit from our ultra-fast delivery and dedicated customer service to keep your operations running smoothly.
- Proven Reliability: High-quality machinery designed to maximize your profit margins and ensure product stability.
Ready to enhance your supply chain efficiency? Contact us today to explore our wholesale offerings and premium trading services!
References
- Beatriz Fernanda Boverio, Alice Deléo Rodrigues. Saúde das abelhas e produtos apícolas: implicações sobre o uso de produtos químicos e alimentos seguros. DOI: 10.52138/citec.v17i01.402
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Professional Stainless Steel Honey Filtering Machine with Water Bath Heating for Beekeeping
- 0.5T Capacity Honey Dehumidifier Dryer with Vacuum Heating and Thickening Filtering Machine
- Honey Concentrating Vacuum Heating Thickening Machine Dehumidifier for Honey
- Electric Double Wall Honey Filtering Machine Purifier Equipment for Honey Processing Plant
- Professional Stainless Steel Honey Filter with Support Handle
People Also Ask
- Why do people filter honey? For Clarity, Stability, and Consumer Appeal
- Is it necessary to filter honey after extraction? A Guide to Straining vs. Raw Honey
- What is the best way to filter honey? A Guide to Quality, Clarity, and Raw Preservation
- Why is filtering honey an important step in honey processing? Ensure Purity, Clarity & Marketability
- What are the benefits of using honey filters? Achieve Purity, Efficiency, and Market Appeal