Professional stingless bee harvesting and storage require precision-engineered vacuum extraction systems and climate-controlled, acid-resistant storage units. These systems must protect fragile cerumen pots from structural damage while managing the honey's naturally high moisture and acidity to prevent fermentation. For B2B distributors, sourcing equipment that integrates high-precision filling with medical-grade hygiene standards is essential for maintaining the high market value of these rare products.
To maintain the integrity of high-value stingless bee products, equipment must transition from traditional centrifugal methods to non-invasive suction technology and high-precision, temperature-regulated storage. This approach prevents product loss and preserves the unique medicinal and sensory profiles required by the global market.
Engineering Requirements for Harvesting Equipment
Non-Destructive Vacuum Suction
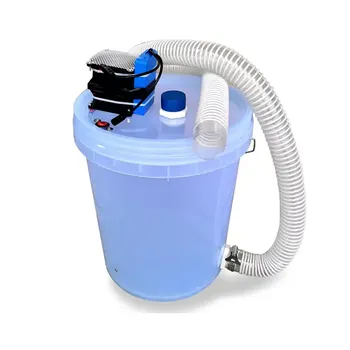
Unlike traditional honey bees, stingless bees store honey in cerumen pots (small wax containers) rather than frames. This renders standard centrifugal extractors unusable and requires specialized vacuum suction pumps or precision pipetting tools. These tools use gentle negative pressure to draw honey directly from the pots without puncturing nearby brood cells or destroying the hive's core structure.
Precision and Waste Reduction
Stingless bee honey yields are exceptionally low, often ranging from only 3 to 5 ml per hive per month. Professional-grade equipment must feature high-precision filling systems designed for minimal residual waste. Every drop represents significant market value, making precision calibration a critical requirement for economic profitability in large-scale operations.
Colony Preservation Design
The primary technical goal of harvesting tools is to ensure continuous productivity of the colony. Equipment must be designed to extract honey and pollen (saburá) without introducing external impurities or wax debris. By maintaining the integrity of the hive, professional tools allow for multiple harvests per year without harming the larvae or causing colony collapse.
Technical Standards for Post-Harvest Storage
Managing High Moisture and Fermentation
Stingless bee honey naturally possesses a higher water content than traditional honey, making it highly susceptible to fermentation. Industrial-grade storage equipment must utilize precise temperature and humidity controls to stabilize the product. Professional units often incorporate cooling systems that inhibit the growth of spoilage bacteria while preserving delicate enzyme activity.
Acid-Resistant Materials
The chemical profile of stingless bee honey is characterized by a low pH (high acidity). To prevent chemical leaching or degradation of the storage vessel, containers must be equipped with acid-resistant liners or be constructed from high-grade stainless steel. This ensures that the honey's unique flavor and therapeutic properties remain untainted during long-term storage.
Airtight Sealing and Hygiene
Superior sealing mechanisms are non-negotiable to prevent microbial contamination and the loss of volatile aromatic compounds. Storage systems should minimize contact between the honey and the air during the filling process. This level of hygiene is essential for meeting the strict standards required by pharmaceutical and high-end food distribution channels.
Understanding Technical Trade-offs and Pitfalls
Precision vs. Equipment Cost
High-precision machinery requires a larger initial investment but significantly reduces product loss during the filling stage. For distributors, the trade-off involves balancing the higher CAPEX of advanced suction systems against the long-term ROI of preserving a high-value, low-volume commodity.
Maintenance and Sanitation Complexity
Specialized vacuum systems and acid-resistant containers require more stringent cleaning protocols than traditional equipment. Failure to properly sanitize the internal components of a suction pump can lead to cross-contamination. Distributors must ensure that their technical partners provide comprehensive maintenance support and clear sanitation guidelines.
Strategic Sourcing for Distributors and Resellers
Selecting a partner who offers a full-spectrum portfolio ensures supply chain reliability and technical consistency across the entire harvesting and storage workflow.
- If your primary focus is rapid market entry: Prioritize one-stop sourcing for comprehensive harvesting kits that include both extraction and basic storage tools.
- If your primary focus is the premium pharmaceutical market: Invest in high-precision, industrial-grade storage units with advanced temperature control and acid-resistant certifications.
- If your primary focus is large-scale operational efficiency: Seek suppliers who offer ultra-fast delivery and automated filling systems to minimize downtime and maximize order fulfillment speed.
The right technical infrastructure is the foundation of a sustainable and profitable stingless bee product trade.
Summary Table:
| Feature | Technical Requirement | Primary Purpose |
|---|---|---|
| Harvesting Method | Non-destructive Vacuum Suction | Protects fragile cerumen pots and ensures colony survival. |
| Material Specs | Acid-resistant (SS316/Liners) | Prevents chemical leaching and corrosion from low-pH honey. |
| Climate Control | Precision Temp/Humidity Cooling | Stabilizes high moisture content to prevent fermentation. |
| Filling Accuracy | High-precision Micro-filling | Minimizes product waste for low-yield, high-value honey. |
| Sanitation | Industrial Medical-grade Sealing | Maintains hygiene for pharmaceutical and premium markets. |
Scale Your Stingless Bee Operation with HONESTBEE
Maximize your profit margins and ensure supply chain reliability with HONESTBEE, your dedicated partner for professional beekeeping infrastructure. We provide commercial apiaries and B2B distributors with a one-stop sourcing solution, offering a full-spectrum portfolio including:
- Specialized Machinery: Precision honey-filling machines and non-destructive vacuum extraction systems.
- Advanced Hardware: Acid-resistant storage units and specialized hive-making equipment.
- Full-Spectrum Consumables: Every essential tool required for large-scale stingless and traditional beekeeping.
Leverage our deep industry expertise, rapid response times, and ultra-fast delivery to stay ahead of the market. Contact HONESTBEE today to discuss OEM/ODM support and wholesale opportunities!
References
- Alessandra Fernandes Gonçalves Benites, Vagner de Alencar Arnaut de Toledo. ASPECTS OF MELIPONICULTURE WITH EMPHASIS ON THE GENUS SCAPTOTRIGONA. DOI: 10.18188/sap.v21i4.29493
This article is also based on technical information from HonestBee Knowledge Base .
Related Products
- Stainless Steel Beekeeping Honey Extractor Lid
- Stainless Steel Manual 8 Frame Radial Honey Extractor Machine for Beehives
- Stainless Steel Manual Honey Press with Guard for Pressing Honey and Wax
- 2 Frame Stainless Steel Manual Honey Spinner Extractor for Beekeeping
- HONESTBEE 2 Frame Manual Acrylic Honey Extractor Beekeeping Equipment
People Also Ask
- How do specialized organic beekeeping tools impact production efficiency? Maximize honey yields and ensure compliance.
- What are the advantages of selecting a stainless steel honey extractor over a plastic one? Pro Beekeeping Guide
- What is a stainless steel honey extractor? Boost Your Apiary's Efficiency with Professional Extraction
- What are the key features of a stainless steel honey extractor? Ensure Purity & Longevity for Your Honey
- What are the key features and benefits of a stainless steel honey extractor? Upgrade to Professional Purity