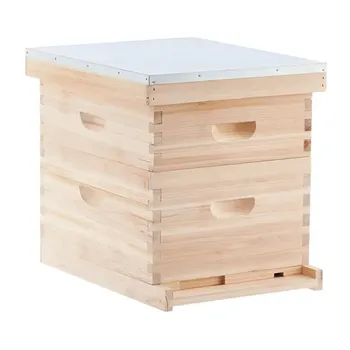
Modern movable-frame hives give commercial apiaries control, repeatability, and scale. Unlike traditional fixed-comb hives, Langstroth-style equipment allows individual frames to be removed, inspected, treated, harvested, and returned without destroying the comb or seriously disrupting the colony. This reduces labor and comb-rebuilding losses while supporting more efficient honey production, disease monitoring, colony management, and migratory operations.
The central advantage is reusability: movable frames turn the hive from a largely inaccessible structure into a manageable production system. Commercial beekeepers can inspect colonies, control risks, and harvest honey repeatedly while preserving the comb bees have already built.
Why Commercial Apiaries Need More Manageable Hive Equipment
Traditional hives limit inspection
In log hives, clay tube hives, top-bar systems, and historical skeps, comb is often fixed to the hive structure or difficult to remove intact. Inspecting brood, honey stores, queen performance, or disease conditions can therefore disturb the nest or require destructive handling.
Movable-frame hives provide direct access to individual combs. Beekeepers can examine the colony’s condition without dismantling the entire hive or destroying its working structure.
Commercial production depends on repeatable processes
A commercial apiary manages many colonies rather than a small number of individual hives. Equipment must therefore support consistent inspections, harvesting, maintenance, and record keeping across the operation.
Standardized frames and hive bodies create a repeatable management platform. This makes it easier for teams to follow the same procedures and for operators to expand their apiaries using compatible equipment.
How Movable Frames Improve Honey Yield and Efficiency
Reusable comb reduces wasted bee effort
When honey is harvested from fixed-comb hives, the comb may be damaged or destroyed. Bees must then consume resources and devote time to producing wax and rebuilding the comb before returning to full honey storage.
With movable frames, intact combs can be removed, extracted, and placed back into the hive. Bees can resume storing nectar in established comb rather than repeatedly rebuilding the foundation of production.
Centrifugal extraction protects the comb
Standardized frames are compatible with centrifugal honey extractors. The extractor removes honey from the comb while leaving the comb substantially intact for continued use.
This creates a more efficient harvest cycle and supports higher productivity than methods that require comb to be crushed, cut, or discarded after each harvest.
Harvesting causes less disruption
Non-destructive harvesting helps preserve the colony’s organization and working resources. The beekeeper can remove full honey frames while leaving brood areas and remaining stores in place.
That separation is particularly valuable in commercial operations, where unnecessary colony disruption can increase labor requirements and slow recovery.
How the Design Supports Scientific Colony Management
Inspections become targeted rather than destructive
A beekeeper can remove and inspect selected frames instead of disturbing the entire hive. This allows more precise monitoring of brood development, honey stores, queen performance, and colony strength.
Targeted inspection also helps operators identify problems earlier and apply management measures before they become larger production or colony-health issues.
Pest and disease management becomes more practical
Many pest and disease-control decisions depend on seeing what is happening inside the colony. Movable frames provide the physical access required for routine monitoring and targeted intervention.
This does not eliminate disease risk, but it gives the beekeeper better information and more management options than a fixed-comb structure allows.
Colony splitting and merging are easier
Standard frames make it simpler to transfer brood, food stores, or bees between compatible hive units. This supports controlled colony splitting, merging, and rebalancing according to apiary needs.
These interventions help commercial operators manage colony strength and use available resources more deliberately.
Why Standardization Matters to Commercial Buyers
Compatible equipment simplifies expansion
A standardized hive system allows frames, boxes, foundations, covers, and related tools to be used across a larger number of colonies. This reduces the operational complexity of managing mixed equipment.
For distributors, wholesalers, and professional beekeepers, compatibility is a major purchasing consideration. A product portfolio built around consistent dimensions is more useful than a collection of isolated components that cannot work together.
Standard equipment supports labor efficiency
Employees can be trained on a common hive format and follow consistent handling procedures. Equipment inspection, frame replacement, honey extraction, and seasonal management become easier to organize.
Standardization also improves order planning because replacement parts and consumable components can be specified more accurately.
It enables a broader equipment ecosystem
Movable-frame hives work as part of a wider production system that may include wax foundations, frame assembly tools, honey extractors, hive tools, protective clothing, pest-control equipment, and transport accessories.
This creates practical value for one-stop sourcing. Buyers can align the hive design with the rest of their apiary equipment rather than solving compatibility problems one product at a time.
How Movable-Frame Hives Support Migratory Beekeeping
Portable units can follow flowering periods
Movable-frame hive bodies are designed for organized handling and transport. This makes them suitable for migratory apiaries that move colonies to different flowering areas.
Following successive nectar flows can help operators pursue seasonal production opportunities and manage the timing of honey harvests more effectively.
Honey can be kept separate by source
Because frames can be inspected, removed, and managed by hive or location, beekeepers have greater control over harvest timing and storage. This can support the production of distinct honey lots, including honey associated with specific flowering periods.
Maintaining that separation requires disciplined labeling, transport, and extraction practices, but movable frames provide the necessary operational control.
Understanding the Trade-offs
Initial investment is higher
Modern hive systems generally require more equipment than basic fixed-comb hives. The investment may include standardized boxes and frames, wax foundations, extractors, transport equipment, and protective gear.
The relevant comparison is not only purchase price. Commercial buyers should evaluate the equipment’s effect on labor, comb reuse, inspection efficiency, maintenance, and long-term production.
Training and maintenance are essential
Movable-frame equipment delivers its benefits only when frames are correctly assembled, spaced, inspected, and maintained. Poorly managed equipment can lead to damaged comb, difficult inspections, or inefficient extraction.
Operators also need training in colony biology, hygienic handling, pest monitoring, and safe transport. The hive is a management platform, not a substitute for technical expertise.
Standardization must match the operation
Not every hive component is automatically interchangeable across all manufacturers or regional formats. Before purchasing, buyers should confirm frame dimensions, box compatibility, material quality, extractor capacity, and replacement-part availability.
For distributors and resellers, dependable specifications and responsive technical support are as important as the initial product price.
Higher yields are not guaranteed by hardware alone
Movable-frame hives create the conditions for more productive management, but results still depend on bee genetics, forage availability, weather, colony health, operator skill, and seasonal practices.
Claims about production increases should therefore be treated as operating potential rather than a universal guarantee.
Making the Right Choice for Your Goal
A modern movable-frame system is most valuable when equipment decisions are connected to the apiary’s wider workflow.
- If your primary focus is commercial honey yield: Choose compatible movable-frame hives and extraction equipment so comb can be reused and bees can spend more effort on honey storage than reconstruction.
- If your primary focus is colony health: Prioritize removable frames that enable regular inspection of brood, stores, pests, diseases, and queen performance.
- If your primary focus is apiary expansion: Standardize hive dimensions and source compatible frames, foundations, boxes, and replacement parts from a dependable supply partner.
- If your primary focus is migratory or specialty honey production: Select portable equipment and establish disciplined systems for transport, frame identification, harvest timing, and lot separation.
- If your primary focus is procurement efficiency: Work with a supplier that can provide a full equipment range, fast responses, technical expertise, reliable quality, and efficient order fulfillment.
For commercial apiaries, adopting movable-frame hives is not simply an equipment upgrade—it is a practical foundation for scalable, measurable, and sustainable beekeeping.
Summary Table:
| Advantage | Impact on Commercial Apiaries |
|---|---|
| Reusable comb | Saves bee effort, increases honey storage capacity |
| Non-destructive inspections | Reduces labor, enables proactive management |
| Standardized components | Simplifies expansion, training, and maintenance |
| Pest/disease management | Improves monitoring and intervention accuracy |
| Colony splitting/merging | Enables controlled population and resource balancing |
| Migratory compatibility | Supports transport and seasonal honey harvests |
| Efficient extraction | Preserves comb, increases productivity |
| Integration with ecosystem | Aligns with tools, extractors, and protective gear |
Upgrade to modern movable-frame hives with HONESTBEE – your one-stop wholesale partner for high-quality beekeeping equipment. We empower commercial apiaries and distributors with a full spectrum of tools and machinery, OEM/ODM support, certifications, fast delivery, and responsive service. Boost your efficiency and profit margins – contact our experts today to discuss your needs!
Related Products
- High-Performance Langstroth Bee Hives for Global Professional Beekeeping
- Langstroth Honey Bee Box Hive Boxes for Different Depths
- Australian Langstroth Beehive Boxes for Beekeeping Wholesales
- Long Langstroth Style Horizontal Top Bar Hive for Wholesale
- Professional Observation Hive: The Ultimate Portable Solution for Beekeeping Education, Exhibitions, and Colony Displays
People Also Ask
- What are the structural and yield differences between traditional primitive beehives and modern standard wooden hives (such as Langstroth hives) for commercial honey producers? Discover why modern hives boost yield and efficiency.
- How does transitioning to modern hives boost honey yield? Increase production and product quality for your commercial apiary
- How do Langstroth and Dadant standard beehives compare regarding brood chamber management and component compatibility? Find the Perfect Fit for Your Apiary
- What is the primary function of using standard Langstroth hives for bee performance evaluation? Eliminate Variables
- What are the technical advantages of standardized Langstroth hives? High-Precision Tools for Commercial Apiaries