All Questions
What Role Does Specialized Processing Machinery Play In The Development Of A Modern Apiary Workshop? Boost Scale And Roi
Discover how specialized machinery drives standardization, hygiene, and high-value product creation in modern commercial apiary workshops.
What Is The 'Crush And Strain' Method Of Honey Processing? A Simple Guide To Low-Cost Harvesting
Learn how the crush and strain method works for honey harvesting, including its benefits for wax collection and low equipment costs.
What Is The Role Of A Laboratory Conductivity Meter In Distinguishing Floral Honey? Mastering Honey Classification
Learn how laboratory conductivity meters provide rapid, objective analysis to distinguish floral honey from honeydew honey based on mineral content.
What Data Is Provided By A Precision Ph Meter Or A Potentiometric Titrator When Analyzing Honey Quality? Expert Guide
Learn how pH meters and potentiometric titrators analyze honey purity, acidity levels, and storage stability for quality control.
Why Is A Uv-Visible Spectrophotometer Used To Detect Hmf? Ensuring Honey Quality And Bioactivity In Biostimulants
Learn how UV-Visible spectrophotometry detects HMF to ensure honey freshness and preserve bioactive compounds for biostimulant research.
What Is The Significance Of A Water Activity Meter In Honey-Based Food Supplements? Ensuring Biological Stability
Learn how water activity meters ensure honey-based supplement safety by measuring free water to prevent fermentation and eliminate preservatives.
What Is The Function Of A Uv/Vis Spectrophotometer In Honey Invertase Measurement? Ensure Honey Freshness And Quality
Learn how UV/VIS spectrophotometers measure honey invertase activity at 400 nm to detect heat damage and ensure premium quality standards.
Why Must A Constant Temperature Water Bath Be Used In Honey Invertase Detection? Ensure Precise Enzymatic Accuracy
Learn why a 40°C constant temperature water bath is essential for honey invertase activity detection to ensure accuracy and prevent kinetic errors.
What Is The Role Of A Honey Colorimeter? Enhance Commercial Value And Precision In Honey Grading
Learn how high-precision honey colorimeters eliminate subjective error and use the Pfund scale to determine market value and botanical origin.
How Are High-Precision Ph Meters And Density Meters Utilized In Honey Beverage Production? Master Quality Control
Learn how pH and density meters ensure consistency, microbial safety, and precise sugar conversion in standardized honey beverage production.
Why Is The Sterilization Of Industrial Honey Extraction And Bottling Machinery Essential? Ensure Food Safety & Purity
Learn why sterilizing honey machinery is a critical HACCP risk node to prevent contamination and preserve honey's sensory quality.
Why Is It Necessary To Equip Honey Processing Facilities With Specialized Filtration And Dehydration Equipment?
Learn how specialized filtration and dehydration systems prevent fermentation, ensure safety, and meet international honey export standards.
What Are The Advantages Of Industrial-Grade Creamed Honey Processing Machines For Texture And Stability?
Learn how industrial creamed honey machines use precise temperature and stirring to ensure smooth texture and prevent phase separation.
What Is The Function Of Honey Sample Homogenization In The Initial Preparation? Ensure Accuracy In Quality Analysis
Learn how honey sample homogenization eliminates composition bias and creates a uniform physicochemical baseline for precise quality testing.
How Do Beehive Placement And Industrial Processing Equipment Influence Honey Quality? Optimize Your Honey Production
Discover how strategic hive placement and advanced processing equipment work together to ensure honey stability, flavor, and commercial value.
How Do Professional Packaging And Processing Technologies Contribute To The Honey Value Chain? Elevate Your Market Value
Learn how professional processing and packaging transform raw honey into high-value assets by enhancing quality, safety, and marketability.
What Function Do Vacuum Chambers And Pump Systems Perform In Bee Bread Packaging? Ensure Peak Nutritional Potency
Learn how vacuum systems remove oxygen to enable inert gas injection, protecting the fragile vitamins and fatty acids in bee bread products.
What Is The Role Of Specialized Honey Storage And Ripening Equipment? Guarantee Superior Honey Stability And Grade
Discover how specialized honey storage and ripening equipment regulates temperature and humidity to prevent fermentation and preserve quality.
How Does Specialized Propolis Processing Equipment Increase Project Value? Scale Profits With Stingless Bee Products
Unlock higher margins by transforming raw propolis into premium pharmaceutical-grade ingredients with specialized extraction equipment.
What Is The Primary Role Of Industrial Honey Processing Equipment? Optimize Efficiency And Purity
Learn how industrial honey equipment maximizes yield and safety through centrifugal extraction and filtration while preserving biological integrity.
How Does Professional Honey Processing Equipment Enhance The Market Appeal? Boost Quality And Retail Success
Learn how professional honey processing equipment improves clarity, moisture control, and hygiene to meet premium retail and export standards.
What Key Technical Support Do Honey Processing Plants Provide For Export? Master Global Standards & Industrial Efficiency
Learn how industrial honey machinery ensures moisture control, purity, and consistency to meet strict global honey export standards.
What Is The Role Of Honey Processing & Filling Machinery? Elevate Production Efficiency And Market Value
Discover how professional honey machinery ensures hygiene, scales production, and secures international certification for commercial apiaries.
How Does Modern Honey Filtration And Processing Equipment Enhance Product Value? Boost Quality And Retail Appeal
Discover how advanced honey filtration improves clarity, extends shelf life, and ensures food safety compliance for premium retail markets.
How Does Specialized Honey Processing Equipment Improve The Quality Of Harvested Honey? Boost Your Global Export Value
Learn how specialized honey processing equipment ensures purity, stability, and standardization to meet international trade requirements.
What Is The Impact Of Modern Harvesting And Processing Equipment On The Market Value Of Honey? Unlock Premium Pricing
Discover how modern beekeeping equipment increases honey market value through purity, food safety, and industrial-grade processing efficiency.
How Does The Establishment Of Centralized Honey Collection Points Optimize The Logistics And Processing Workflow?
Learn how centralized honey collection points streamline logistics, reduce costs, and maintain quality by bridging producers and markets.
What Are The Primary Functions Of Industrial-Grade Large Sedimentation Tanks In Honey Processing? Enhance Your Quality Control
Discover how industrial sedimentation tanks use gravity to purify honey, ensure clarity, and preserve nutritional integrity without heat damage.
How Does The Determination Of Water-Insoluble Matter In Honey Influence The Selection And Operation Of Processing Equipment?
Learn how measuring water-insoluble matter optimizes honey filtration, protects machinery from wear, and ensures regulatory compliance.
How Do Honey Harvesting And Processing Machines Support Indigenous Bee Conservation? Transforming Ecology Into Economy
Learn how advanced honey processing machinery creates economic incentives for bee conservation through value-added production.
How Does The Transition To Industrial-Grade Honey Processing And Filtration Equipment Improve Honey Product Quality?
Learn how industrial honey processing enhances clarity, flavor, and shelf life through precision filtration and moisture control.
What Is The Function Of High-Efficiency Solvent Extraction Equipment In The Propolis Dewaxing Process? Purify With Ease
Learn how high-efficiency solvent extraction automates propolis dewaxing, reduces wax content, and preserves bioactive resins for high quality.
What Is The Critical Role Of A Vacuum Freeze Dryer In Apilarnil Production? Preserve Potency And Stability
Learn how vacuum freeze dryers stabilize drone larvae powder (Apilarnil) by preserving bioactive enzymes and extending shelf life without heat.
Why Is An Industrial Low-Temperature Freezer Essential For Drone Larvae? Lock In Nutrients And Potency
Learn why -18°C industrial freezing is vital for preserving drone larvae nutrients, stopping enzyme activity, and extending shelf life to 10 months.
How Does An Air Circulation Dryer Compare To A Vacuum Freeze Dryer? Choosing The Best Method For Drone Larvae Powder
Compare air circulation and vacuum freeze drying for drone larvae powder. Learn about nutrient retention, shelf life, and cost-efficiency.
Why Is Professional Honey Harvesting And Processing Equipment Considered A Necessary Investment? Boost Roi & Efficiency
Discover how professional honey equipment increases yield, lowers labor costs, and unlocks retail value for commercial beekeeping operations.
What Is The Role Of A Quantitative Spectrophotometer In Evaluating Honey For Heat Damage? Ensure Freshness With Hmf Testing
Learn how spectrophotometers measure HMF levels at 284nm and 336nm to detect heat damage and ensure honey quality and freshness.
What Key Process Does A Muffle Furnace Perform In The Ash Analysis Of Honey? Ensure Precision And Purity
Learn how high-temperature calcination in a muffle furnace isolates mineral ash to verify honey's botanical origin and quality standards.
What Advantages Does A Concentric Cylinder Rheometer Offer Over A Standard Viscometer? Expert Honey Analysis Guide
Learn why a concentric cylinder rheometer is superior to a viscometer for honey analysis, offering precise flow curves and shear-thinning data.
What Role Does A Constant Temperature Water Bath Play In The Rheological Measurement Of Honey? Ensure Data Accuracy
Learn how a constant temperature water bath controls thermal uniformity to ensure accurate, reproducible honey viscosity data.
What Role Does Industrial-Grade Processing Equipment Play In Honey Competitiveness? Secure Your Organic Honey Quality
Discover how industrial equipment ensures organic honey integrity through contamination control, traceability, and moisture management.
Why Is A 0.20 Μm Microporous Membrane Used For The Cold Sterilization Of Royal Jelly? Preserve Bioactive Potency
Learn why 0.20 μm cold filtration is essential for royal jelly sterilization to remove bacteria while preserving 10-HDA and sensitive proteins.
What Role Does Industrial Weighing Equipment Play In Honey Production? Precision Metrics For Modern Apiculture
Learn how industrial weighing equipment optimizes honey yield, improves genetic selection, and monitors colony health through data-driven metrics.
How Does The Pasteurization Process Affect Honey? Understand The Impact On Nutrition, Flavor, And Shelf Stability
Learn how pasteurization impacts honey's enzymes, antioxidants, and physical properties to help you choose between stability and nutrition.
What Are The Functional Differences Between Raw Honey And Regular Pasteurized Honey? Understanding Heat Vs. Nutrition
Explore how processing affects honey. Compare raw vs. pasteurized honey in terms of enzymes, pollen retention, flavor, and nutritional benefits.
What Is The Significance Of Establishing Intensive Honey Processing Facilities For The Honey Industry's Advancement?
Learn how intensive honey processing facilities drive industry growth through standardization, precision control, and high-value market access.
What Are The Requirements For Specialized Reaction Vessels? Key Hardware For Stingless Bee Product Processing
Learn the essential requirements for stingless bee product reaction vessels, focusing on stainless steel and precise thermal regulation.
What Are The Technical Advantages Of Sfe Over Ethanol Maceration? Elevate Propolis Extraction For Superior Purity
Compare SFE vs. ethanol maceration for propolis. Learn how supercritical fluid extraction ensures zero residues and preserves bioactivity.
Why Is Vacuum Freeze-Drying Equipment Required For Bee Products? Preserve Potency In Royal Jelly & Bee Venom
Learn why vacuum freeze-drying is essential for heat-sensitive bee products to prevent protein denaturation and preserve bioactive compounds.
Why Is The Implementation Of Professional Honey Processing Technology Critical For International Honey Export?
Learn why professional honey processing is essential for global export, focusing on moisture control, purity, and international regulatory compliance.
What Function Do Specialized Filtration And Fermentation Machines Serve In The Industrial Production Of Honey-Based Beverages?
Learn how specialized filtration and fermentation machines transform raw honey into stable, commercial-grade beverages through precise processing.
What Are The Advantages Of Standardized Honey Processing Equipment? Scale Your Production And Ensure Export Quality
Discover how standardized honey equipment boosts yield, preserves bioactive purity, and meets export standards over manual methods.
How Do Industrial Honey Extraction And Processing Machines Improve The Quality Of Raw Honey? Enhance Purity & Stability
Learn how industrial honey equipment improves raw honey through precise filtration, moisture control, and advanced dehydration techniques.
What Is The Primary Purpose Of Using A Grinding Machine? Optimize Bee Pollen Phenolic Extraction Today
Learn how grinding machines increase surface area and solvent penetration for efficient phenolic extraction from bee pollen and bee bread.
How Does An Ultrasonic Cleaning Bath Facilitate The Extraction Of Phenolic Compounds From Bee Products? Boost Potency
Learn how ultrasonic cavitation ruptures cell walls in bee products to extract heat-sensitive phenolic compounds with higher yields and speed.
What Are The Benefits Of Industrial Honey Machinery? Scale Your Apiary With Advanced Processing And Filling Solutions
Discover how industrial-grade honey machinery enhances product purity, ensures market standardization, and secures economic stability for apiaries.
What Functions Do Industrial-Grade Honey Processing Machines Perform? Drive Market Competitiveness With Advanced Tech
Learn how industrial honey processing machines enhance market competitiveness through precise moisture control, filtration, and automated filling.
What Is The Significance Of An Integrated Honey Processing Plant? Scaling Beekeeping Cooperatives For Profit
Discover how integrated honey processing plants transform beekeeping cooperatives through quality control, deep processing, and retail readiness.
How Do Fine Extraction Machines Contribute To The Development Of Algae-Derived Bee Immune Enhancers?
Learn how fine extraction technology concentrates microalgae biomolecules to create potent, disease-resistant immune enhancers for honeybees.
Why Are Specialized Cold Chain And Deep Processing Technologies Necessary For Bee Products? Ensure Maximum Bioactivity
Learn why ultra-low temp storage and freeze-drying are vital for preserving the bioactivity and market value of royal jelly and propolis.
What Is The Significance Of Implementing A Haccp System In Honey Processing? Secure Global Market Access For Your Honey
Learn how HACCP systems protect honey quality and act as a vital gateway for international exports to high-value markets like the EU.
What Processing Technologies Are Utilized In Honey Production To Delay Crystallization? Master Stabilization Techniques
Learn how precise heating and filtration technologies extend honey shelf life by dissolving glucose crystals and removing nucleation sites.
What Technical Standards Are Required For Machinery And Consumables For Organic Honey? Ensure Pure Production
Learn the essential standards for organic honey production, from food-grade stainless steel machinery to natural, untreated beehive materials.
How Can Honey Processing Equipment Address Consumer Biases? Transform Crystallized Honey Into Premium Creamed Products
Learn how processing equipment turns crystallized honey into high-value creamed products, ensuring stability, purity, and better market positioning.
Why Is Rapid Homogenization Necessary In The Commercial Collection Process Of Apilarnil? Preserve Bioactive Potency Now
Learn why rapid homogenization is vital for Apilarnil production to prevent oxidative spoilage and lock in nutritional stability.
What Are The Primary Technical Differences Between The Production Of Raw Honey And Processed Honey? Key Comparisons
Learn the technical differences between raw and processed honey production, focusing on temperature, filtration, and nutritional integrity.
How Does Flash Pasteurization At 160°F Impact The Chemical Composition Of Honey? Balance Stability And Bioactivity
Learn how heating honey to 160°F destroys enzymes and antioxidants, and discover the trade-offs between shelf stability and nutritional value.
What Is The Importance Of Using A High-Precision Electrical Conductivity Meter For Honey? Ensure Honey Purity & Origin
Learn how high-precision electrical conductivity meters distinguish blossom, honeydew, and blended honey by measuring mineral 'fingerprints'.
What Is The Technical Significance Of Measuring Ph Values With A Precision Acidity Meter During The Quality Grading Of Honey?
Learn how precision pH measurement in honey ensures biological stability, flavor consistency, and scientific traceability for quality grading.
How Does A Specialized Water Activity Analysis System Assist In Assessing The Commercial Storage Safety Of Honey? | Honestbee
Learn how water activity analysis predicts fermentation risks and ensures honey storage safety for export and long-distance logistics.
What Is The Role Of Heating And Ultrasonic Agitation In Honey Pretreatment? Ensure Analytical Accuracy
Learn how heating and ultrasonic agitation homogenize honey samples, dissolve crystals, and reduce viscosity for precise composition analysis.
Why Is The Water Evaporation Process Critical In Industrial Honey Processing? Ensure Stability And Product Quality
Learn why moisture control in honey processing prevents fermentation, ensures high osmotic pressure, and meets commercial viscosity standards.
Why Is Precise Temperature Control Essential For Bee Pollen Drying? Protect Nutrients With Honestbee Technology
Learn why precise thermal control is critical in bee pollen processing to preserve proteins, amino acids, and prevent mycotoxin contamination.
What Role Does Constant Temperature Oscillation Equipment Play In The Extraction Of Bee Pollen? Boost Kinetic Yield
Learn how constant temperature oscillation (40°C, 150 rpm) maximizes the extraction of lipids from lyophilized bee pollen.
What Is The Importance Of Using Standardized Industrial Extraction Equipment In The Propolis Extraction Process? Achieve Safety & High Yield
Learn how industrial extraction equipment ensures consistent biological activity, safety, and maximum yield in propolis processing.
How Does Temperature-Controlled Extraction Improve Propolis Extract Quality? Master Purity & Potency Control
Learn how precise thermal regulation optimizes propolis extraction, prevents wax contamination, and protects bioactive flavonoids and resins.
What Is The Application Value Of Industrial-Grade Honey Processing Equipment In Managing High-Yield Landscapes?
Unlock the full potential of high-yield landscapes with industrial honey equipment that ensures rapid, sanitary, and scalable production.
Why Is Specialized Emulsification Or Atomization Equipment Required? Unlock High-Value Therapeutic Bee Products
Learn why specialized equipment is essential for maximizing the bioavailability and absorption of bee products in skincare and respiratory health.
How Does Specialized Processing Equipment For Bee By-Products Affect Beekeeper Income? Maximize Your B2B Profit Potential
Discover how deep-processing equipment for propolis, pollen, and royal jelly transforms raw hive products into high-value industrial ingredients.
What Role Do Professional Honey Harvesting And Processing Machines Play? Scale Your Yield And Market Value
Discover how professional honey machinery transforms raw yield into high-value, market-ready inventory through sterile extraction and automation.
How Does The Determination Of Diastase Activity (Gothe Units) Guide The Optimization Of Honey Processing Equipment?
Learn how measuring diastase activity (Gothe units) helps optimize honey processing equipment and prevents thermal damage during production.
What Is The Primary Function Of Industrial Grinding In Drone Brood Powder Processing? Boost Bioavailability & Quality
Learn how industrial grinding equipment optimizes drone brood powder by refining particle size, enhancing nutrition, and ensuring feed homogeneity.
What Are The Benefits Of Using Automated Honey Extraction And Processing Lines? Elevate Quality And Global Compliance
Learn how automated honey processing ensures EU export compliance, preserves bioactivity, and enhances production efficiency for commercial apiaries.
What Role Does Honey De-Waxing And Separation Equipment Play? Boost Forest Honey Value With Professional Processing
Learn how professional de-waxing equipment turns forest honey into a high-value dual-stream revenue source of pure honey and commercial beeswax.
What Are The Advantages Of Using Small-Scale Processing Equipment? Boost Honey Quality And Profit Margins
Learn how small-scale honey processing equipment preserves bioactivity, increases profit margins, and ensures superior on-site product quality.
How Do Standardized Evaluation Scales And Sample Cups Contribute To Honey Qa? Master Sensory Analysis For Premium Results
Learn how 5-point scales and transparent sample cups transform honey sensory evaluation into quantifiable data for superior quality assurance.
How Does The Demonstration Of Honey Processing Equipment Benefit Beekeepers? Unlock Efficiency & Scalability
Discover how centrifugal extractors and filling machines transform raw honey into high-value commercial goods while boosting hive productivity.
How Do Standardized Processing And Filtration Equipment Enhance Honey Market Competitiveness? Master Global Export Standards
Learn how advanced filtration and processing equipment ensure honey quality, meet export standards, and boost international market competitiveness.
What Are The Advantages Of Industrial Vacuum Evaporation For Honey? Preserve Quality With Low-Heat Dehydration
Learn why vacuum evaporation is superior to conventional heating for honey moisture regulation, preserving antioxidants and flavor profile.
How Does Vacuum Low-Temperature Concentration Equipment Address Quality Issues? Stabilize Stingless Bee Honey Quality
Learn how vacuum low-temperature technology reduces moisture and prevents fermentation in stingless bee honey while preserving vital bioactive enzymes.
How Do Electricity-Driven Honey Processing Machines Contribute To The Honey Post-Treatment Process? Boost Your Efficiency
Learn how automated honey processing machinery enhances extraction, filtration, and packaging for superior honey quality and safety.
What Are The Advantages Of Using Professional Honey Processing Equipment? Boost Purity, Yield, And Market Value
Learn how professional honey processing outperforms manual methods by preserving enzymes, enhancing hygiene, and increasing apiary efficiency.
What Core Technical Challenge Does Specialized Bee Bread Extraction Machinery Address? Protect Your Wax Combs Now
Learn how specialized extraction machinery solves the challenge of harvesting bee bread without destroying valuable honeycomb infrastructure.
What Specialized Equipment Is Necessary To Diversify Honey Production Into Mead Or Honey Beer? Scale Your Honey Business
Learn the essential equipment needed for mead and honey beer production, from fermentation vessels to honey heating systems.
How Does The Introduction Of Automated Honey Processing Equipment Improve Apiary Profitability? Scale Your Honey Business
Learn how automated extractors and filling machines boost apiary profits by lowering labor costs, increasing yield, and ensuring product quality.
How Do Advanced Packaging And Processing Machines Help Apiaries Solve Product Stagnation? Boost Your Revenue Today
Discover how advanced machinery transforms raw hive products into market-ready assets, ensures hygiene, and overcomes inventory stagnation.
How Does The Establishment Of A Specialized Honey Processing Facility Contribute To The Industrial Scaling Of Honey Production?
Learn how specialized honey processing facilities enable industrial scaling through standardization, hygiene, and advanced equipment.
What Is The Primary Purpose Of Adding High-Purity Glucose Crystal Seeds In Honey Crystallization? Master Honey Texture
Learn how high-purity glucose seeds create smooth, microcrystalline honey by providing nucleation sites and shortening production cycles.
What Role Does A High-Precision Constant Temperature Climate Chamber Play In Honey Crystallization? Optimize Your Honey
Discover why a precise 14°C environment is critical for honey crystallization. Learn how climate chambers ensure natural lattice formation.
How Is A Texture Analyzer Utilized To Evaluate The Quality Of Crystallized Honey? Master Consistency In Honey Texture
Learn how texture analyzers measure hardness and cohesiveness in honey to ensure perfect spreadability and product quality standards.
Related Products
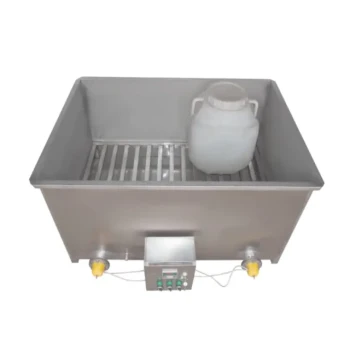
Heavy Duty Stainless Steel Honey Processing Machine Decrystallizing Tank

Electric Double Wall Honey Filtering Machine Purifier Equipment for Honey Processing Plant

Fully Automatic Honey Filling Packaging Machine for Processing Line

Electric Honey Press Machine for Squeezing Honey Comb Press Equipment

Commercial 48-Frame Stainless Steel Honey Extractor